
Precision Ceramic Injection Molded Components — Micron-Stable Tooling for Electronics, Automotive & Medical
XUXIANG delivers ceramic injection molded components held to +/-0.001 mm, backed by ISO 9001:2015, ZEISS CMM metrology and rapid quoting for OEM/ODM buyers worldwide.
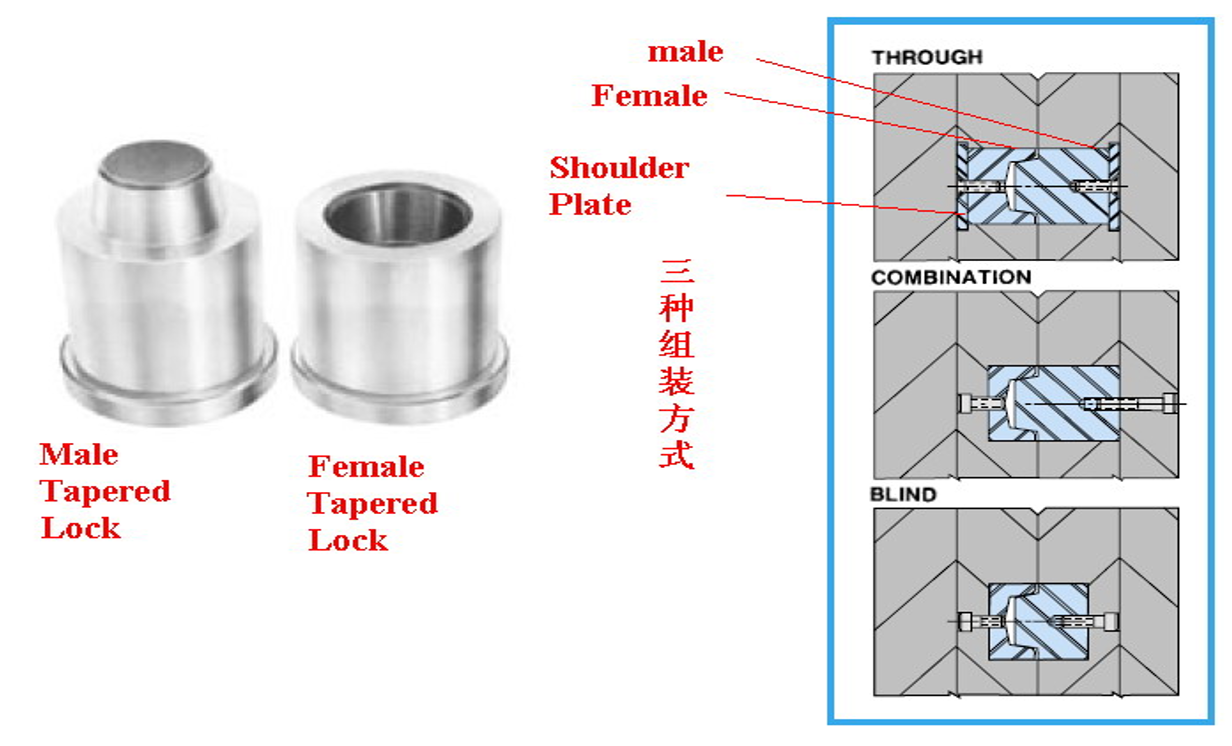
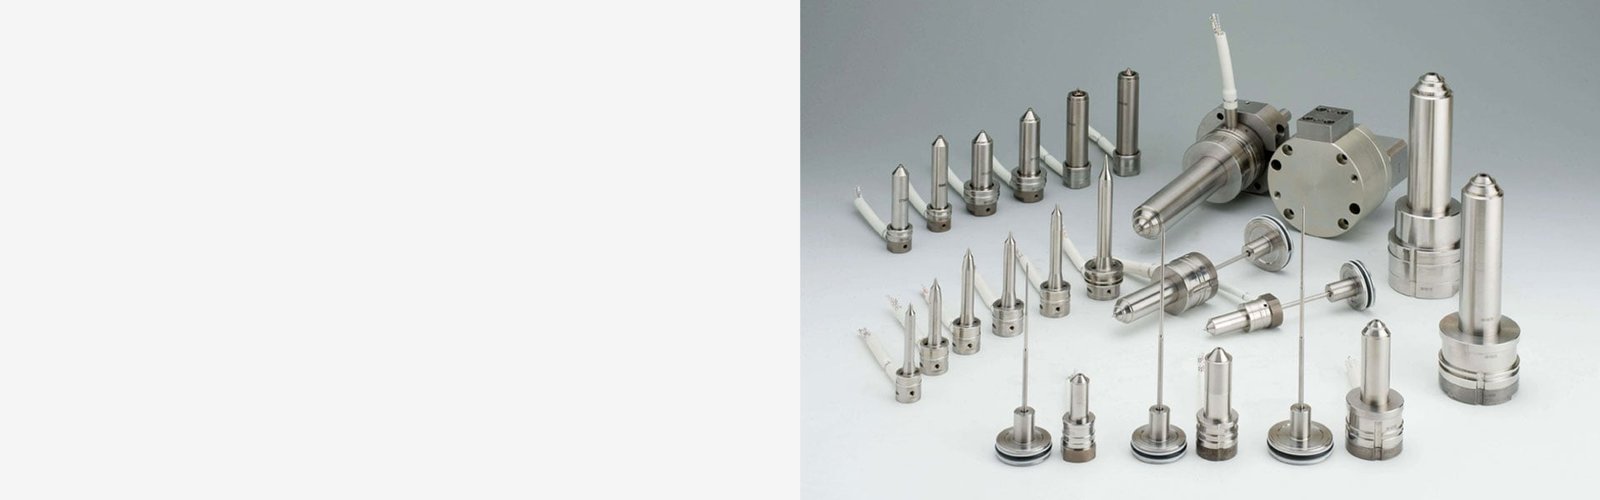
Featured Ceramic Injection Molding Tooling








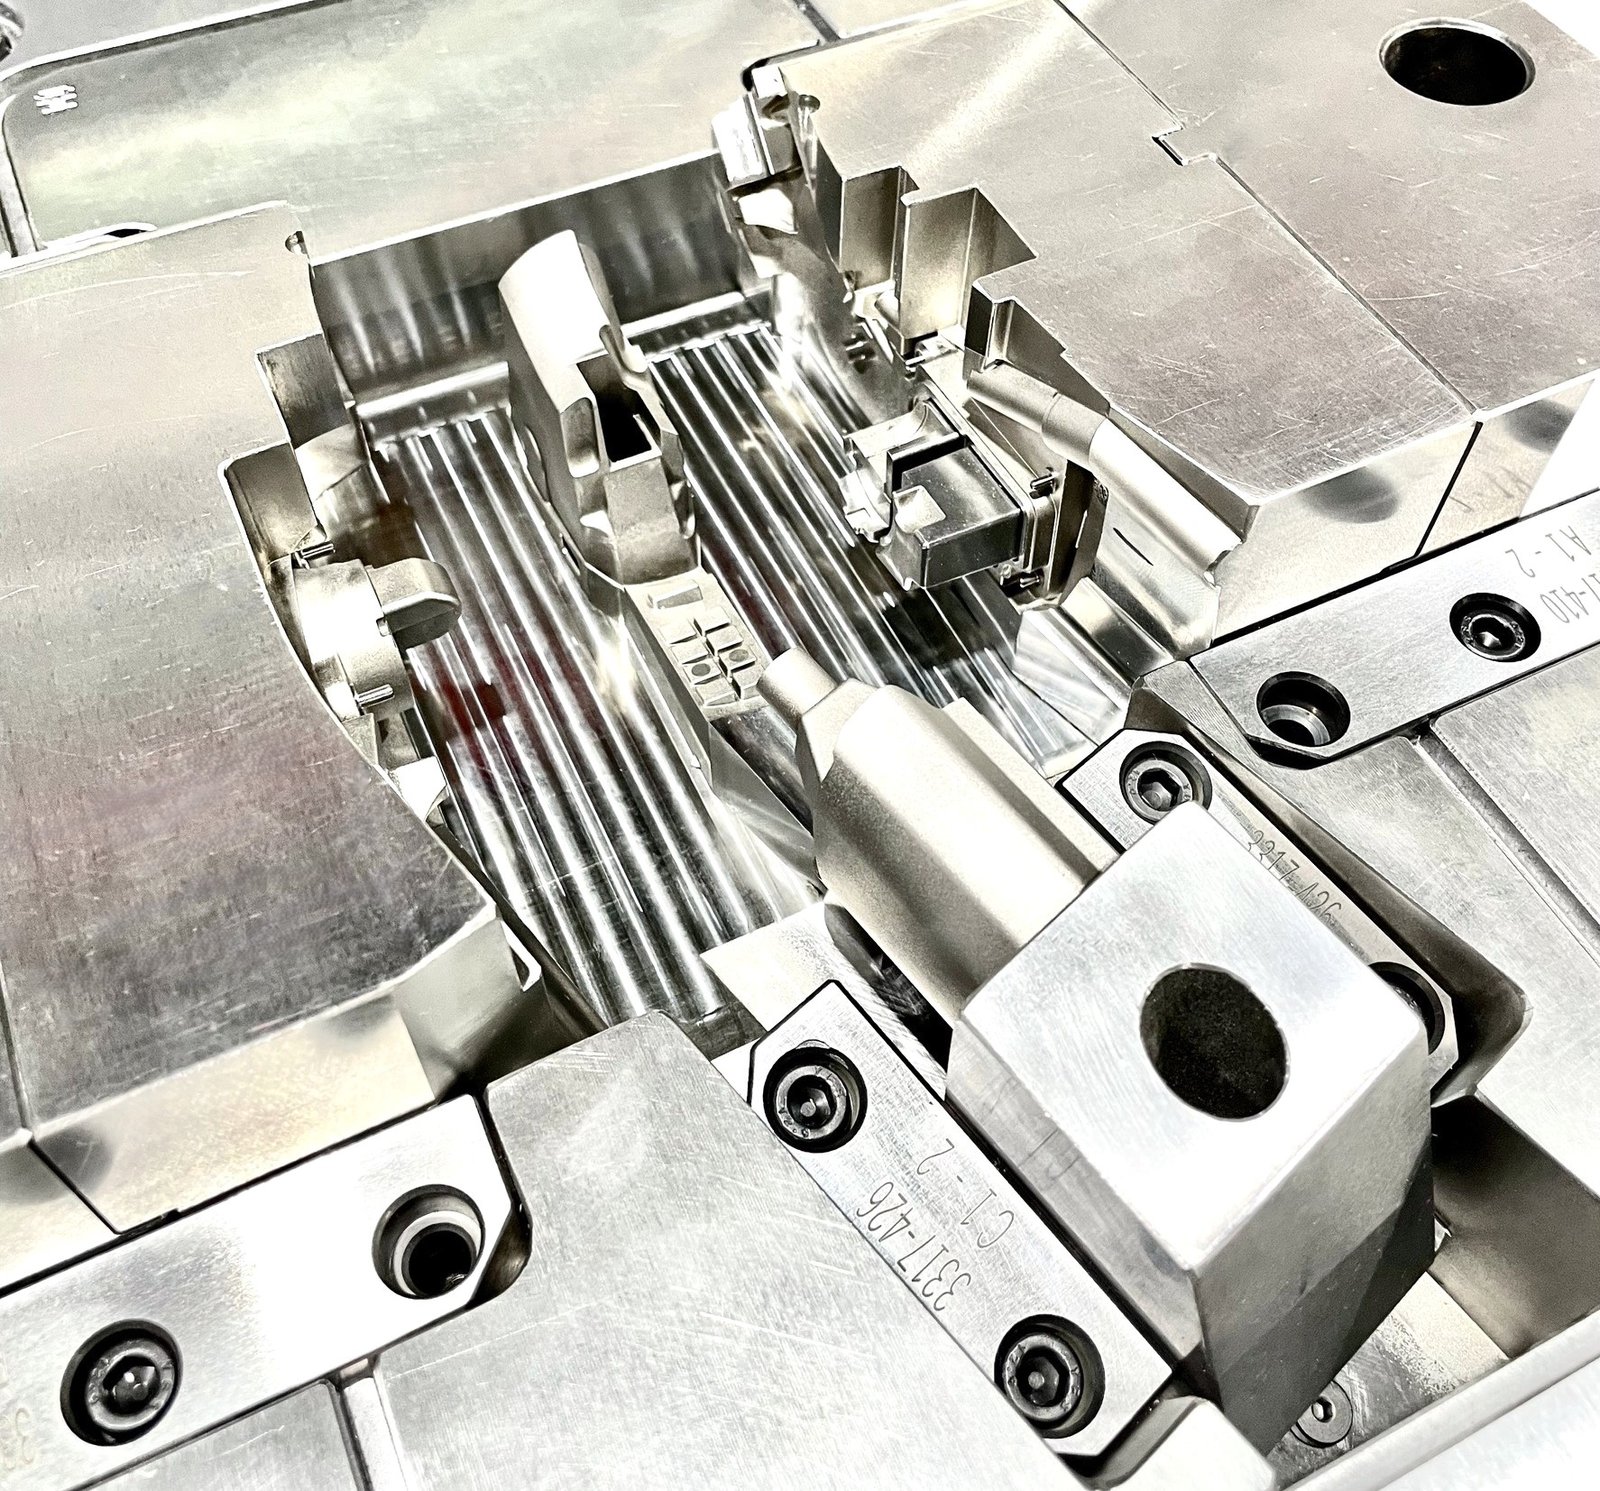
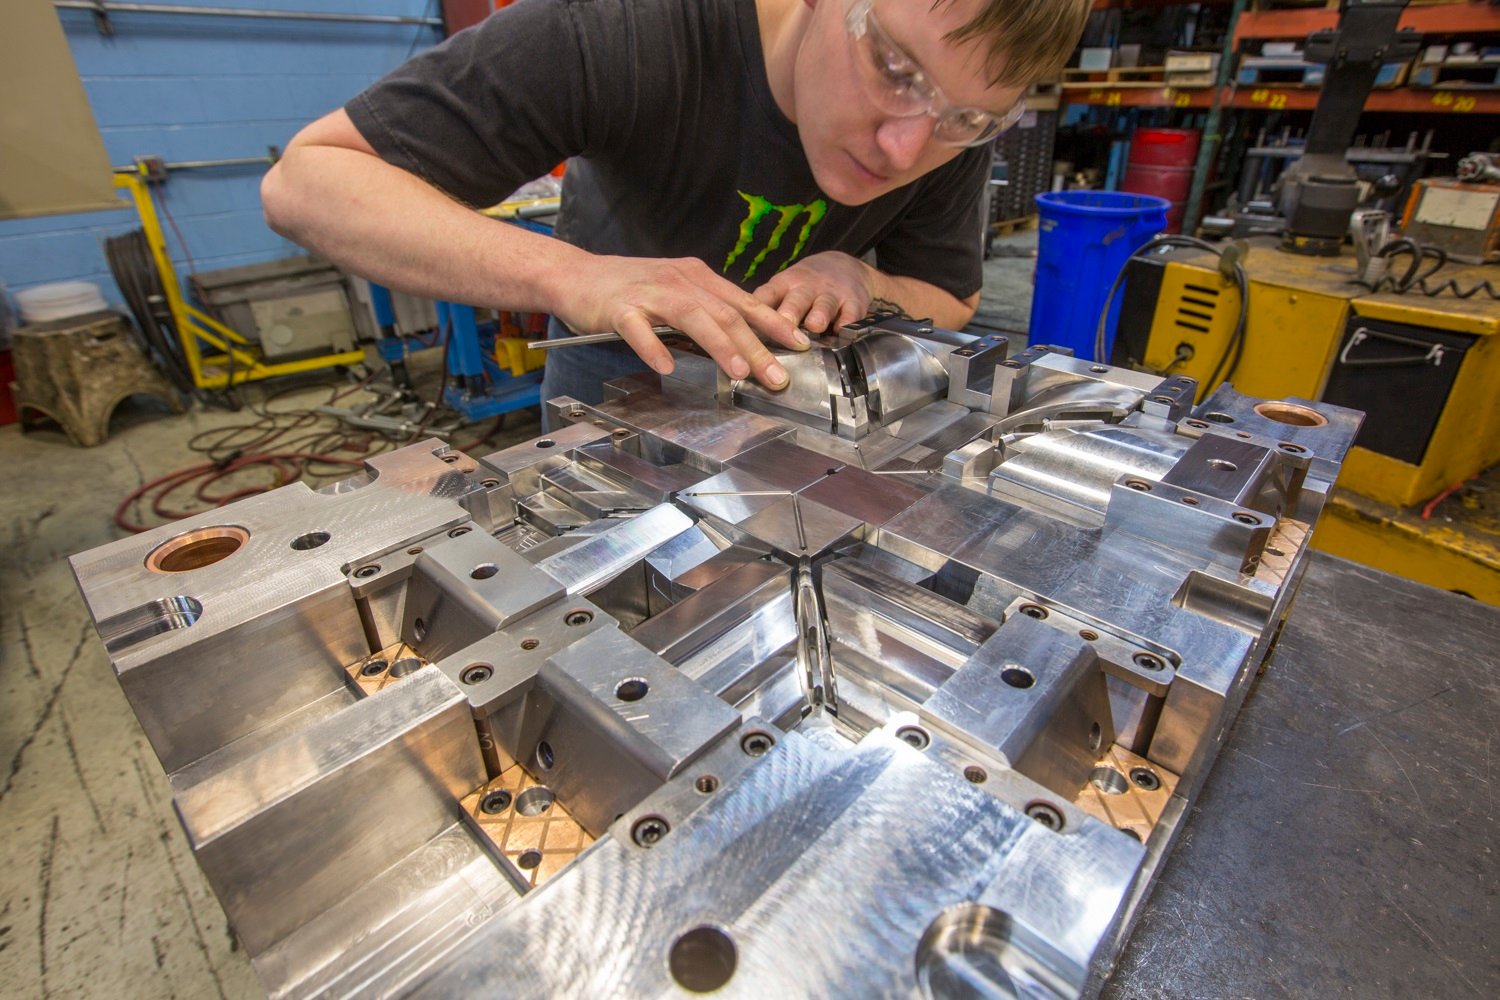
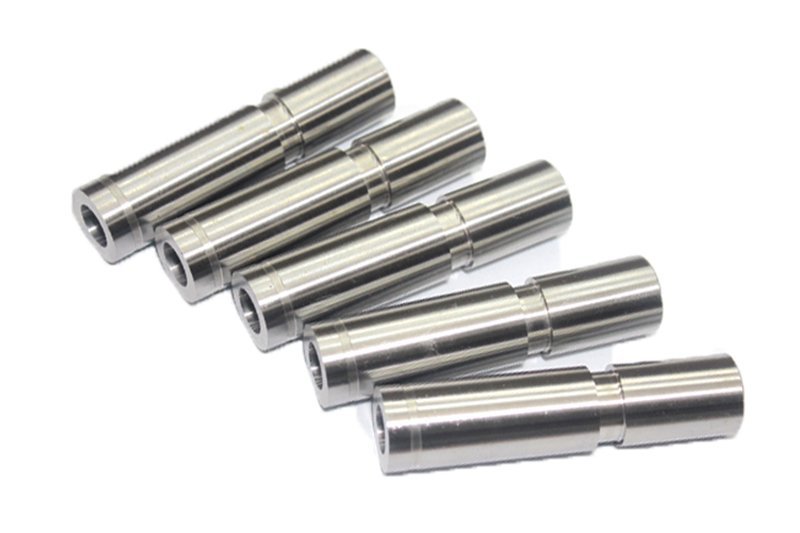
Precision Mold Components in Action
Why XUXIANG Ceramic Injection Molded Components Stand Apart
+/-0.001 mm Machining Precision
Maximum tolerance held across slow-wire EDM, CNC and grinding operations — validated on every ceramic injection molded component with ZEISS MICURA CMM metrology.
Mirror-Grade EDM Surface Finish
Ra 0.1um surface integrity achieved with Sodick slow-wire and Mitsubishi mirror EDM — critical for high-density ceramic injection molding tooling and micro-connectors.
ZEISS CMM Verification to 0.7um
Every ceramic injection molded component undergoes five-step QC with ZEISS MICURA CMM and Nikon toolmaker’s microscopes — full FAI reports and material certificates included.
24-Hour Quote, 3-7 Day Samples
Engineering-reviewed quotes returned within one business day; prototype ceramic injection molded components delivered in 3-7 days, mass production in 15-25 days.
Dual-Factory Capacity Since 2025
Dongguan 2,000 m² R&D facility plus Quanzhou 1,400 m² volume-production expansion — 200% capacity increase for dependable, scalable ceramic injection molding tooling.
ISO 9001:2015 & DFM Support
16 years of precision-mold experience, ISO-governed quality system, and DFM feedback from 10+ engineering experts before production — tolerance failure prevented upfront.
Advanced Ceramic Injection Molding Capabilities & Tooling
From feedstock formulation to post-sintered finishing—micron-stable tooling and CNC precision for high-performance ceramic components across electronics, automotive, 5G and medical applications.
Ceramic Feedstock Development
Custom ceramic feedstock formulation engineered for viscosity, particle distribution and mold-fill behavior in CIM processes. Working with zirconia, alumina and silicon nitride powders, XUXIANG develops binder systems optimized for thin-wall micro-features, dimensional stability post-debind and minimal sintering shrinkage—validated through rheology testing and pilot-run verification before production.
Get a Quote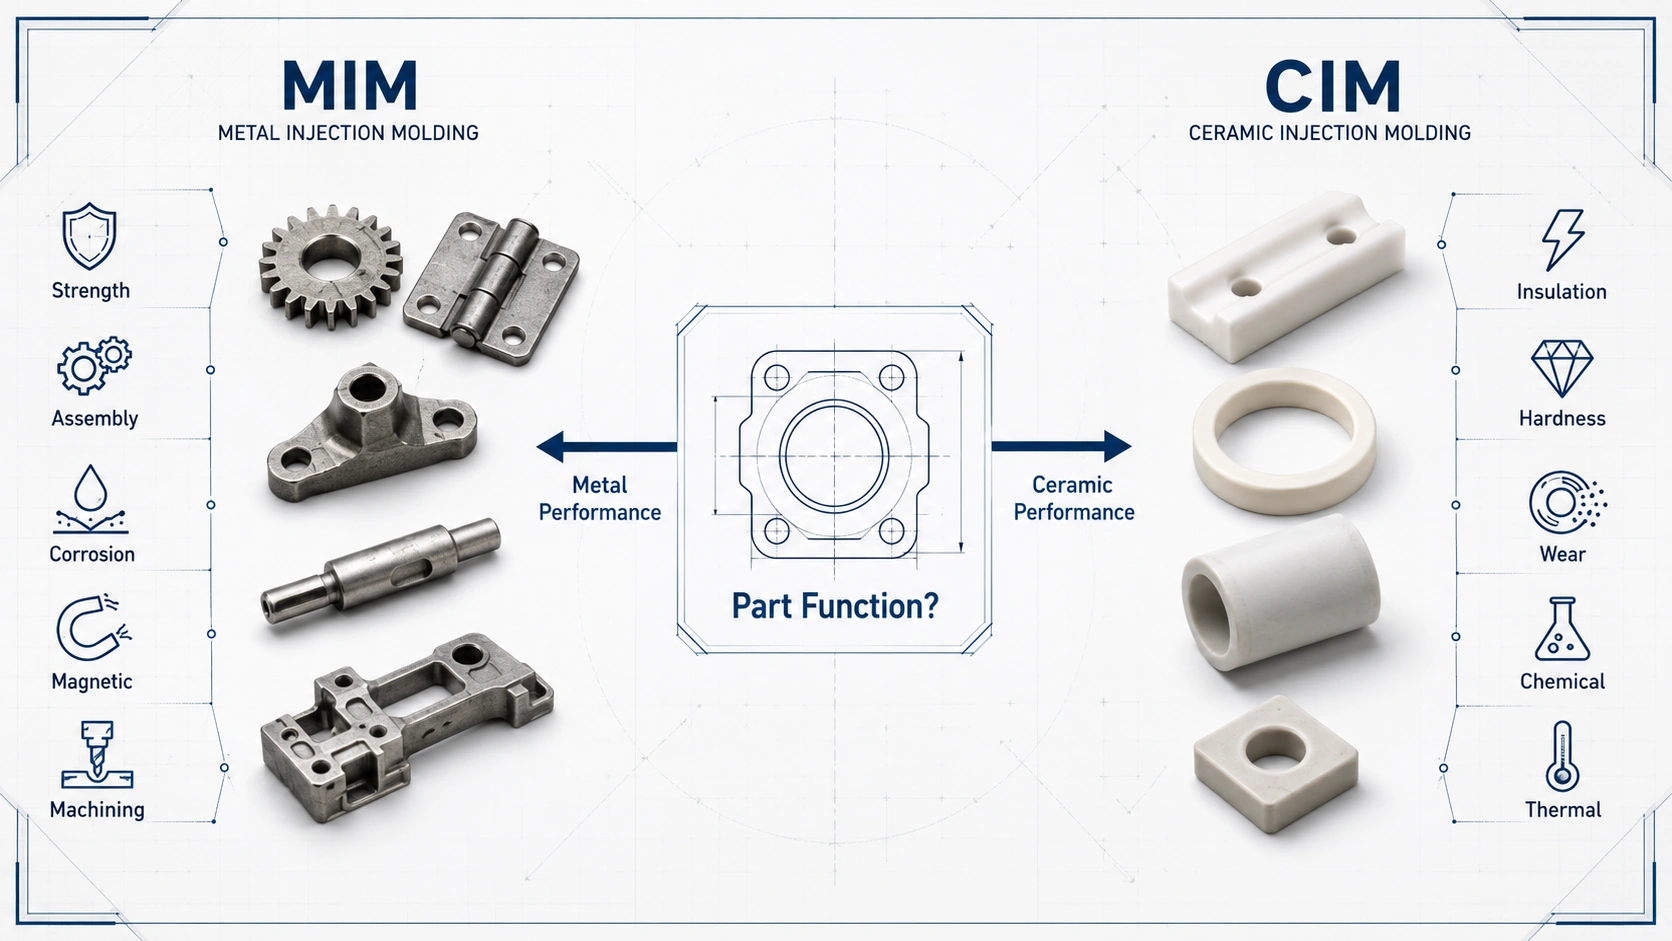
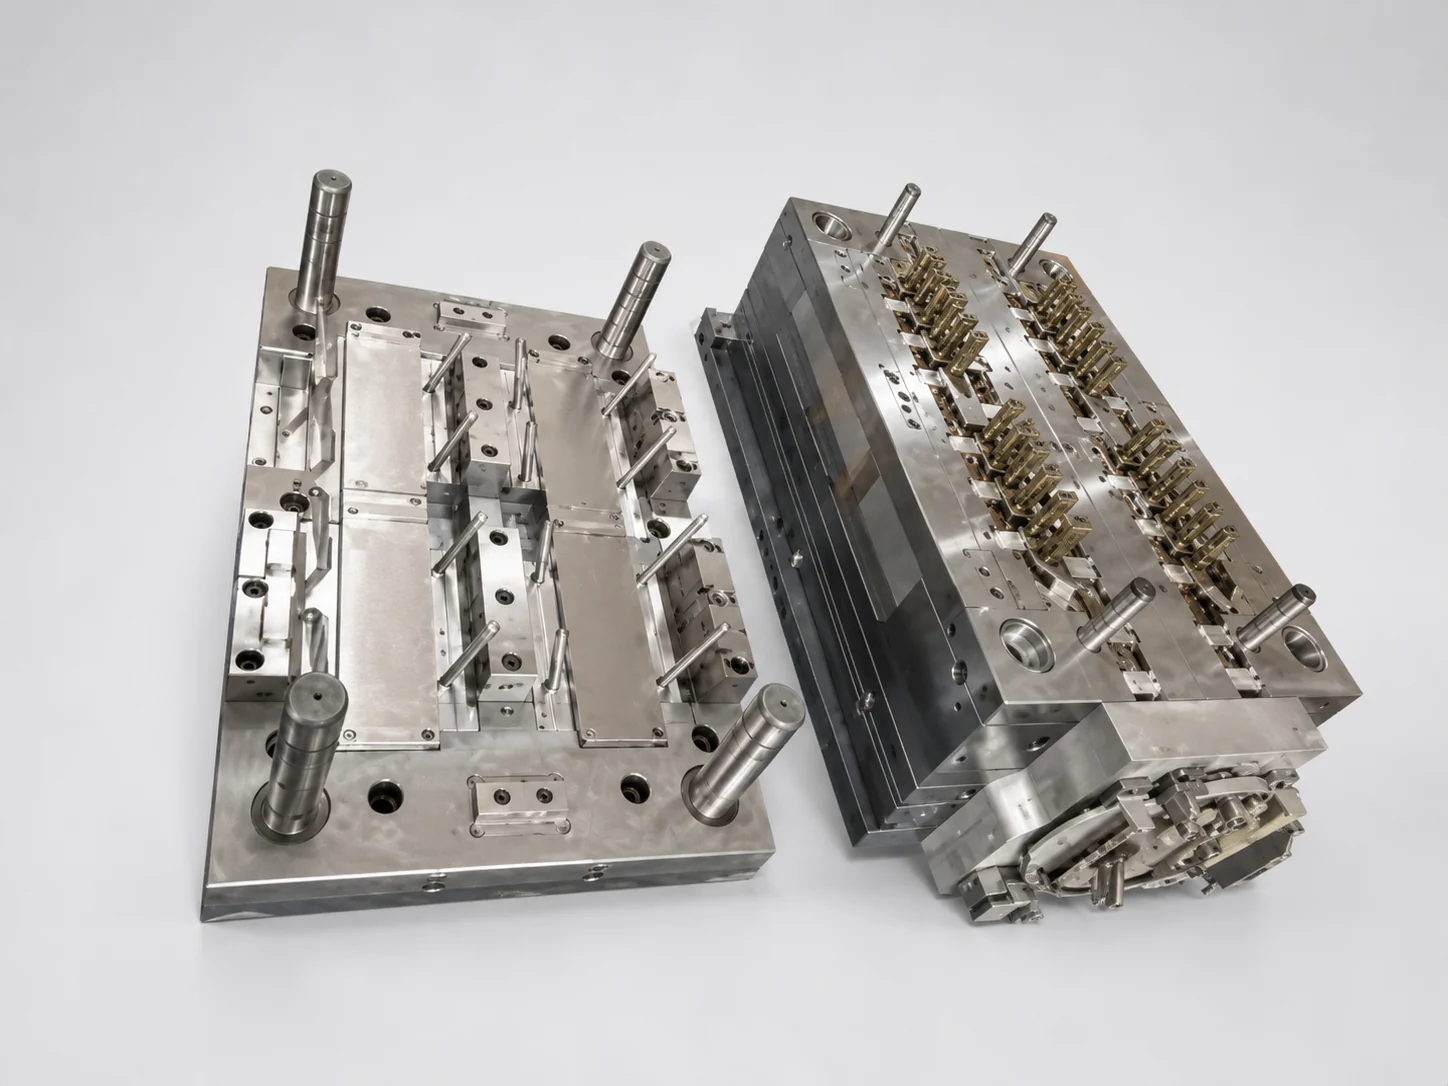
CIM Tooling & Molds
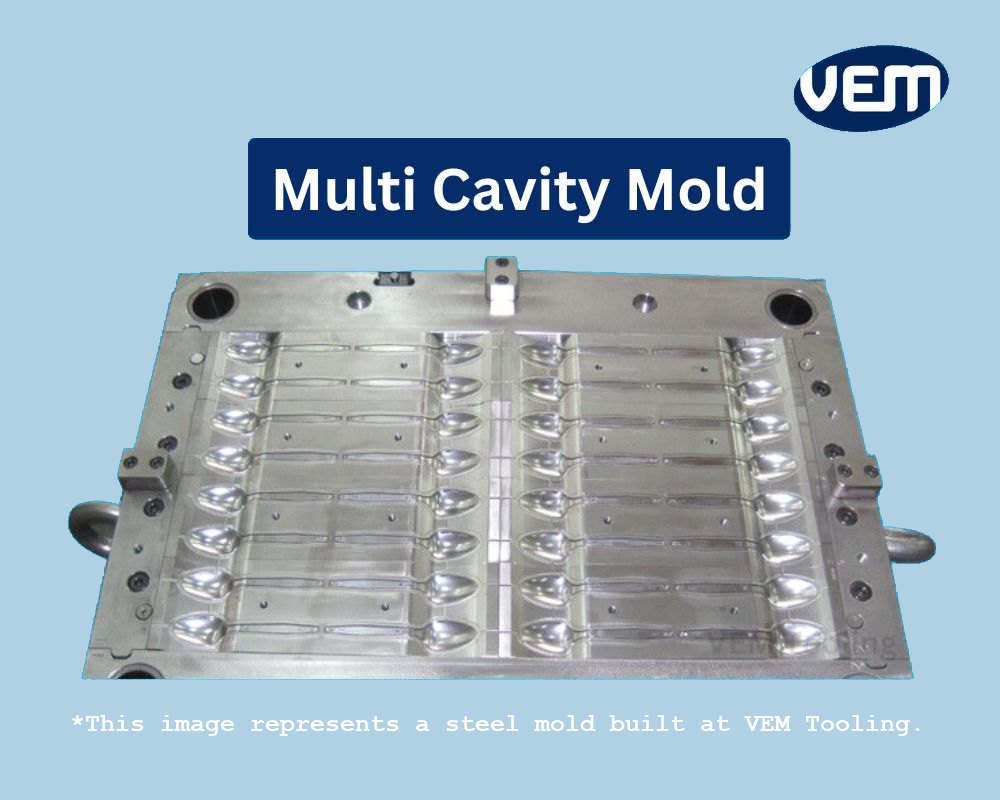
High-precision tooling for ceramic injection molding held to +/-0.001 mm machining tolerance. Sodick slow-wire EDM and mirror-grade finishing down to Ra 0.1 µm ensure cavity surfaces resist feedstock adhesion and enable clean ejection. Multi-cavity inserts, conformal cooling and micro-pin cores designed for zirconia, alumina and silicon nitride parts—backed by DFM analysis and ZEISS CMM validation.
Get a Quote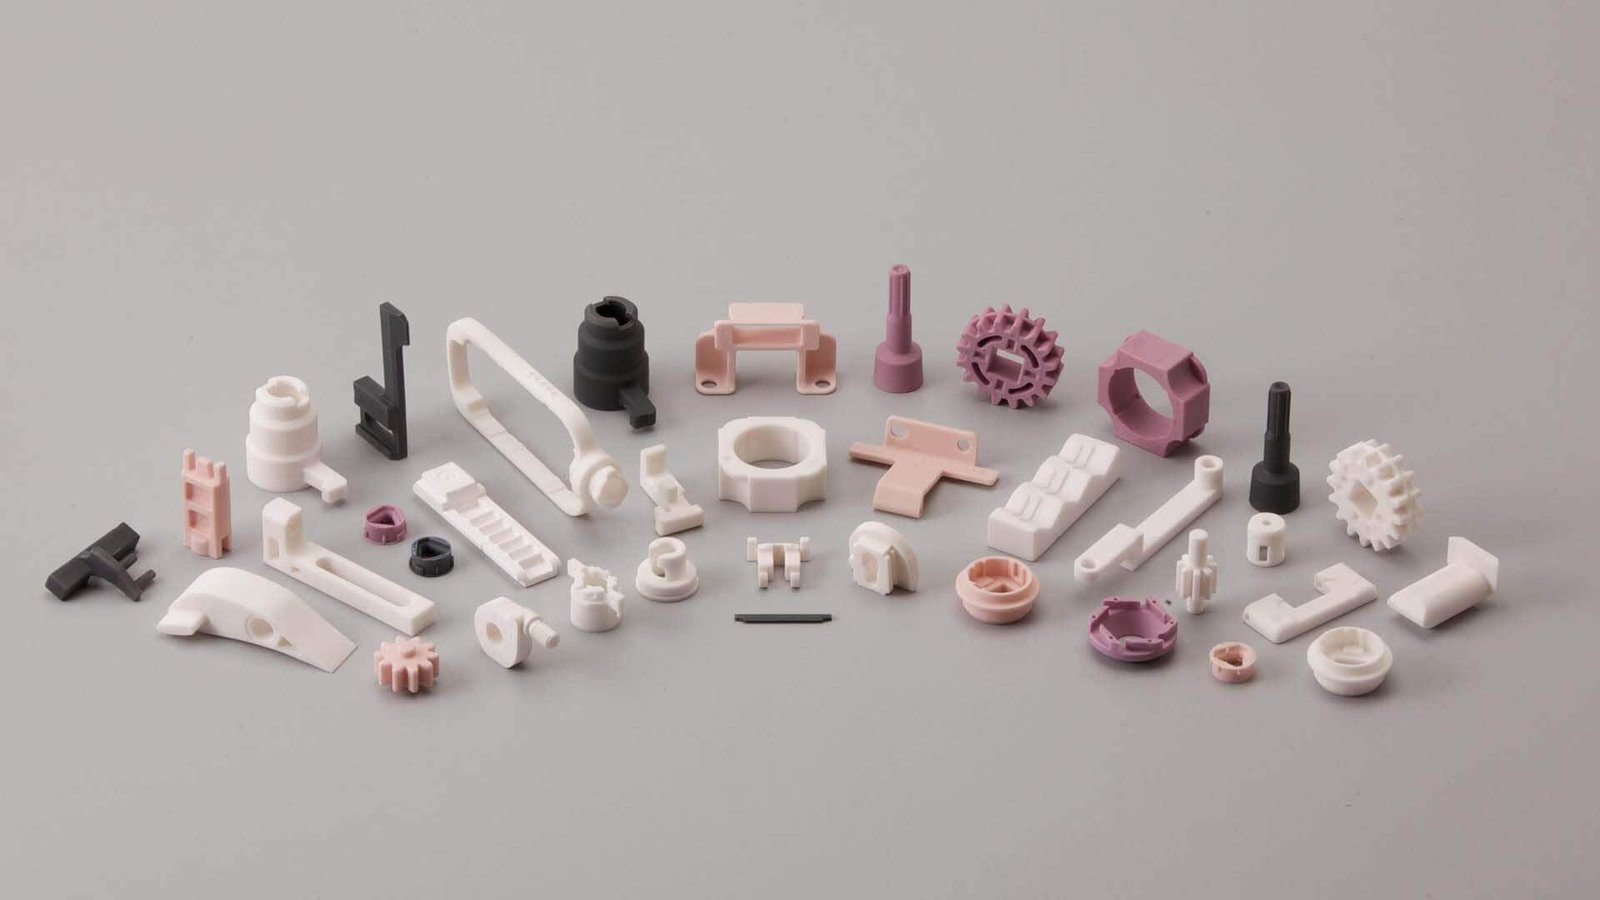
Zirconia Injection Molded Parts
Net-shape zirconia components for electronics, connectors and wear applications produced via CIM with post-sintering dimensional control. Typical sintered tolerance +/-0.5 % linear, with optional CNC grinding to +/-0.01 mm. High fracture toughness, low thermal conductivity and biocompatibility—delivered with material certificates, FAI reports and full traceability from feedstock batch to final inspection.
Get a Quote
Alumina Injection Molded Parts
Alumina injection molded parts for insulation, thermal management and structural applications in 5G, automotive sensors and industrial electronics. Alumina 95 % and 99 % grades available. CIM tooling designed for complex geometries—thin walls, internal channels, integrated threads—sintered to target density and inspected via Nikon toolmaker’s microscope and ZEISS MICURA CMM for critical dimensions and surface integrity.
Get a Quote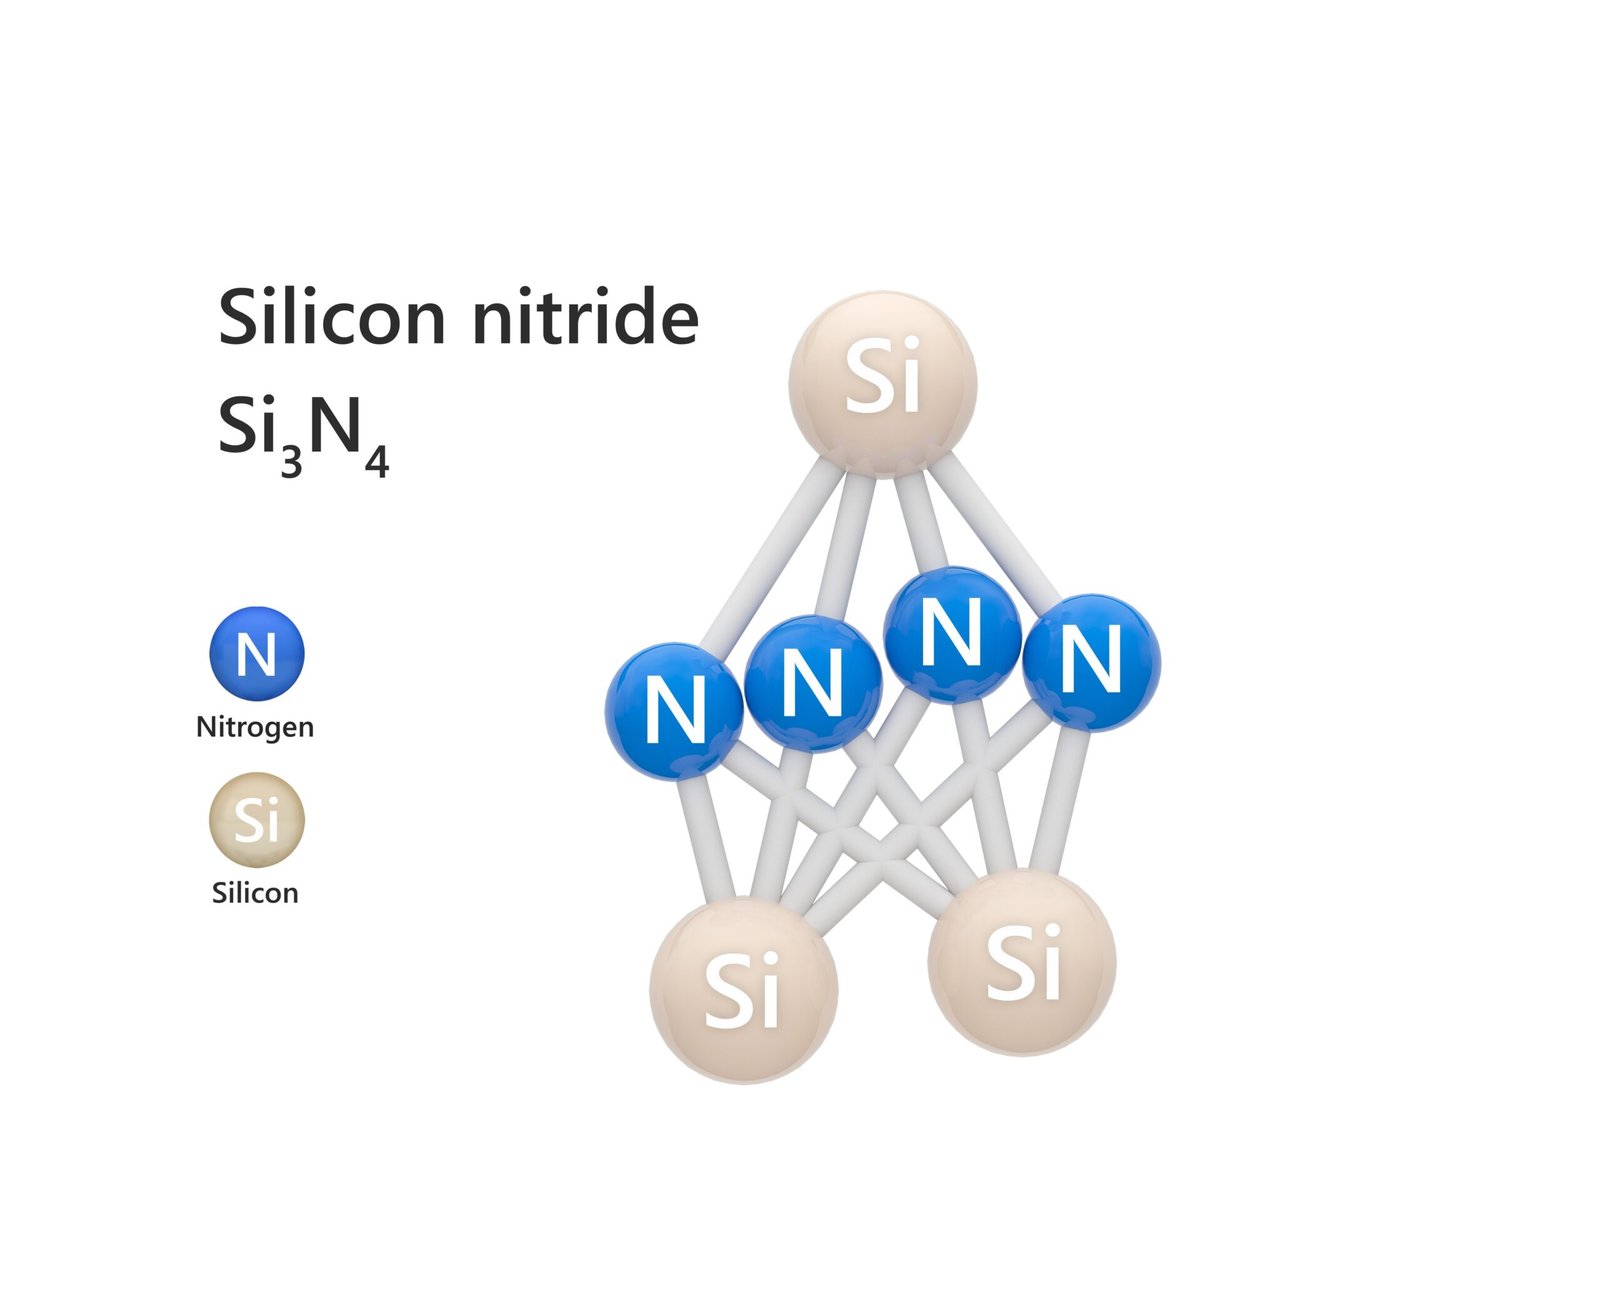
Silicon Nitride Components
Silicon nitride components machined and molded for high-temperature, high-wear and corrosive environments in automotive powertrains, robotics and medical devices. Exceptional thermal shock resistance and mechanical strength at elevated temperature. XUXIANG supplies both CIM-formed net shapes and post-sintered CNC-machined parts with tolerances to +/-0.01 mm, supported by spectral material analysis and dimensional FAI documentation.
Get a Quote
Medical Ceramic Components
Medical-grade ceramic components for surgical instruments, orthopedic implants, diagnostic devices and drug-delivery systems. Zirconia and alumina parts held to ISO 13485–compatible traceability standards, with biocompatibility certificates, lot control and cleanroom-compatible packaging available. CIM tooling designed for complex anatomical geometries, micro-features and tight tolerances—validated through five-step QC and CMM inspection.
Get a Quote
5G Connector Ceramics
High-precision ceramic insulators, ferrules and housings for 5G board-to-board, RF and FPC connectors. Zirconia and alumina parts molded or machined to +/-0.01 mm for reliable signal integrity and mechanical alignment in high-density interconnects. Mirror-finish EDM tooling and post-sintering CNC grinding ensure low insertion force, dimensional repeatability and compatibility with automated assembly—delivered with full material and dimensional reports.
Get a Quote
Automotive Ceramic Parts
Automotive ceramic parts for ADAS sensors, BMS interconnects, powertrain temperature/pressure transducers and EV thermal-management modules. Alumina and silicon nitride components engineered for thermal cycling, vibration resistance and electrical isolation. CIM tooling and post-sintering machining held to +/-0.01 mm, with material certificates, FAI documentation and AEC-Q200–aligned testing available to support tier-supplier and OEM qualification programs.
Get a Quote
Post-Sintering CNC Machining
Precision CNC machining and grinding of sintered ceramic parts to final tolerances of +/-0.01 mm or tighter. Fanuc CNC centers and Dawn grinding equipment process zirconia, alumina and silicon nitride blanks into complex profiles, threads, bores and surface finishes down to Ra 0.2 µm. ZEISS MICURA CMM verification, Nikon microscope inspection and full dimensional reports ensure conformance to print—supporting both prototype and production volumes.
Get a QuotePrecision Materials for Ceramic Injection Molding Tooling
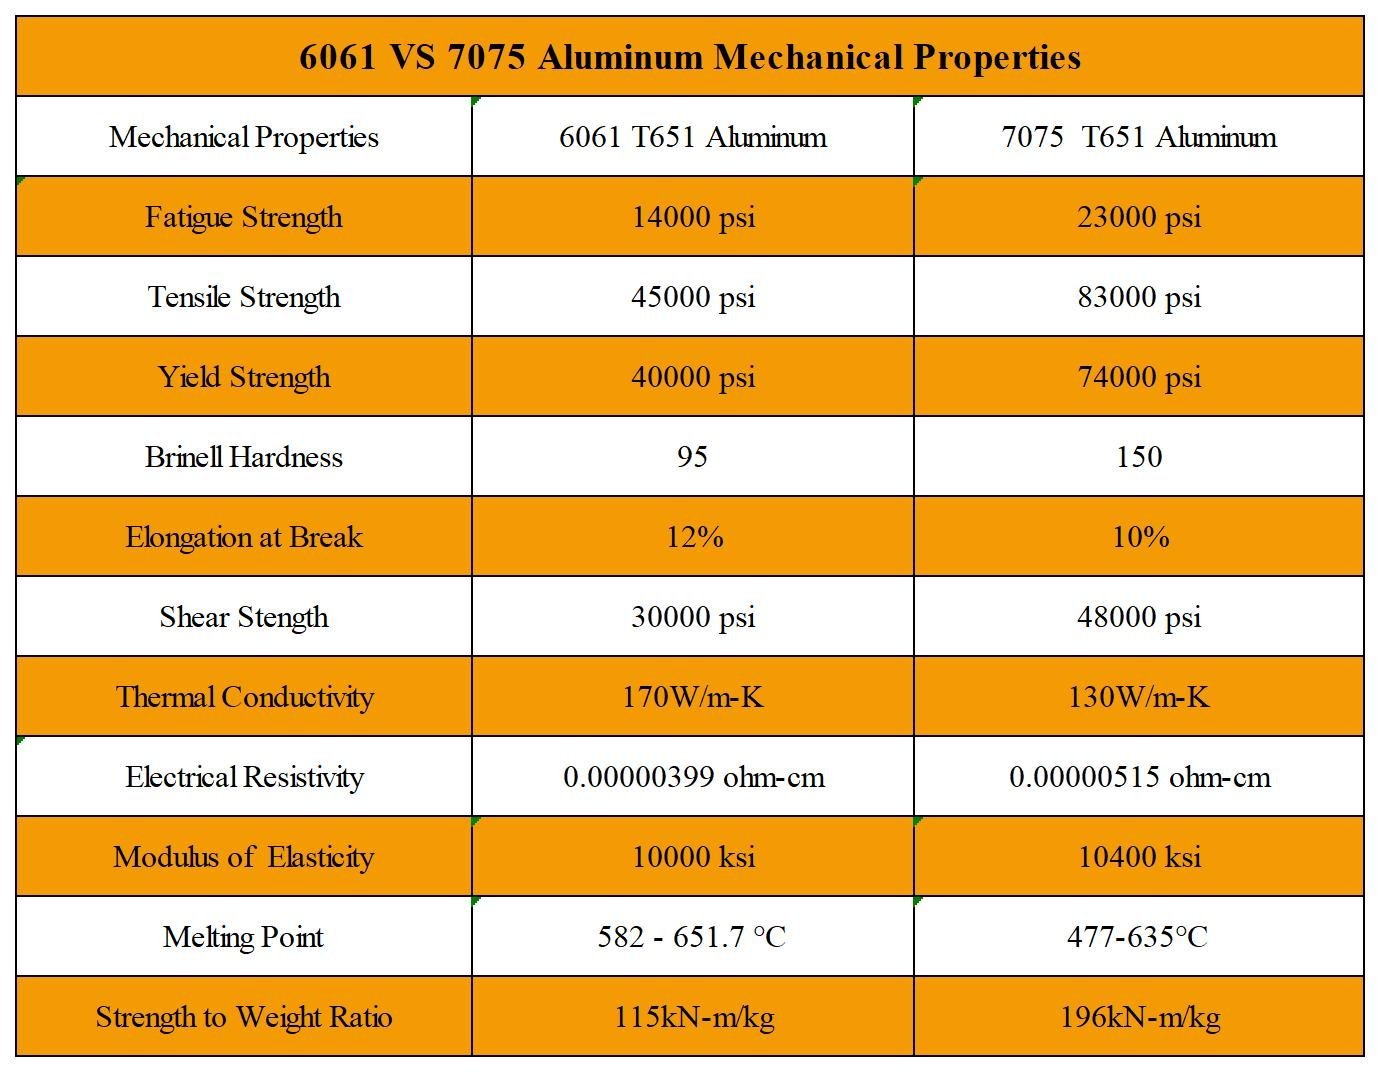
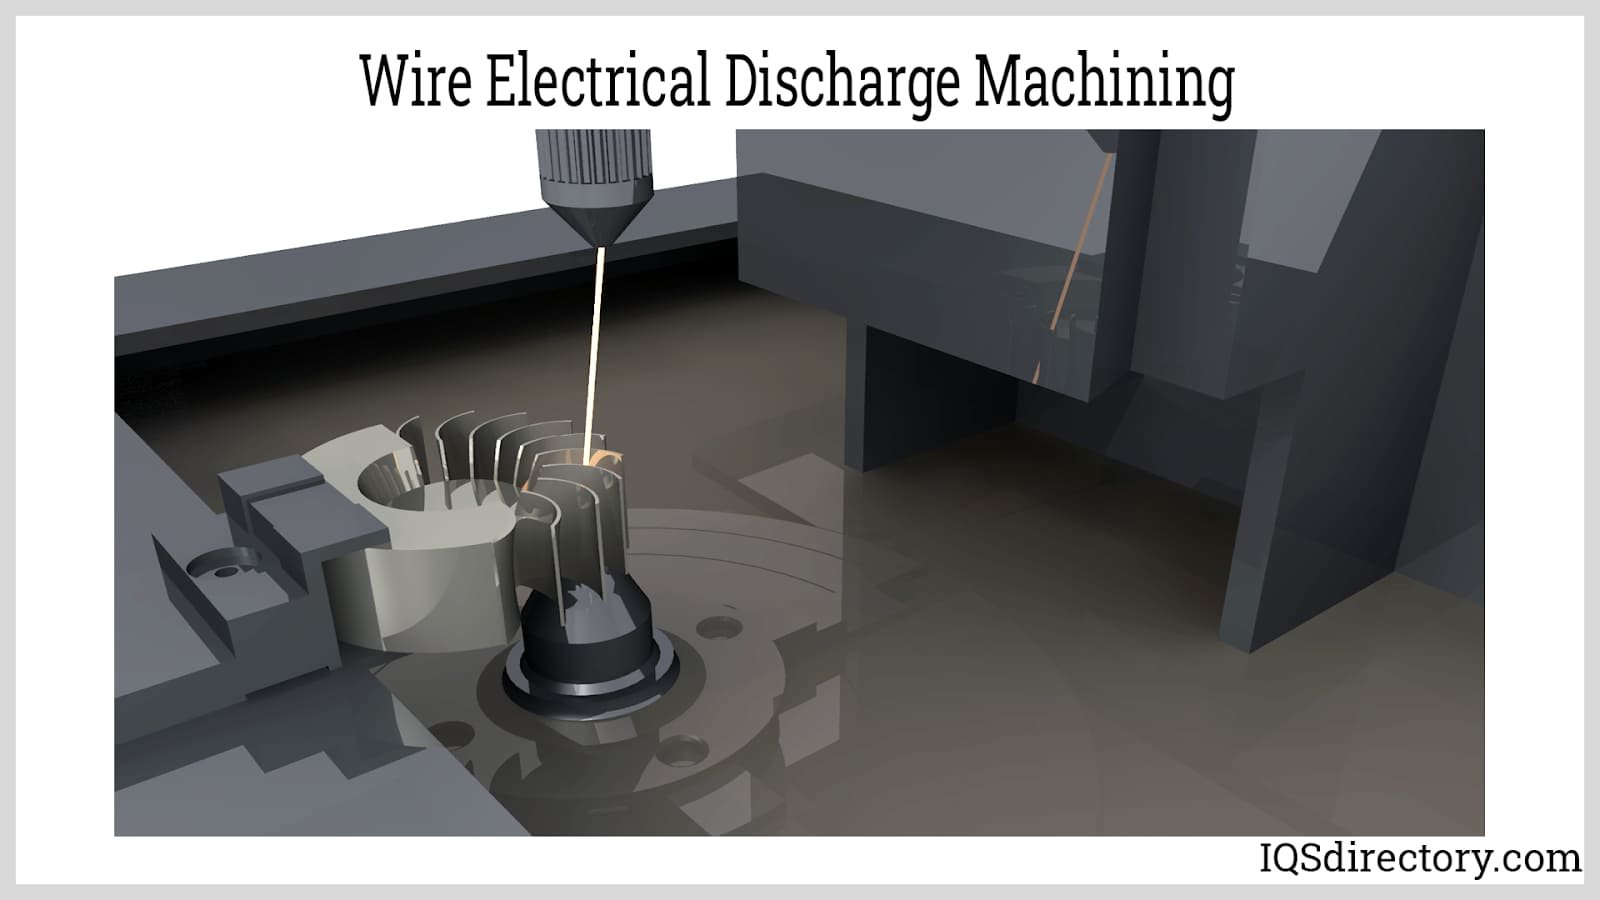
Advanced Manufacturing Processes for Ceramic Injection Molded Components
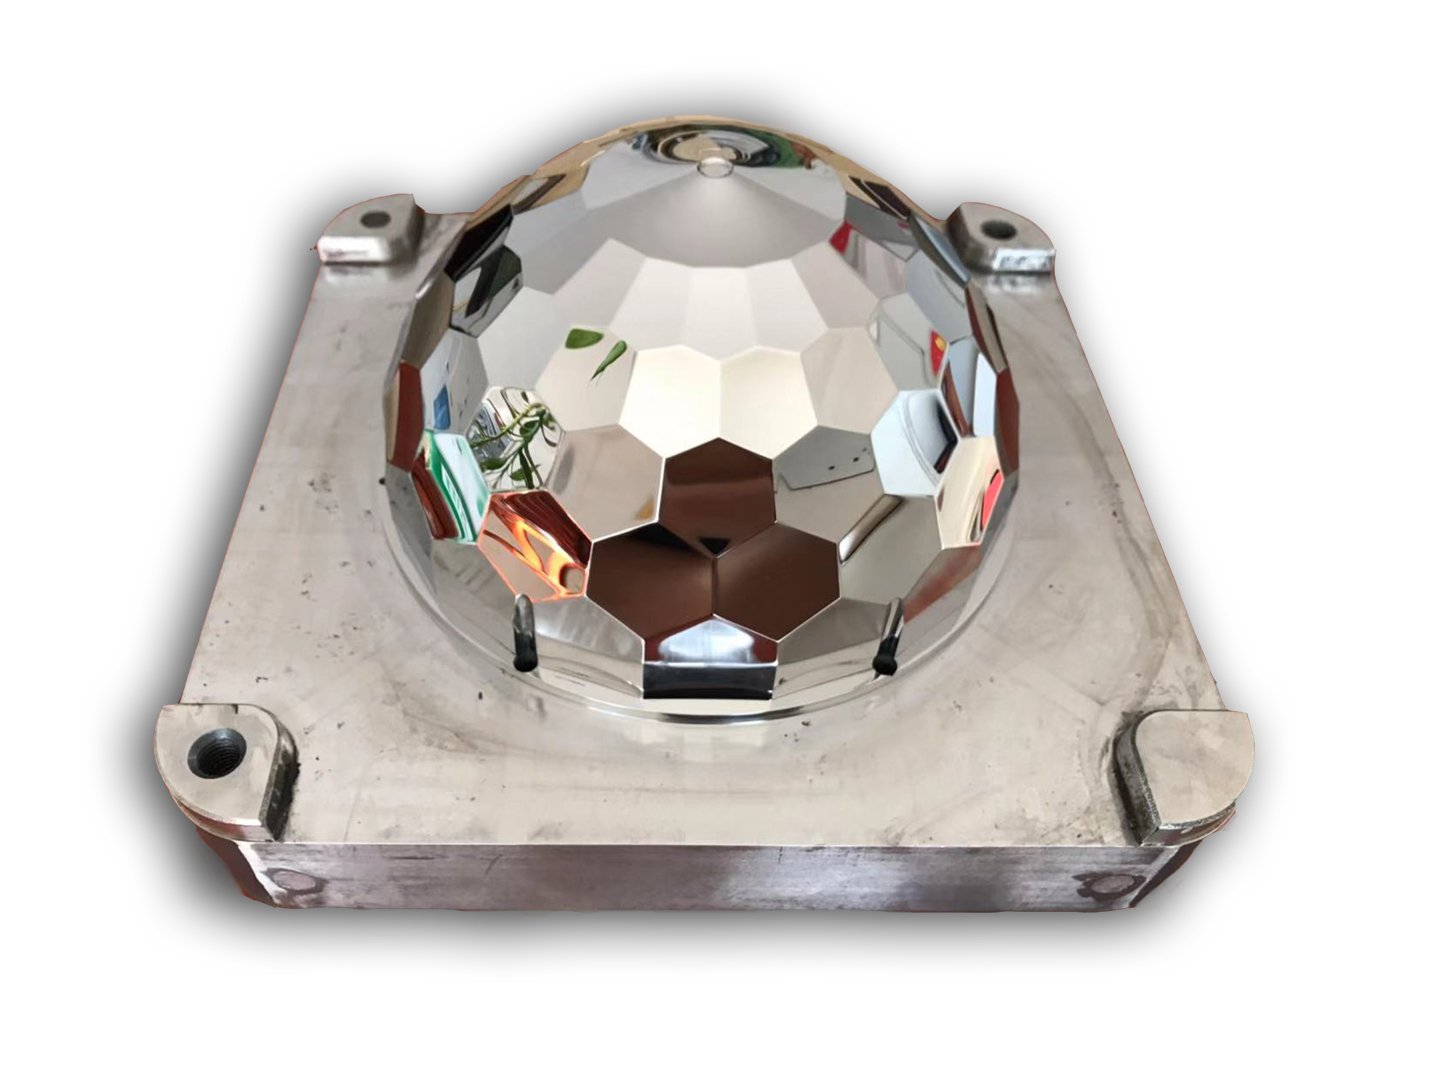
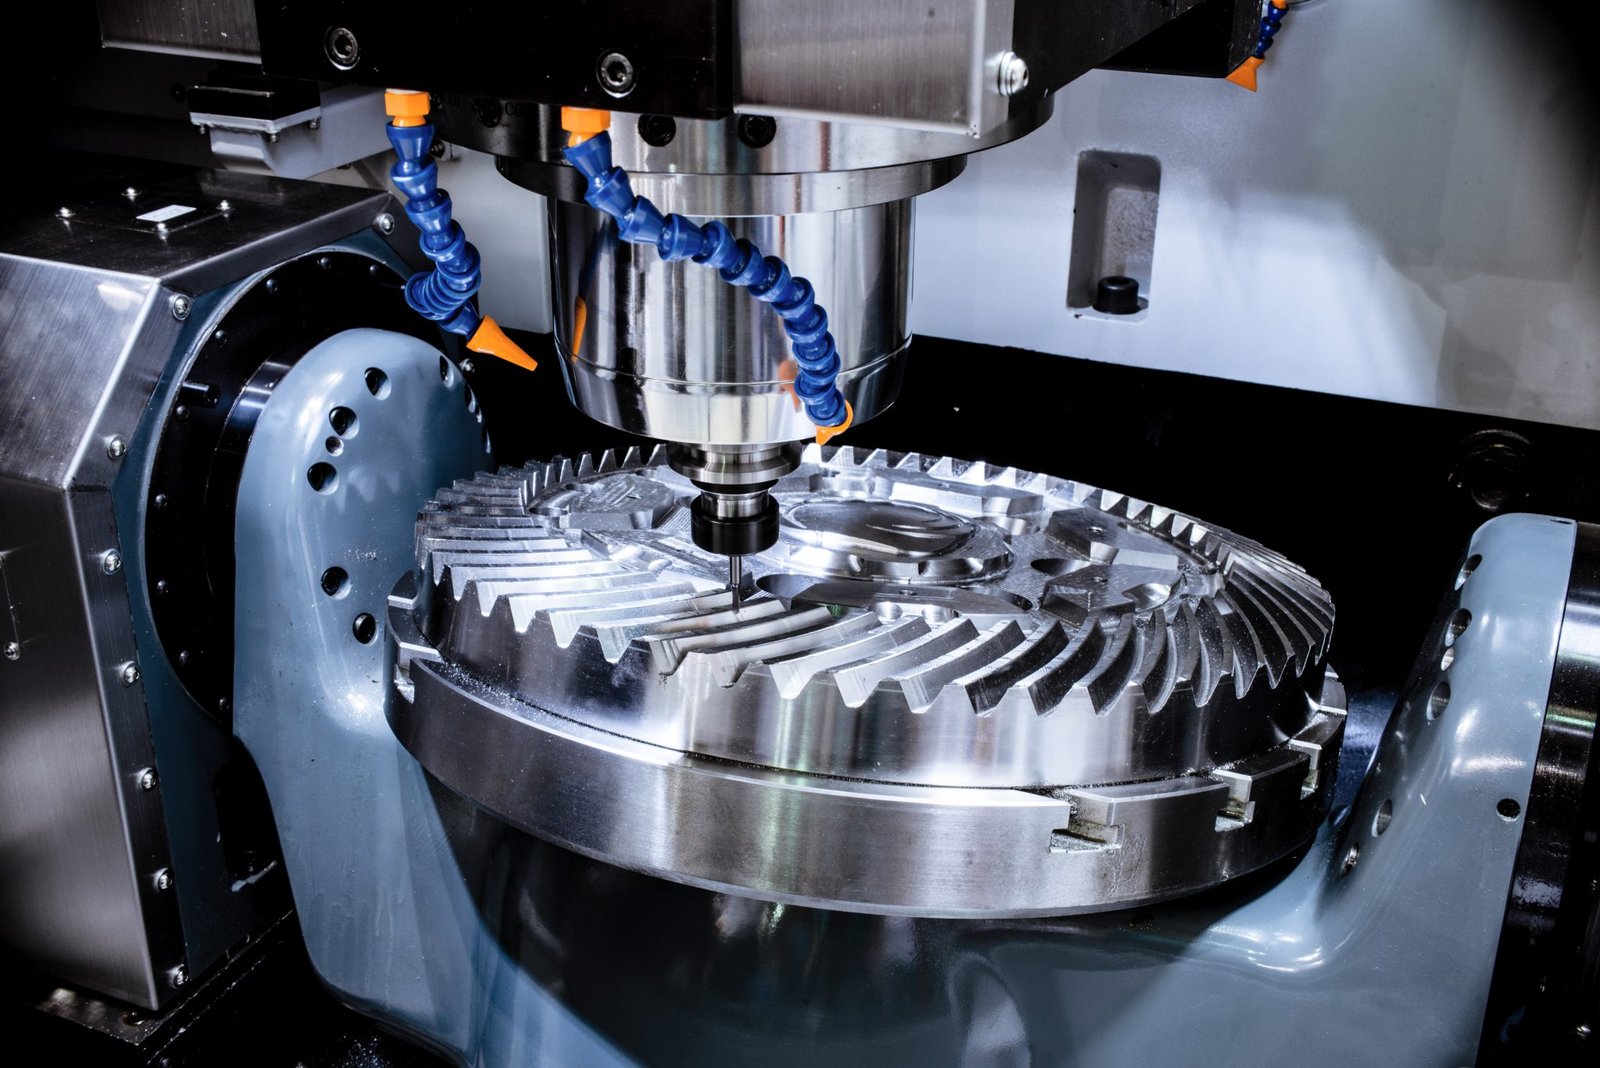
Mirror EDM
Mitsubishi mirror-grade electrical discharge machining delivers Ra 0.1um surface finishes on ceramic injection mold cavities and cores, eliminating secondary polishing while ensuring flawless part release and optical-grade surface replication in high-precision ceramic components.

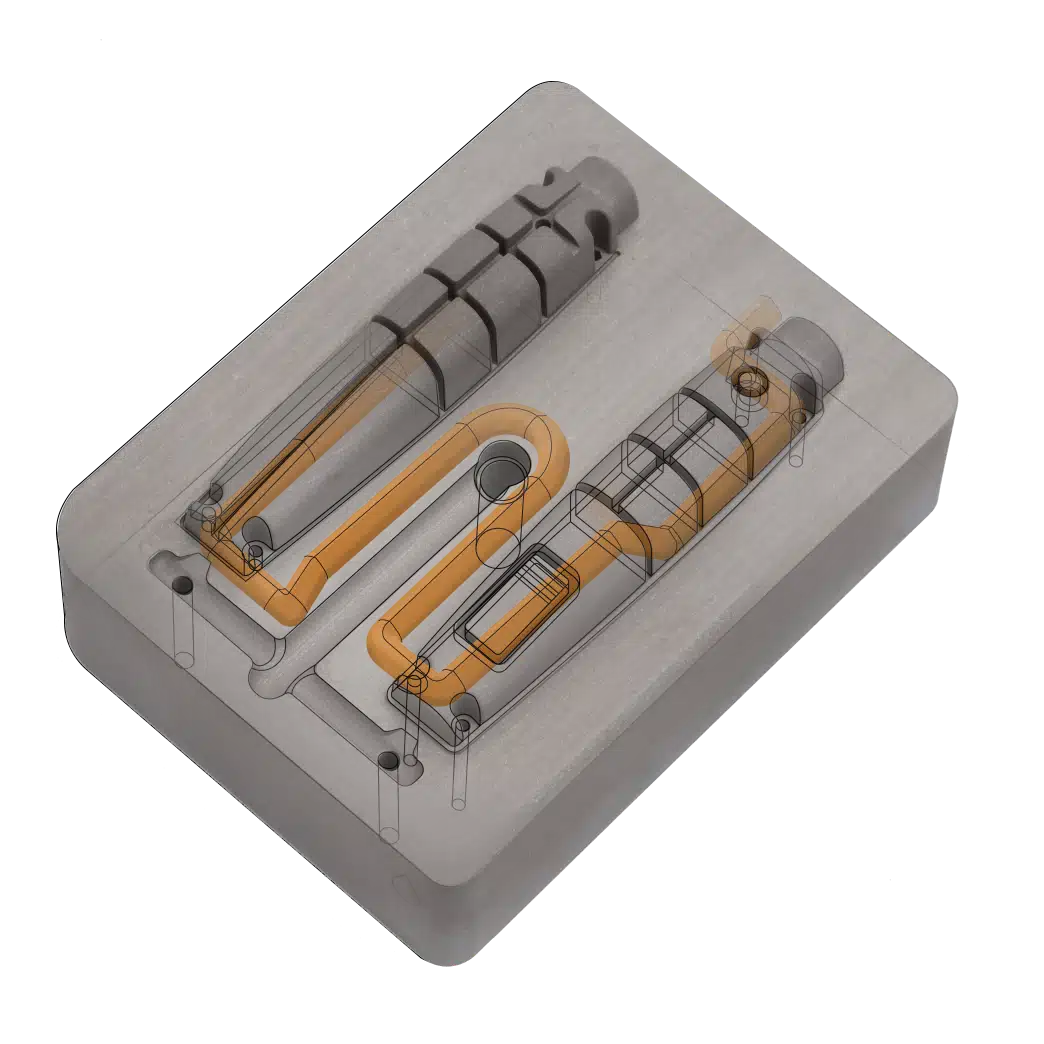
Conformal Cooling Integration
Advanced conformal cooling channels machined into ceramic injection mold cores reduce cycle times by up to 30%, improve part consistency and minimize warpage in high-precision ceramic components through optimized thermal control and uniform heat extraction across complex geometries.
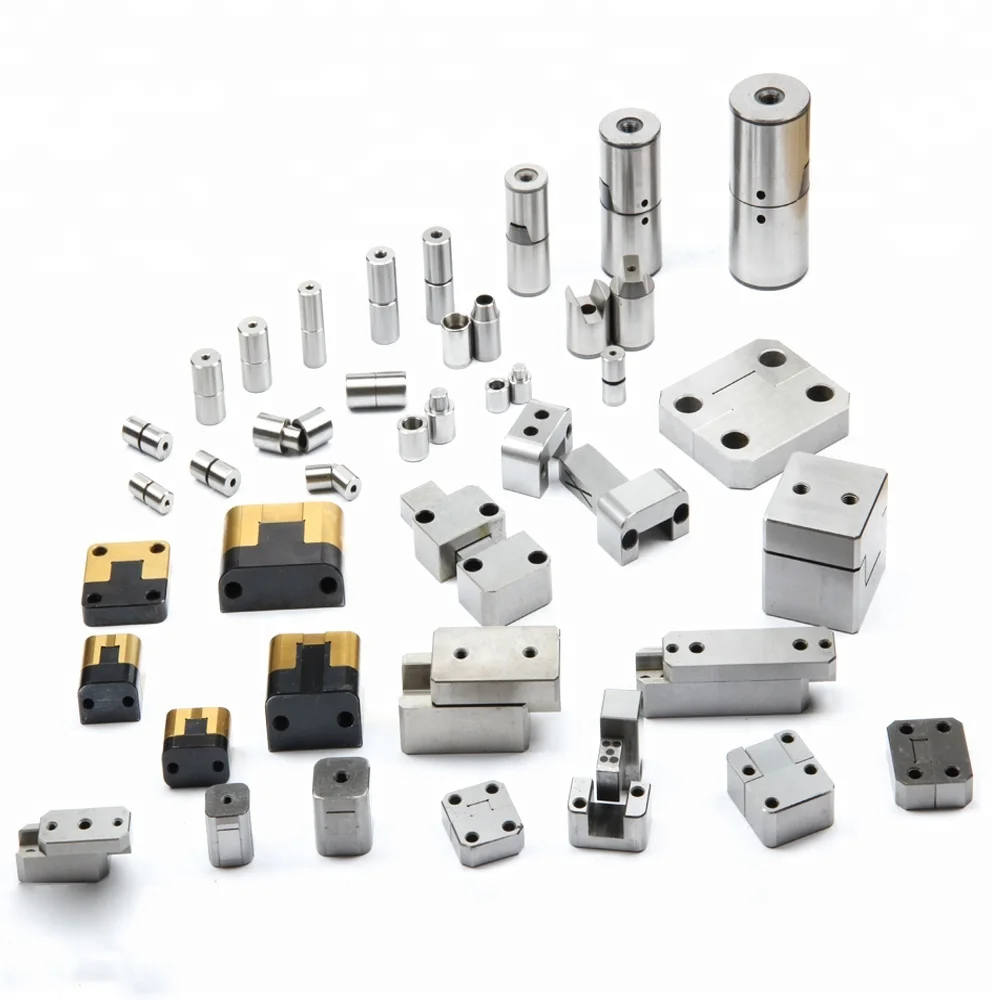
Precision Tooling Accessories & Inserts for Ceramic Injection Molded Components
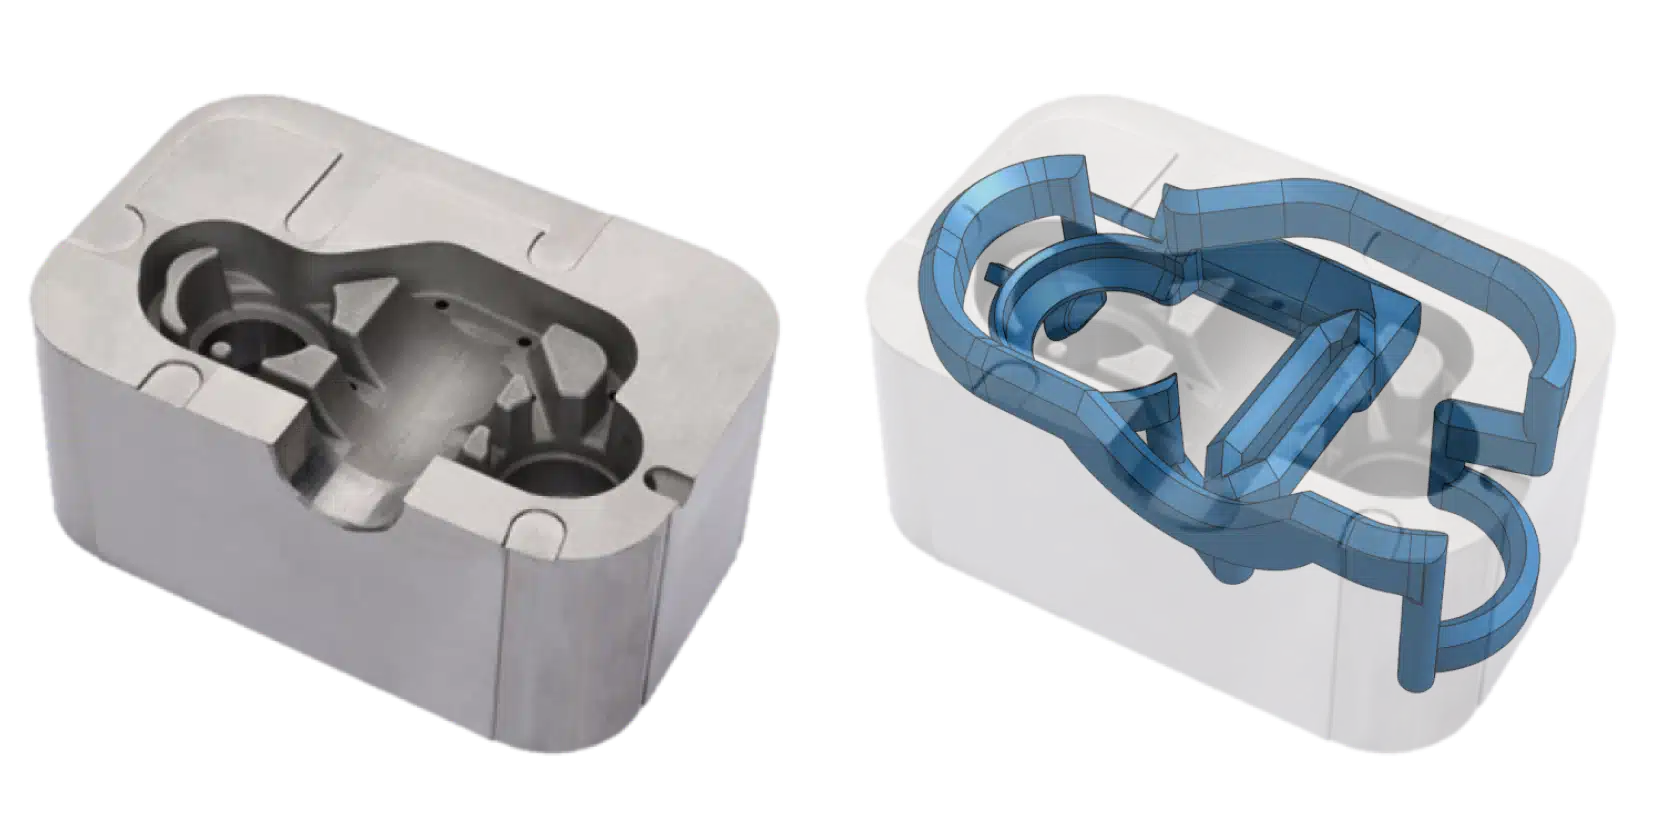
Conformal Cooling Cores
3D-contoured cooling channels for ceramic injection molds, designed via DFM collaboration and machined with Sodick slow-wire EDM. Reduces cycle time by up to 30% while maintaining micron-level dimensional stability across production runs.
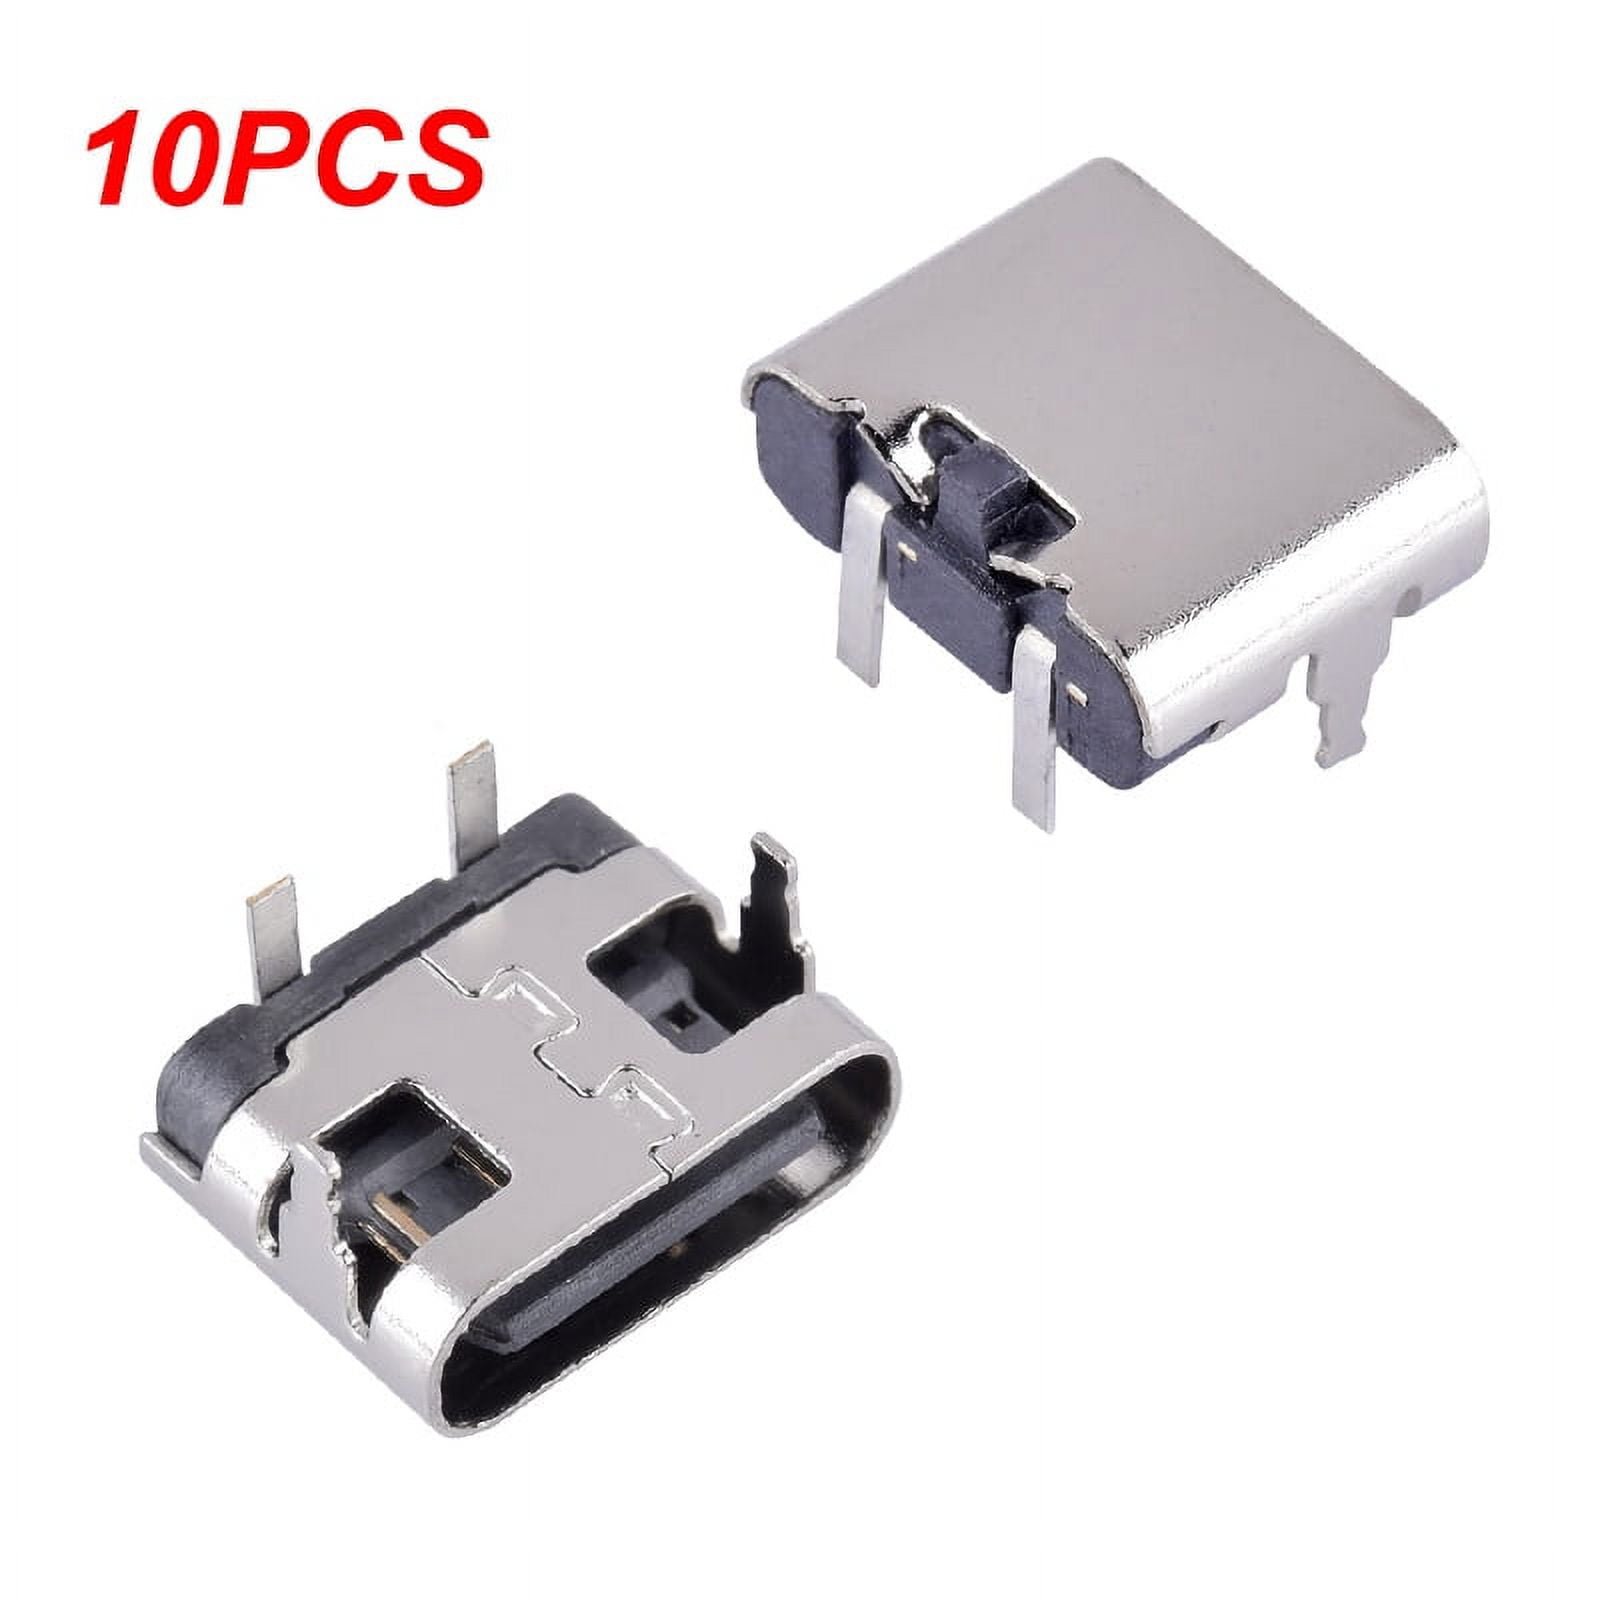
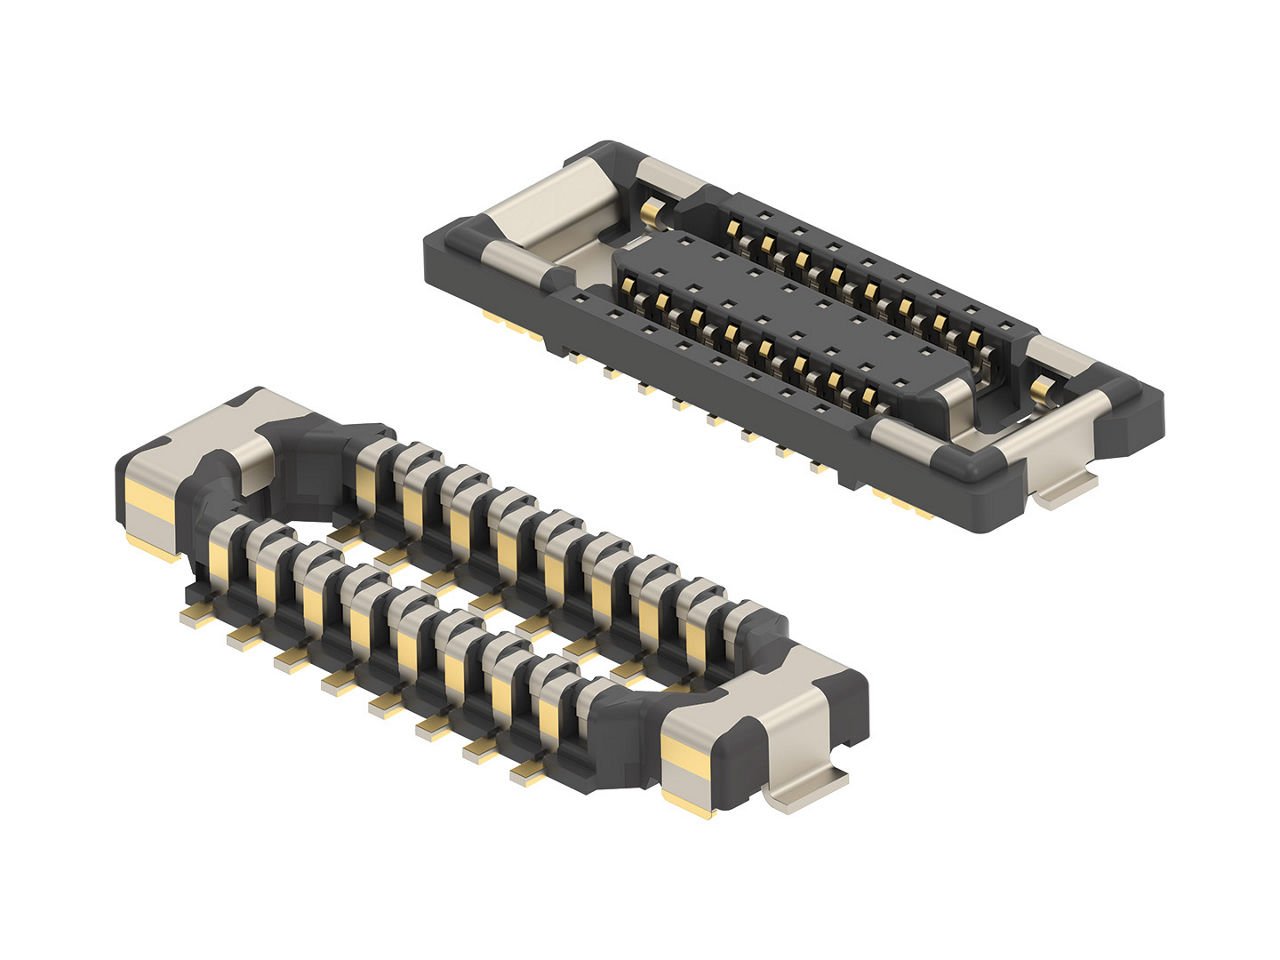
Board-to-Board Connectors
High-density terminal tooling for ceramic PCB interconnects in automotive ADAS and telecom infrastructure. Mitsubishi mirror EDM delivers Ra 0.1 μm surface finish, validated through five-step QC with full FAI documentation and material certificates.
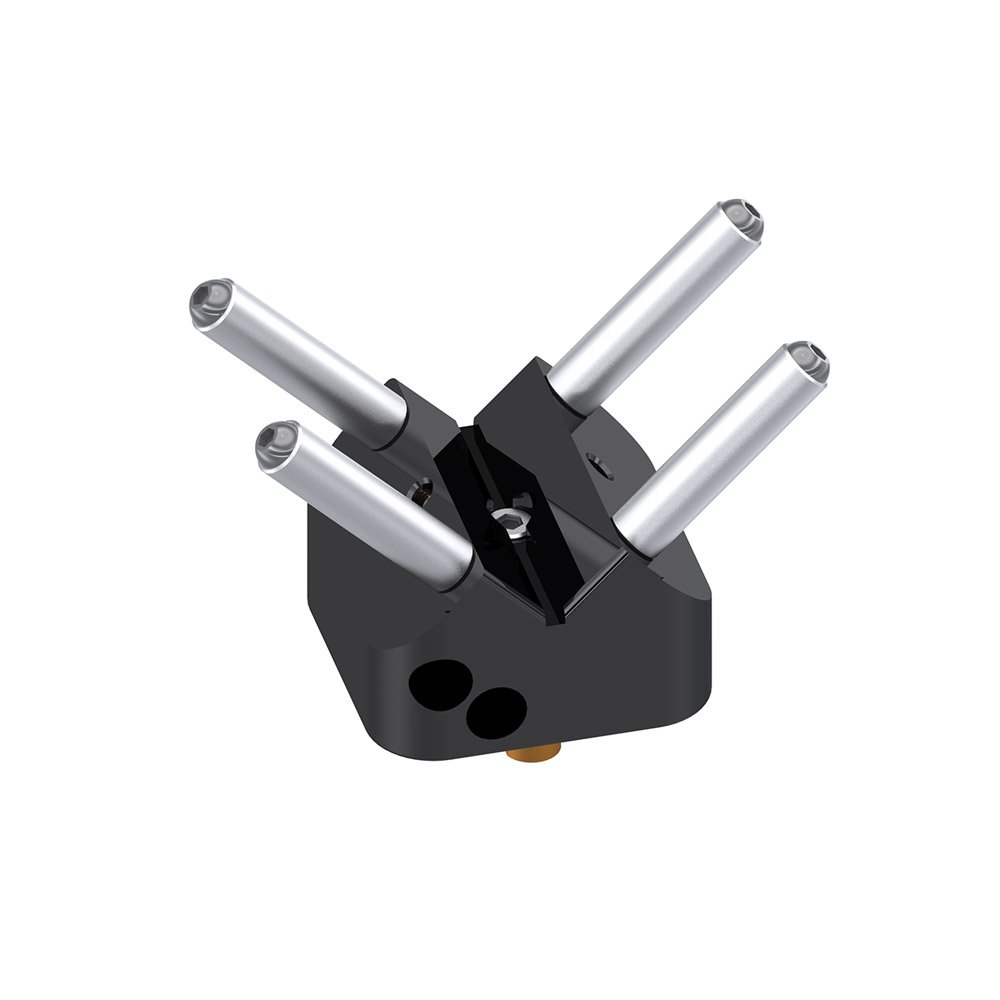
End-Effector Jigs
Precision fixtures and grippers for robotic handling of ceramic injection molded components during secondary operations. CNC-machined to +/-0.002 mm, with Nikon microscope verification, ensuring repeatable positioning in automated assembly and inspection lines.
Precision Tooling Accessories & Inserts for Ceramic Molding Programs
Founded in 2010 in Dongguan’s Chang’an manufacturing hub, XUXIANG has evolved from a specialist mold-core machining shop into a dual-factory precision manufacturing group serving electronics, 5G/telecom, automotive & NEV, and medical-device supply chains worldwide. Today we operate 2,000 m² of R&D and micro-machining capacity in Dongguan, plus a 1,400 m² volume-production facility in Quanzhou launched in 2025 — together delivering over 200% capacity growth and lead times roughly 30% faster than industry average.
Our mission is to solve the buyer’s two biggest pain points: tolerance failure and delivery delay. We’ve invested over CNY 8 million in Japanese, Swiss and German precision assets — Sodick and Seibu slow-wire EDM, Mitsubishi mirror EDM, Fanuc CNC and ZEISS MICURA CMM metrology measuring to 0.7 µm — enabling +/-0.001 mm machining precision and Ra 0.1 µm mirror-grade finishes on ceramic injection molded components and high-performance tooling.
Every project receives DFM feedback from 10+ engineering experts before production and passes a five-step validated QC flow — material spectral analysis, in-process tolerance monitoring, ZEISS/Nikon CMM verification, surface-integrity checks and full FAI documentation with material certificates. ISO 9001:2015 governs every process, and we return quotes within 24 hours, ensuring dependable quality, responsive service and transparent pricing for precision mold components that perform.
Precision Ceramic Injection Molded Components — Engineering-Grade Accuracy
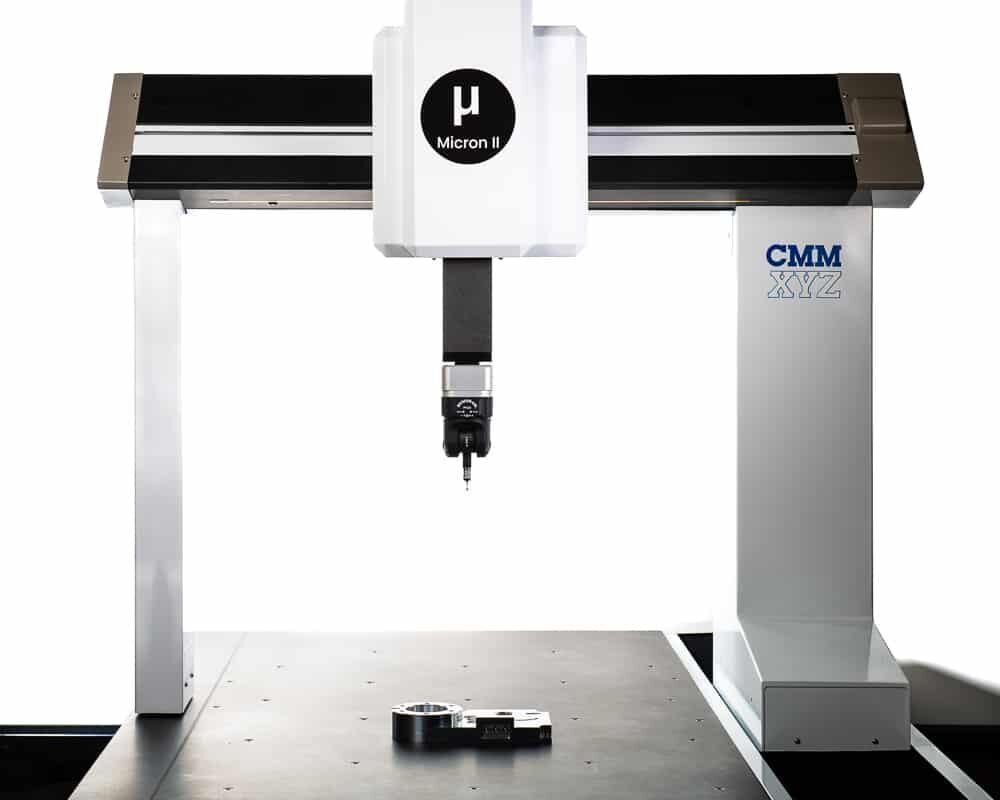
Micron-Stable Machining & Metrology
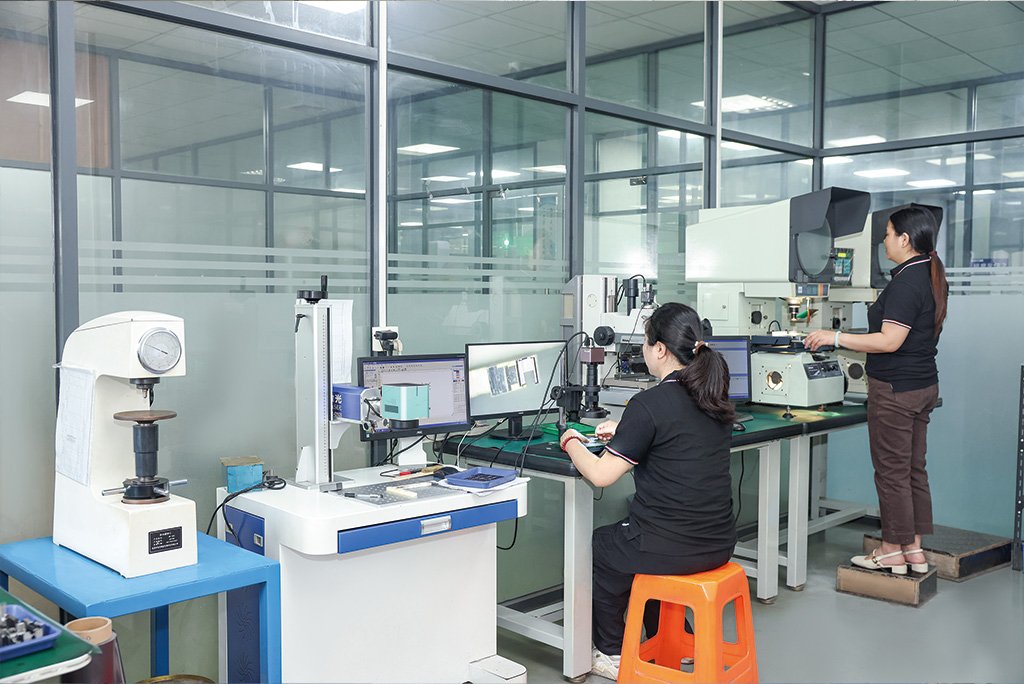
Every ceramic injection molded component is validated through ZEISS MICURA CMM measuring to 0.7um and Nikon V-12B toolmaker’s microscopes, ensuring +/-0.001 mm machining precision across complex geometries, thin walls and tight-tolerance core inserts for electronics, automotive and medical applications.
- ZEISS MICURA CMM with 0.7um resolution for sub-micron dimensional verification
- Nikon V-12B and MM-400 class toolmaker's microscopes for edge and surface inspection
- +/-0.001 mm maximum machining accuracy on CNC, EDM and grinding operations
- Full FAI documentation with material certificates and inspection reports for every shipment
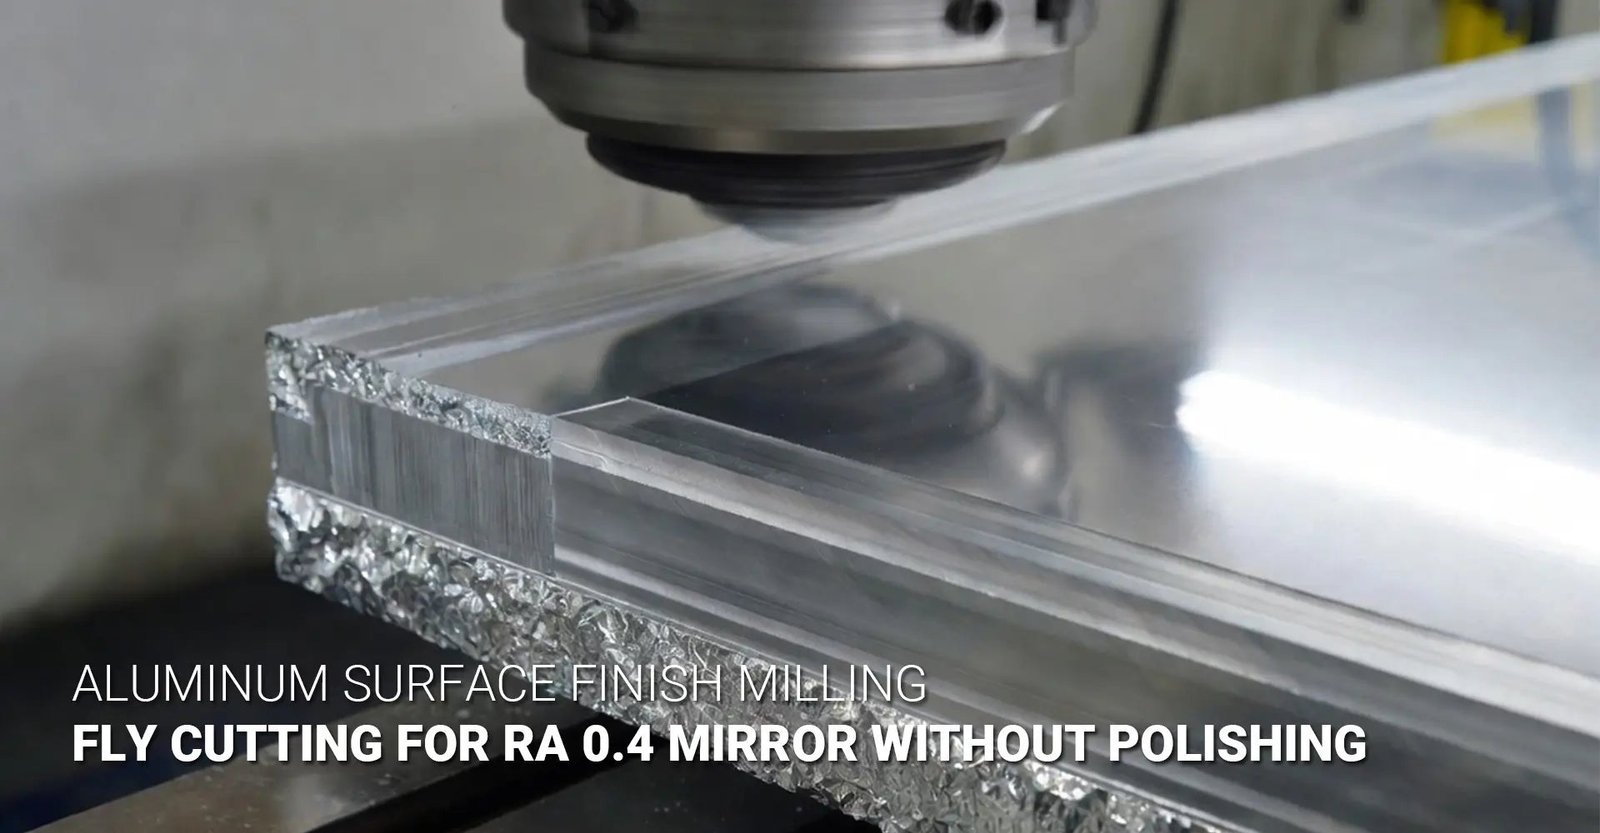
Mirror-Grade EDM & Corner-Radius Mastery
Sodick and Seibu slow-wire EDM, combined with Mitsubishi mirror EDM, deliver Ra 0.1um surface finishes and corner radii down to R ≤ 0.015 mm — critical for high-density micro-connector tooling, conformal cooling channels and zero-draft ceramic mold cores.
- Ra 0.1um mirror-grade EDM finish for optical-class surface quality
- Corner radii down to R ≤ 0.015 mm for micro-pin and thin-wall tooling
- +/-0.002 mm class positioning on slow-wire EDM; +/-0.003 mm on sinker EDM
- Sodick, Seibu and Charmilles EDM assets for complex 3D cavity and insert work
Full DFM Engineering Support
Before production begins, 10+ precision-mold engineers review your CAD files for manufacturability, tolerance feasibility and material selection — providing DFM feedback, cost-optimization suggestions and full FAI reports to eliminate tolerance failures and costly rework cycles.
- DFM review by 10+ engineers with 16 years of precision-mold experience
- Five-step QC flow: material spectral analysis, in-process monitoring, CMM verification, surface checks, FAI
- Full first-article inspection reports with dimensional data and material certificates
- ISO 9001:2015 quality system governing every project from quote to shipment
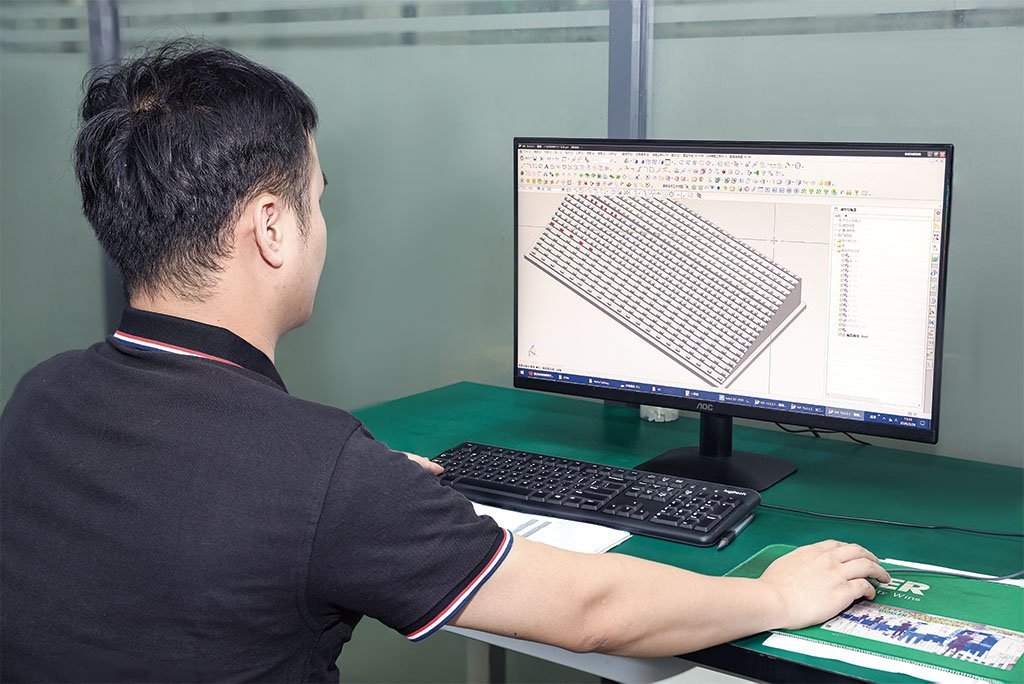
Dual-Factory Speed & Capacity
With 2,000 m² in Dongguan for R&D and micro-machining plus 1,400 m² in Quanzhou for volume production, XUXIANG delivers samples in 3–7 days and mass production in 15–25 days — roughly 30% faster than industry average, with +200% capacity since 2025.
- Dual factories: Dongguan (R&D, micro-machining) + Quanzhou (volume production)
- 3–7 days for sample parts; 15–25 days for mass production runs
- +200% annual output capacity since 2025 expansion in Fujian province
- 24-hour quote turnaround with transparent pricing and lead-time commitment
XUXIANG vs. Typical Ceramic Injection Molded Component Suppliers
Evidence-based comparison: what sets precision-grade tooling apart from commodity mold shops.
← 左右滑动查看 →
How We Manufacture Ceramic Injection Molded Components
Every ceramic injection molded component follows a rigorous six-phase process—from CAD intake and DFM engineering through ZEISS CMM validation and full FAI traceability—ensuring +/-0.001 mm precision, mirror-grade finishes and on-time delivery.
CAD Intake & DFM Review
Your design is analyzed by 10+ engineers for moldability, tolerance feasibility and cost optimization. DFM feedback is returned within 24 hours to prevent downstream rework and accelerate toolpath planning.
Material Selection & Electrode Design
We specify carbide, tool steel or copper-tungsten electrodes and validate material certificates via spectral analysis. Electrode geometry is optimized on Beijing Jingdiao high-precision CNC to achieve Ra 0.1um EDM finishes.
EDM & CNC Machining with In-Process Monitoring
Sodick slow-wire EDM, Mitsubishi mirror EDM and Fanuc CNC machines hold +/-0.001 mm tolerances. Real-time SPC monitors dimensional drift, and corner radii down to R 0.015 mm are validated at each setup.
ZEISS & Nikon CMM Validation
Parts are validated—not merely inspected—on a ZEISS MICURA CMM measuring to 0.7um and Nikon toolmaker’s microscopes. Every critical dimension is compared against nominal CAD values with full deviation reports.
FAI Documentation & Material Certificates
A five-step QC flow generates first-article inspection reports, surface-integrity checks and certified material traceability documents. ISO 9001:2015 governs every record, ensuring full auditability for aerospace, automotive and medical applications.
Secure Packaging & Delivery
Finished ceramic injection molded components are cleaned, inspected for surface defects, packaged in anti-static or foam-lined trays and shipped with courier tracking. Lead times: 3–7 days for samples, 15–25 days for production.
How to Partner with XUXIANG for Ceramic Injection Molded Components
From CAD upload to validated delivery, our five-step process combines 24-hour quoting, DFM engineering support and full FAI documentation — so you receive precision tooling on time, every time.
Submit CAD and Technical Requirements
Upload your 3D files, drawings and specifications through our secure portal. Our engineering team reviews tolerances, material requirements and production volumes to prepare a tailored quote.
Receive 24-Hour Quote with DFM Feedback
Within 24 hours, you receive a detailed quotation plus design-for-manufacturability insights from our 10+ precision-mold experts, identifying potential tolerance risks and cost-saving opportunities before production begins.
Approve First-Article Samples
We machine and deliver first-article samples in 3–7 days, validated on our ZEISS MICURA CMM to +/-0.001 mm. You inspect, test fit and approve before any mass production starts.
Launch Mass Production
After sample approval, full production runs 15–25 days on Sodick slow-wire EDM, Fanuc CNC and mirror EDM — each part monitored through our ISO 9001:2015 five-step QC flow for micron-stable consistency.
Receive Parts with FAI and Certificates
Every shipment includes complete FAI reports, CMM inspection data and material certificates, giving you full traceability and confidence for your assembly line or next-stage tooling integration.
Quality Certifications for Ceramic Injection Molded Components
Customer Outcomes — Precision Ceramic Injection Molded Components Delivered
XUXIANG’s ceramic injection molded components held +/-0.002 mm on our 5G connector tooling across 50,000 cycles. We cut validation time by 40% and launched two months ahead of schedule.
The mirror EDM finish on our ADAS sensor housings eliminated secondary polishing entirely. Cost per unit dropped 22%, and every shipment arrived with full FAI reports — zero quality escapes in 18 months.
We needed ceramic injection molded components for implantable device tooling with sub-micron repeatability. XUXIANG’s ZEISS CMM validation gave us audit-ready traceability, and lead time was 30% faster than our previous supplier.
FAQ — Ceramic Injection Molded Components & Precision Tooling
What is the minimum order quantity (MOQ) for ceramic injection molded components?
What are typical lead times for samples and mass production of ceramic injection molded components?
Do you charge for sampling and NRE (non-recurring engineering) on ceramic injection molded components?
What payment terms does XUXIANG offer for ceramic injection molded components?
How do you handle shipping, insurance and customs for international orders of ceramic injection molded components?
What IP protection and NDA policies are in place for custom ceramic injection molded components?
What tolerance guarantees apply to ceramic injection molded components?
Do you provide material certifications and traceability for ceramic injection molded components?
Is there a fee for design-for-manufacturability (DFM) support on ceramic injection molded components?
The Complete Buyer’s Guide to Ceramic Injection Molded Components for Precision Manufacturing
Navigate the complexities of sourcing ceramic injection molded components with confidence. This guide delivers a proven decision framework, critical supplier evaluation criteria, material selection insights, and the most common procurement mistakes to avoid when specifying high-precision ceramic parts.
1. What Are Ceramic Injection Molded Components?
Ceramic injection molding (CIM) combines fine ceramic powder—typically alumina, zirconia or silicon nitride—with a thermoplastic binder system at loadings of 50–65 vol.%, then injects the feedstock into precision steel molds under pressures of 50–150 MPa. After molding, the green part undergoes catalytic or thermal debinding to remove the polymer, followed by high-temperature sintering at 1,400–1,700 °C, which densifies the ceramic to over 98% theoretical and shrinks the part by 15–20% in each axis. CIM enables complex three-dimensional geometries—undercuts, threads, thin walls below 0.3 mm—in a single shot, without secondary machining.
2. Evolution and History of Ceramic Injection Molding
Ceramic injection molding emerged in the mid-1970s when European aerospace researchers combined polymer injection-molding techniques with powder-metallurgy feedstocks to produce turbine blades and thermal-barrier components. Early trials demonstrated that complex geometries previously requiring hand-layup or multi-axis machining could be net-shaped in minutes, though binder burnout and sintering shrinkage remained inconsistent.
By the late 1980s, advances in wax-polymer binder systems and computer-controlled sintering furnaces brought dimensional repeatability within +/-0.5% — precise enough for electronics housings and automotive sensor bodies. Aerospace adoption accelerated as CIM delivered weight savings of 30–40% versus machined metal in high-temperature applications.
The 1990s miniaturization wave in mobile electronics and fiber optics drove demand for sub-millimeter ceramic ferrules, sleeves and micro-connectors. CIM became the only economically viable route: machining a single zirconia ferrule cost $8–12, while molded equivalents reached $0.15–0.40 at volume.
Today, feedstock formulations achieve sintered tolerances of +/-0.01 mm, and cycle times under 15 seconds enable annual outputs exceeding 50 million parts per mold — transforming CIM into the backbone of 5G antenna components, medical implant housings and EV power-module insulators.
3. Types of Ceramic Injection Molded Components
Ceramic injection molded components serve distinct functional roles across industries, each demanding specific geometries, tolerances and material systems. Understanding these categories helps procurement teams specify the right technical requirements and qualify suppliers with proven domain expertise.
Structural and Mechanical Parts

Insulators, bushings and ceramic bearings dominate this category. Typical geometries include cylindrical sleeves, flanged bushings and ring-shaped insulators with wall thicknesses from 0.5 to 5 mm. Tolerances range from ±0.05 mm for general industrial use to ±0.01 mm for high-precision automation fixtures. Alumina and zirconia are preferred for wear resistance and electrical isolation.
Electronic Substrates and Housings
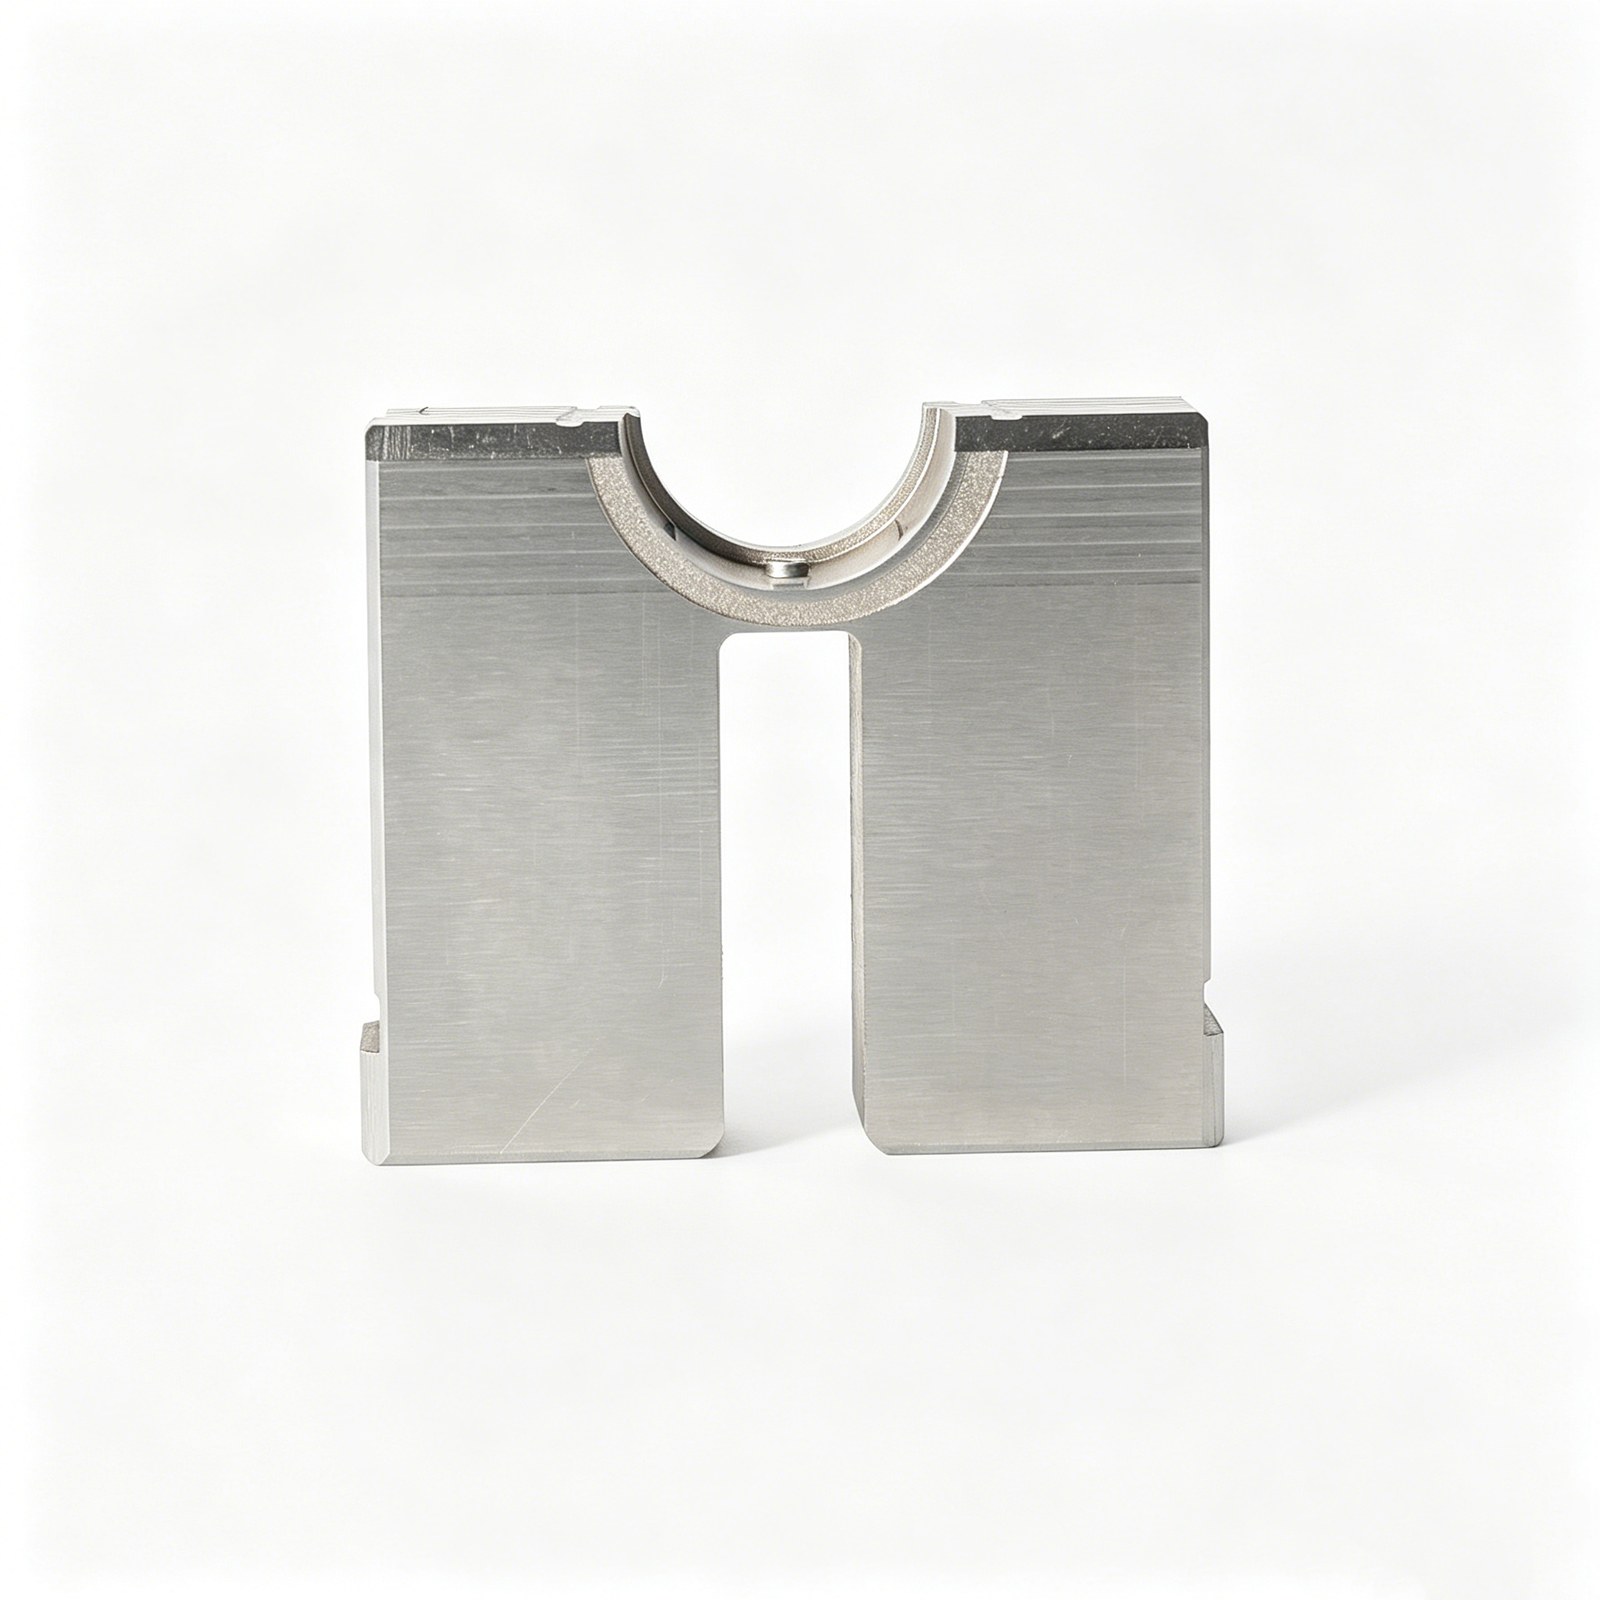
Substrates for hybrid circuits and RF modules require flatness under 0.02 mm and surface finishes below Ra 0.4 µm. Housings for sensors and connectors feature thin walls (0.3–1.0 mm) and complex internal channels. Alumina and aluminum nitride (AlN) are standard for thermal management and dielectric performance in 5G and telecom applications.
Medical Implants and Surgical Instruments
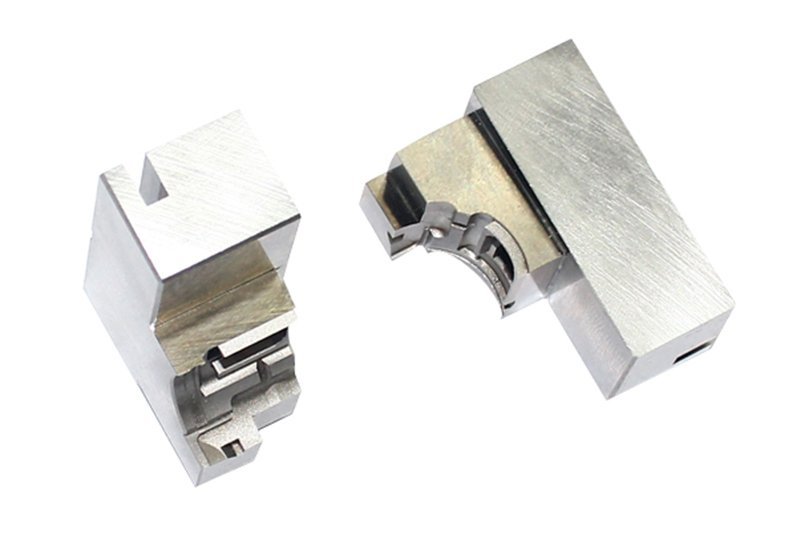
Biocompatible zirconia components — hip-ball heads, dental abutments, surgical blade inserts — demand tolerances of ±0.005 mm and mirror finishes (Ra ≤ 0.1 µm). Geometries are often contoured or threaded. ISO 13485 traceability and material certification are mandatory for this segment.
Micro-Connectors and Telecom Fixtures
High-density terminal ferrules, fiber-optic alignment sleeves and micro-pin insulators require inner-diameter tolerances of ±0.002 mm and concentricity under 0.01 mm. Wall thicknesses drop to 0.2–0.5 mm. Alumina and stabilized zirconia ensure dimensional stability across thermal cycling in 5G infrastructure and mobile devices.
4. Materials for Ceramic Injection Molded Components
Ceramic injection molding feedstocks rely on fine ceramic powders blended with thermoplastic binders. The four most common materials—alumina, zirconia, silicon nitride and aluminum nitride—each deliver distinct thermal, mechanical and electrical properties that map directly to application requirements in electronics, automotive sensors and medical implants.
| Material | Density (g/cm³) | Max Use Temp (°C) | Dielectric Strength (kV/mm) | Cost Tier |
|---|---|---|---|---|
| Alumina (Al₂O₃) | 3.9–4.0 | 1,700 | 15–25 | Low |
| Zirconia (ZrO₂) | 6.0–6.1 | 2,400 | 10–12 | Medium |
| Silicon Nitride (Si₃N₄) | 3.2–3.3 | 1,400 | 12–15 | High |
| Aluminum Nitride (AlN) | 3.3 | 1,800 | 14–16 | High |
| Bioceramics (HA/TCP) | 3.0–3.2 | 1,200 | 8–10 | Very High |
5. Customization and Surface Finishing Options
Post-sintering processes transform ceramic injection molded components from dimensionally stable blanks into application-ready parts. Precision grinding, metallization, laser marking and functional coatings each address specific end-use demands — from sub-micron flatness for sealing surfaces to bioactive layers for implants — while adding 1–3 weeks and 15–40 % to unit cost.
Precision Grinding and Lapping
Grinding recovers dimensional accuracy after sintering shrinkage, achieving flatness within +/-0.005 mm and surface finishes down to Ra 0.2 µm. Centerless grinding suits cylindrical pins and ferrules; surface grinding refines seal faces and mounting planes.
Lapping with diamond slurry brings optical-grade flatness (< 0.001 mm) and Ra 0.05 µm for fiber-optic ferrules and high-vacuum seals. Expect 3–5 days added lead time and 20–30 % cost uplift for ground parts, 30–40 % for lapped.
Metallization for Electrical Contacts
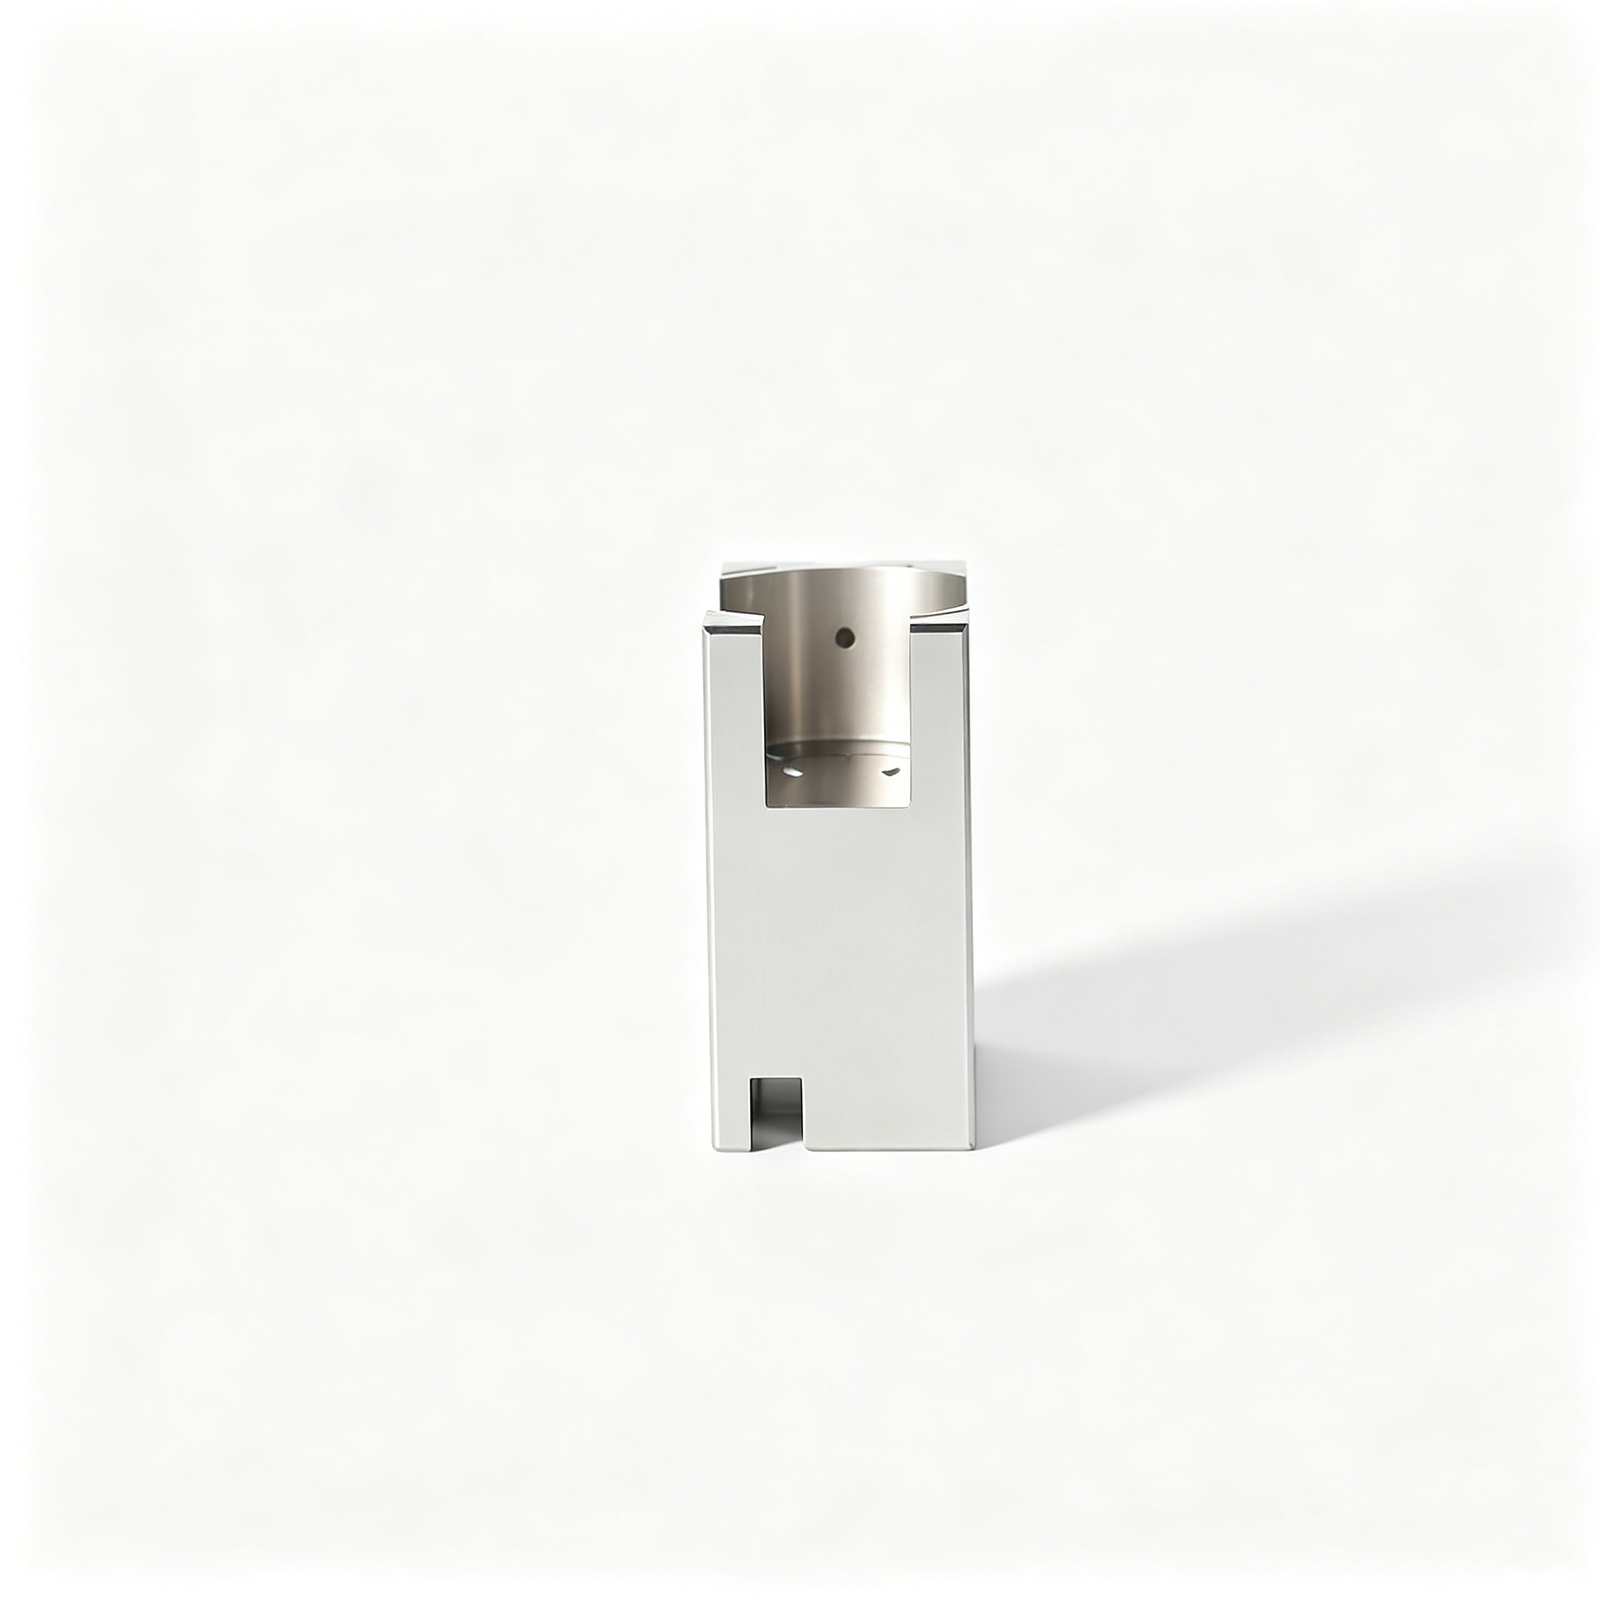
Plating (electroless nickel, gold) or PVD sputtering deposits conductive layers on insulating ceramics for sensor housings, RF shields and semiconductor chucks. Typical thickness is 1–5 µm nickel base plus 0.5–1 µm gold flash.
Metallization adds 5–7 days and 25–35 % cost. Mask design and adhesion testing are critical; poor pre-clean causes delamination in thermal cycling.
Laser Marking and Traceability
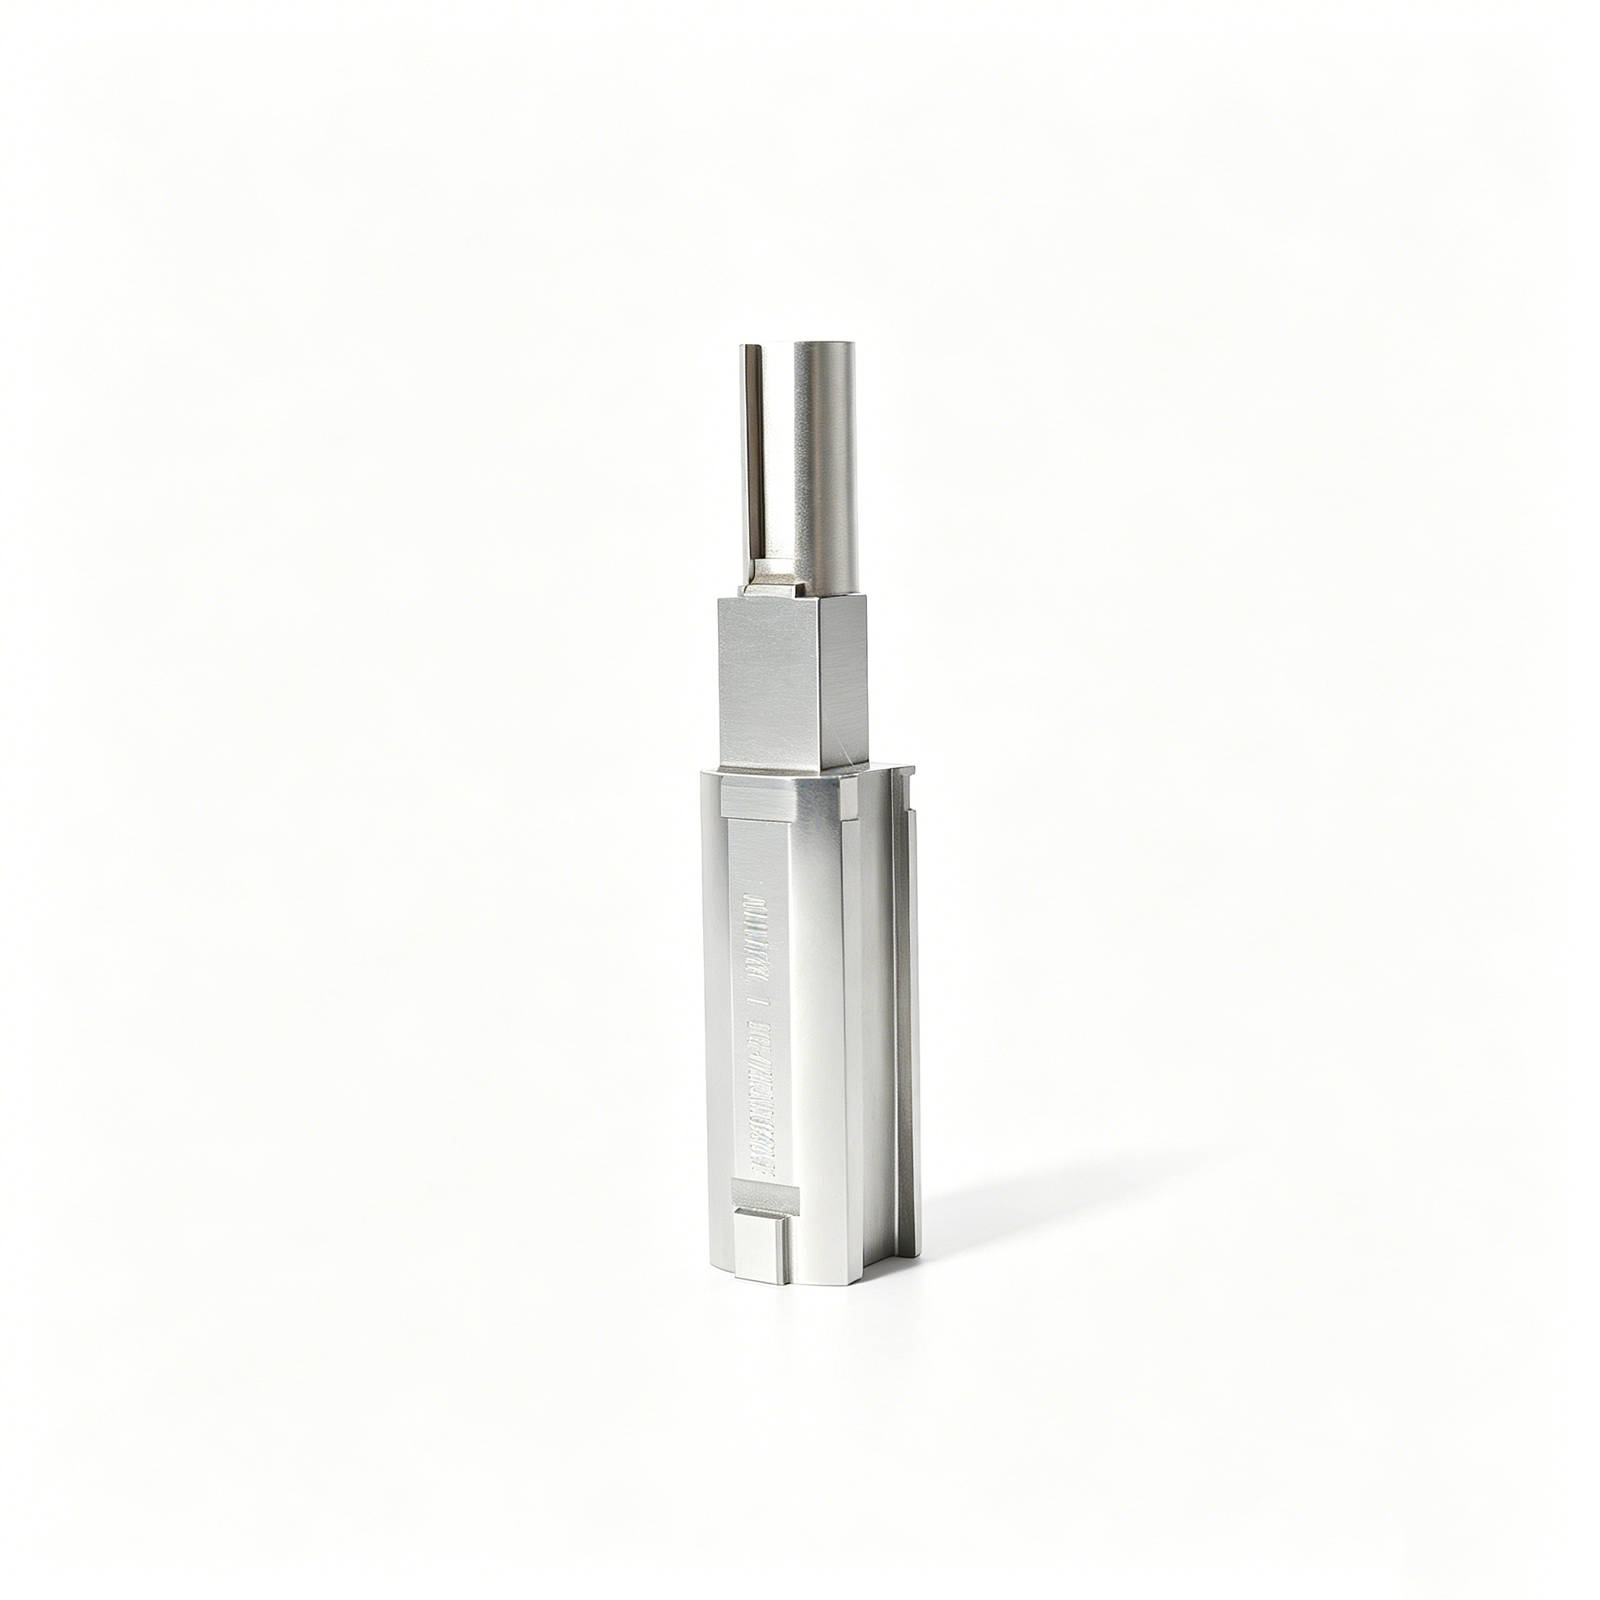
Fiber or CO₂ lasers etch alphanumeric codes, 2D DataMatrix or logos without consumables or masks. Mark depth is 10–50 µm; resolution supports 0.3 mm character height for medical and aerospace traceability.
Laser marking adds 1–2 days and 5–10 % per part. It is permanent, autoclave-safe and preferred over pad printing for high-mix, low-volume batches.
Surface Coatings
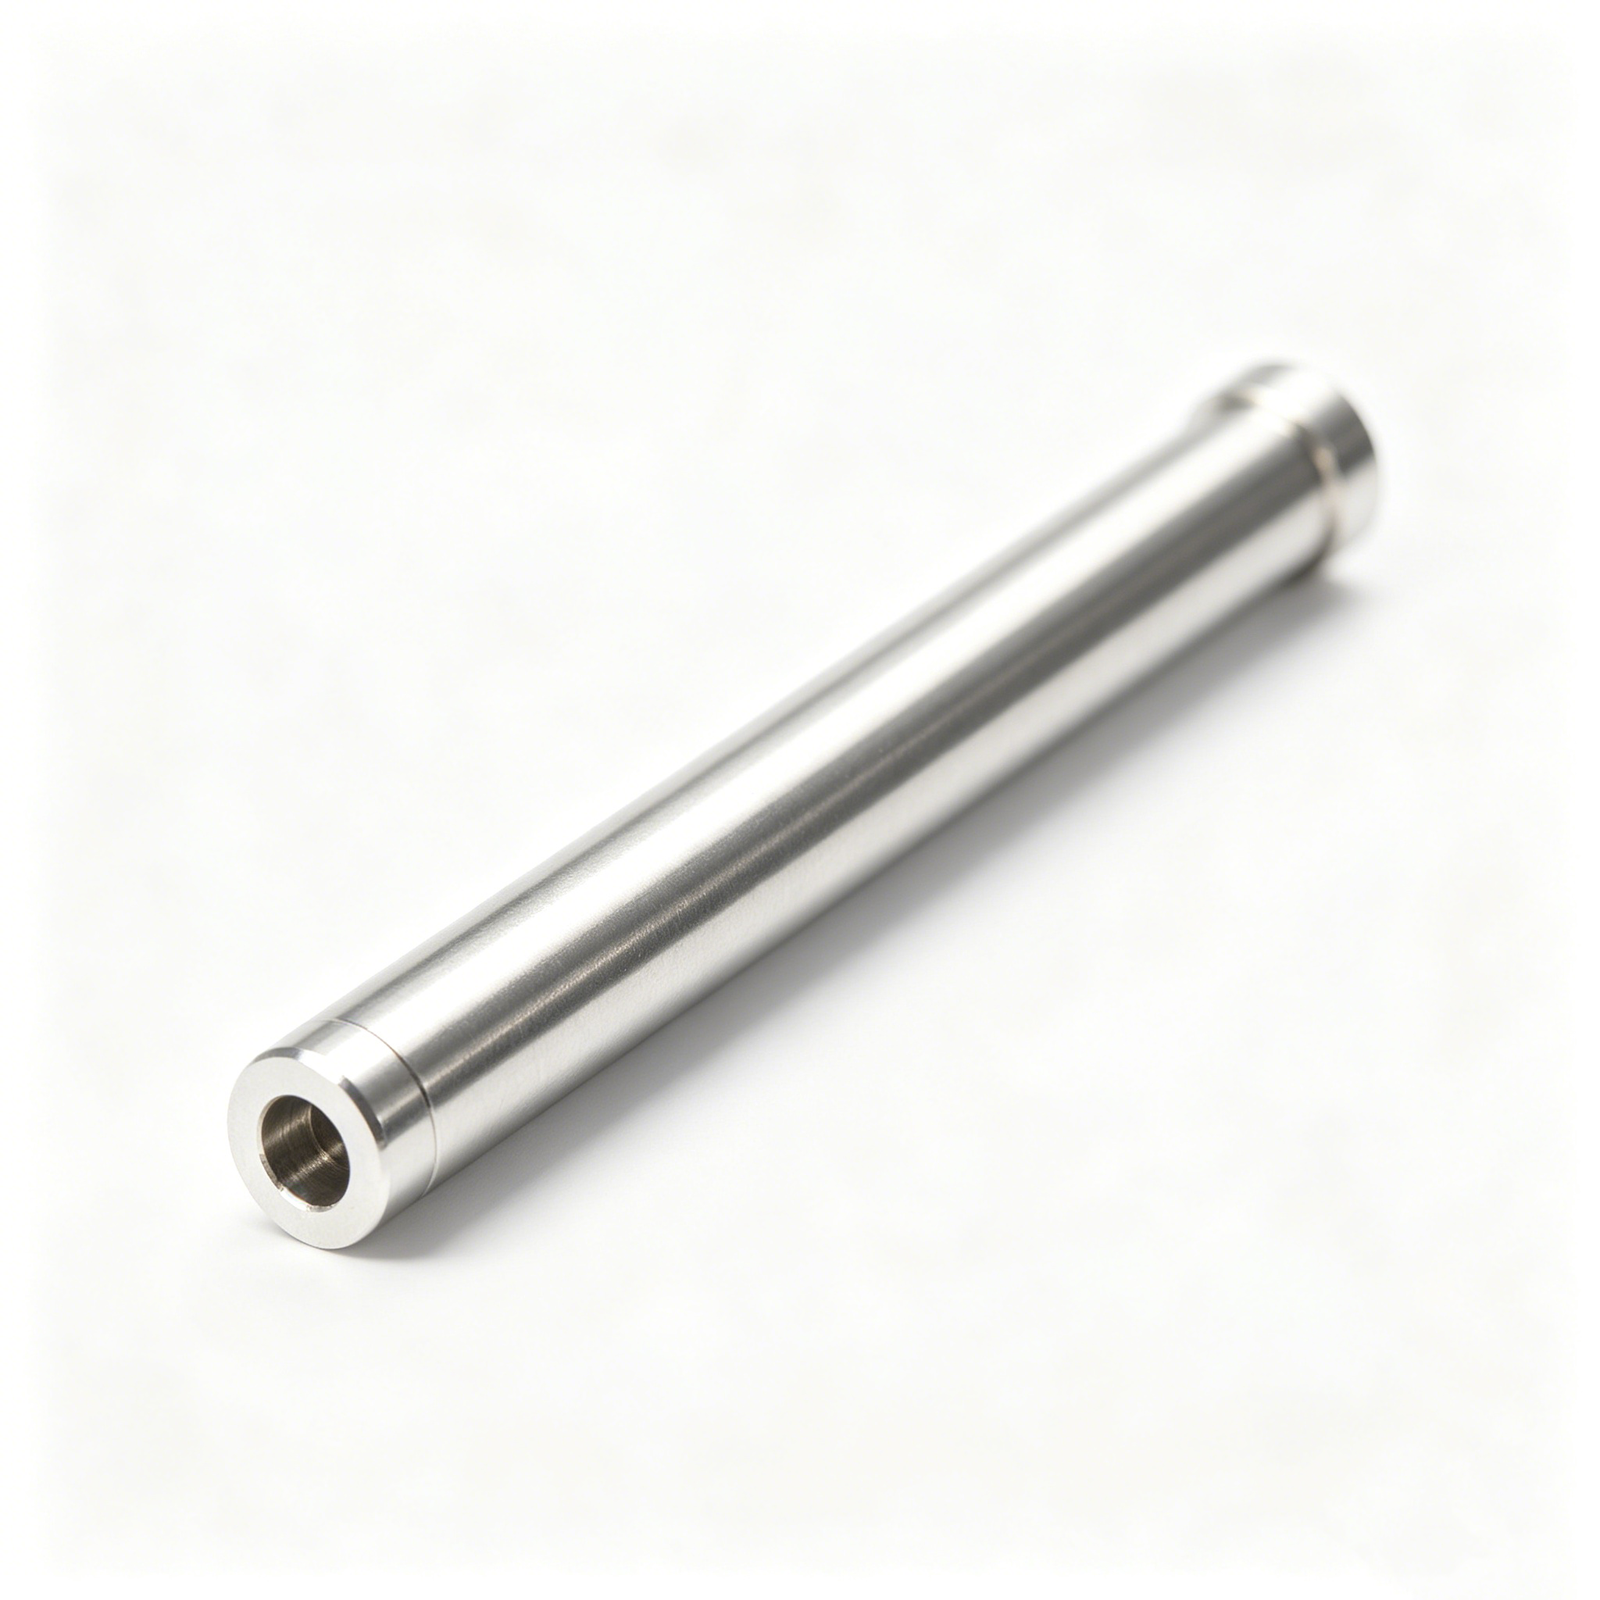
Bioactive coatings (hydroxyapatite, calcium phosphate) promote osseointegration on dental and orthopedic implants. Wear-resistant coatings (TiN, DLC) extend life in sliding contacts and cutting tools.
Coating adds 7–10 days and 15–25 % cost. Specification must include thickness, adhesion test method (scratch, pull-off) and biocompatibility certificates (ISO 10993) for medical applications.
6. Key Quality and Performance Criteria
Ceramic injection molded components must meet measurable quality benchmarks across dimensional, mechanical and material properties. Buyers in medical, automotive and 5G markets rely on ISO and ASTM testing to validate parts before production scale-up.
Dimensional Tolerance and Surface Finish
Grinding recovers dimensional accuracy after sintering shrinkage, achieving flatness within +/-0.005 mm and surface finishes down to Ra 0.2 µm. Centerless grinding suits cylindrical pins and ferrules; surface grinding refines seal faces and mounting planes. Lapping with diamond slurry brings optical-grade flatness and Ra 0.05 µm for fiber-optic ferrules and high-vacuum seals. Expect 3–5 days added lead time and 20–30% cost uplift for ground parts, 30–40% for lapped.
Density and Mechanical Strength
Sintered density above 98% of theoretical maximum eliminates porosity that causes premature failure. ISO 6872 flexural strength (≥300 MPa for alumina) and compressive strength (≥2,000 MPa) are baseline requirements for load-bearing applications in robotics and automotive.
Thermal and Electrical Properties
Dielectric strength (≥10 kV/mm) and thermal conductivity (20–35 W/m·K for AlN substrates) govern performance in power electronics and RF modules. ASTM C1161 and IEC 60672 certification is mandatory for medical-device and automotive Tier 1 supply chains.
7. How to Choose a Ceramic Injection Molded Components Manufacturer
Selecting a ceramic injection molded components supplier requires a systematic evaluation of technical capability, quality systems and operational responsiveness. A disciplined framework protects against tolerance drift, delivery delays and hidden costs downstream.
Production Capacity and MOQ Flexibility
Confirm annual throughput, machine count and batch-size range. Suppliers running multi-cavity tooling on 50–200 ton presses typically offer MOQs from 1,000 to 10,000 pieces; pilot runs may start at 100–500 units. Ask for capacity utilization and lead-time guarantees at your target volume.
In-House Tooling and Mold-Making Capability
Verify whether the supplier owns CNC machining, EDM and CMM inspection assets. In-house tooling shortens iteration cycles by 20–40 % and ensures tighter tolerances. Request equipment lists—look for Sodick, Charmilles or Seibu slow-wire EDM and ZEISS or Mitutoyo CMM platforms.
Quality Certifications and Audits
ISO 9001:2015 is baseline; automotive projects require IATF 16949, medical devices need ISO 13485. Request certificates, scope statements and last audit date. Schedule a facility visit or third-party process audit to validate metrology, material traceability and statistical process control.
8. Common Mistakes When Sourcing Ceramic Injection Molded Components
Even experienced procurement teams stumble when sourcing ceramic injection molded components, often underestimating the interplay of material science, tooling precision and process control. Five recurring mistakes drive most tolerance failures, delivery delays and cost overruns.
Underestimating Shrinkage Compensation in Mold Design
Ceramic parts shrink 15–25% during sintering, yet many buyers approve mold designs without verifying that the toolmaker has applied the correct shrinkage factor for the chosen ceramic feedstock and sintering profile. A zirconia component targeting ±0.02 mm final tolerance requires mold dimensions calculated to ±0.003 mm or tighter.
Request DFM documentation that specifies shrinkage coefficients by axis and confirms CMM capability (e.g., ZEISS MICURA class) for pre-sintering validation.
Ignoring Binder Removal and Sintering Profiles
Binder debind and sintering are not ‘black-box’ steps. Rushed thermal cycles cause warping, cracking or incomplete densification. Buyers who skip process-parameter review often receive parts that pass visual inspection but fail under mechanical or thermal load.
Ask for time-temperature curves, ramp rates and hold times; reputable manufacturers document every stage and link profiles to material certificates.
Choosing Material Solely on Cost
Selecting alumina over zirconia to save 20% on unit price is false economy if your application demands fracture toughness above 4 MPa·m½. Without verified datasheets—hardness, flexural strength, dielectric constant—you risk field failures.
Demand third-party test reports and cross-check against ISO or ASTM standards before finalizing material selection.
9. Steps to Launch Your Ceramic Component Project
Launching a ceramic injection molded components project requires a structured, phased workflow to mitigate tolerance risk and compress time to market. XUXIANG’s engineering-led approach divides the process into six gates, each with clear deliverables and timeline expectations.
Feasibility and Material Selection
Binder debind and sintering are not black-box steps. Rushed thermal cycles cause warping, cracking or incomplete densification. Buyers who skip process-parameter review often receive parts that pass visual inspection but fail under mechanical or thermal load. Ask for time-temperature curves, ramp rates and hold times; reputable manufacturers document every stage and link profiles to material certificates.
DFM Consultation and Mold Design
A 10+ engineer DFM team flags wall-thickness variations, draft angles and gate placement to prevent warpage. Mold design, simulation and approval typically span 1–2 weeks; ZEISS MICURA validation confirms +/-0.001 mm tooling accuracy before steel cut.
T1 Sampling and Dimensional Inspection
First articles undergo five-step QC: spectral analysis, in-process monitoring, CMM verification to 0.7 µm, surface integrity and FAI documentation. T1 cycles average 2–3 weeks; dimensional reports accompany every sample shipment.
Pilot Run and Performance Testing
Pilot batches (50–500 units) validate process repeatability and material certificates. Customers conduct thermal cycling, hermeticity or dielectric testing; feedback loops close within 3–5 days to adjust sintering profiles or surface finishes.
Transition to Volume Production
ISO 9001:2015 process control locks in validated parameters. The Quanzhou expansion adds 1,400 m² and targets 200 % annual output growth, enabling delivery roughly 30 % faster than industry average with full supply-chain integration and kanban replenishment.
10. Pricing and Cost Considerations
Tooling investment typically represents 40–60% of total project cost for runs below 1,000 units, with precision molds ranging from $8,000 to $25,000 depending on cavity count, feature complexity and tolerance class. Material and binder systems add $0.80–$3.50 per part, while debinding and sintering cycles — often 48–72 hours combined — contribute significant energy and labor overhead that scales favorably only above 500-unit batches.
Secondary operations (grinding, lapping, metallization) and CMM inspection can add 15–30% to unit cost on low volumes but drop to 5–10% beyond 5,000 pieces as setup is amortized. Negotiate tooling amortization across multiple purchase orders when annual demand exceeds 10,000 units; many suppliers will spread mold cost over 24 months in exchange for volume commitment, reducing effective per-unit burden by 20–35%.
| Quantity Tier | Unit Price Range (USD) | Tooling Amortized | Typical Lead Time |
|---|---|---|---|
| 100 | $18–$45 | Full upfront | 8–10 weeks |
| 500 | $12–$28 | Partial (20–40%) | 6–8 weeks |
| 1,000 | $8–$18 | Partial (50–70%) | 5–7 weeks |
| 5,000+ | $4–$10 | Fully amortized | 4–6 weeks |
Ready to Source Precision Ceramic Injection Molded Components?
Get your quote in 24 hours, samples in 3-7 days, and full DFM engineering support from 10+ precision experts.