
Wire EDM, sinker EDM and precision grinding solve different geometry problems. Wire EDM cuts a through profile in electrically conductive material with a moving wire electrode. Sinker EDM uses a shaped electrode to create blind cavities and three-dimensional negative geometry. Grinding removes material with an abrasive wheel and is often selected for accessible planes, diameters and profiles where size, form and surface control are required. A mold component may use all three in sequence.
This guide supports the XUXIANG wire EDM machining capability and helps buyers describe geometry, material condition, datum, tolerance, surface and inspection instead of choosing a process by name alone.
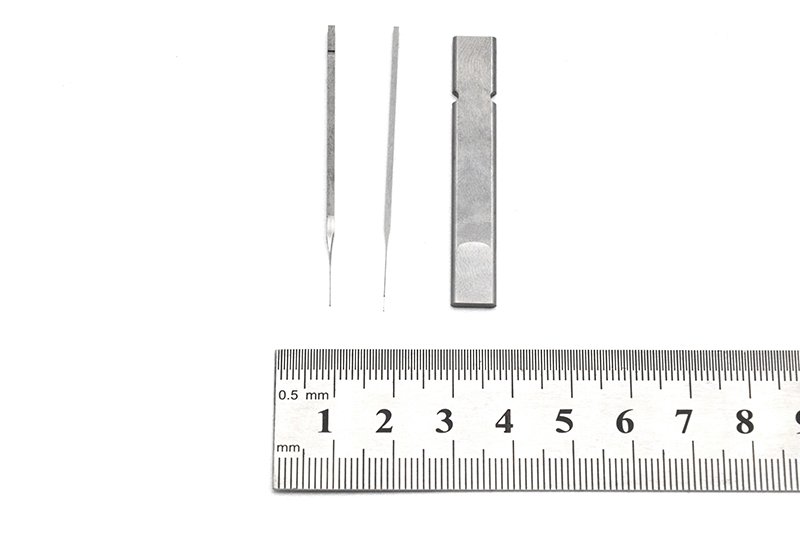
Quick Process Comparison
| Requirement | Wire EDM | Sinker EDM | Precision grinding |
|---|---|---|---|
| Typical access | Through-cut path | Blind cavity or internal form | Wheel-accessible surface/profile |
| Tool | Continuously fed wire | Shaped electrode | Abrasive wheel |
| Material | Electrically conductive | Electrically conductive | Broad range, process-specific |
| Mechanical cutting force | Very low | Very low | Present and controlled |
| Key planning issue | Start hole, wire path, taper and slug | Electrode design, wear and flushing | Wheel access, workholding, heat and dressing |
| Common evidence | Profile report, form/position, surface | Cavity geometry, electrode record, surface | Size, flatness/roundness, finish and burn control |
The table is directional. Machine, control, tooling, material, part size and inspection capability determine achievable results. Require a drawing review before accepting any tolerance claim.
Choose Wire EDM for Through Geometry
Wire EDM is effective for punches, die inserts, slots, contours and profiles that the wire can traverse. It can process hardened conductive materials without conventional cutting force, which helps with slender or already heat-treated parts.
The designer must provide a continuous path or identify start holes. Internal corners remain influenced by wire diameter, spark gap and finishing strategy; an impossible sharp corner should be revised or produced by another method. If a slug can fall or move, plan retention and removal so it does not damage the part.
Specify taper, land, relief and cut direction on die components. A two-dimensional DXF alone may not communicate thickness-dependent geometry or datums. Identify which face establishes orientation and where the profile must be measured.
Choose Sinker EDM for Blind Cavities
Sinker EDM reproduces an electrode shape into conductive material. It is suited to blind ribs, pockets, logos, textured cavities and internal forms that a travelling wire cannot reach. The electrode, orbit strategy, wear compensation and flushing become part of the process plan.
Electrode design affects cost and lead time. Complex cavities may require roughing and finishing electrodes or multiple orientations. Ask the supplier to identify electrode material, quantity and whether tooling is retained for reorders.
Deep narrow features need review for flushing, debris removal and stable discharge. Do not specify geometry that traps the electrode or makes inspection impossible without discussing section access, draft and radii.
Choose Grinding for Accessible Precision Surfaces
Surface, cylindrical, jig and profile grinding cover different applications. Grinding is commonly used for plates, rails, punches, pins and shutoff or reference surfaces where direct abrasive access is available. It can establish size and finish after heat treatment.
Workholding and wheel access are critical. Thin parts may distort under magnetic or mechanical holding; intermittent contact and small radii require suitable wheel selection and dressing. Grinding heat can alter the surface if parameters, coolant and wheel condition are poorly controlled.
Define whether the requirement is size, flatness, parallelism, roundness, cylindricity, profile or surface texture. “Precision ground” is not an acceptance criterion.
Process Sequence Matters
A typical component may be rough machined, heat treated, ground on datums and then wire-cut or sinker-EDMed. Another part may be EDM-produced and lightly ground where accessible. The sequence affects distortion, remaining stock and the datums available to locate later operations.
Ask the manufacturer to submit a process route for critical parts. Confirm when heat treatment occurs and how distortion allowance is managed. If a final EDM operation references a ground face, that relationship belongs on the drawing and inspection plan.
Material and Heat Treatment
Provide material standard, grade, condition, hardness requirement and any approved substitute policy. EDM requires electrical conductivity; grinding behavior depends on hardness, toughness, carbides and thermal response.
Do not accept a hardness value without location and test method. Surface treatment, nitriding or coating may require stock allowance or masking. If material certificates or heat-treatment records are required, state them in the RFQ.
Surface Integrity, Recast and Grinding Burn
EDM removes material through controlled electrical discharges and can leave a thermally affected surface layer. Roughing and finishing passes influence texture and surface condition. Critical fatigue, sliding or sealing applications may require an agreed finish strategy and additional finishing.
Grinding can create thermal damage or residual stress when heat is not controlled. Visual appearance alone may not reveal it. Define any required burn inspection or metallurgical verification based on application risk; do not add expensive tests without an engineering basis.
Mitsubishi Electric and Makino publish process information that distinguishes wire and sinker EDM applications. See Mitsubishi Electric EDM and Makino EDM technologies.
Translate Function Into Drawing Requirements
Identify functional interfaces first: shutoff, sliding fit, locating diameter, cutting edge, sealing plane or cavity surface. Apply tolerances only where function requires them. Excessively tight global tolerances increase finishing and inspection cost without improving the tool.
Use a datum system that the supplier can manufacture and inspect. State profile and position requirements, corner radii, relief, surface texture and edge condition. Distinguish theoretical sharp corners from permissible radii.
For matched components, define clearance and which member controls it. Do not rely on two independent nominal dimensions whose accumulated tolerances defeat the fit.
RFQ Package
Include:
- controlled 2D drawing and 3D model;
- material, condition and heat treatment;
- quantity and reorder expectation;
- datum scheme and critical characteristics;
- through/blind feature identification;
- surface texture and surface-integrity requirements;
- edge break, burr and corner rules;
- inspection method and report format;
- certificate and traceability requirements;
- mating-part or assembly information;
- allowed process alternatives and approval route.
Ask the supplier to flag inaccessible features and measurement uncertainty before quoting.
Inspection Planning
Select instruments by characteristic. CMM or vision systems may verify profiles and positions; micrometers, height gauges, roundness equipment or surface instruments address other features. Very small radii and deep cavities may require specialized access.
Agree how the part is fixtured, which datum is established first and how temperature is controlled for critical measurements. A report should show nominal, tolerance, actual result, instrument or method and part identity.
First-article inspection is valuable when tooling or process is new. Retain the approved program and datum setup for reorders.
Bulk and Reorder Controls
Monitor electrode wear for sinker EDM, wire condition and process stability for wire EDM, and wheel dressing and thermal control for grinding. Inspect at risk-based intervals rather than only after the batch is complete.
For reorders, confirm drawing revision, material lot, heat-treatment route, machine program, electrode revision and inspection setup. A similar-looking part can fail assembly if datum or clearance logic changes.
Quote Cost by Process Drivers
Wire EDM cost is affected by cut length, workpiece thickness, number of passes, start holes, threading events and required surface. Sinker EDM adds electrode design, manufacturing, wear and multiple burn stages. Grinding cost depends on stock removal, setup, wheel specification, dressing, access and inspection. Ask the supplier to separate one-time engineering or electrode cost from repeat unit cost.
A cheaper route is not economical if it leaves inaccessible stock, requires manual polishing that changes form, or cannot be inspected reliably. Request alternative process routes when the drawing permits them, and require the supplier to state the dimensional or surface tradeoff. This makes value engineering reviewable instead of allowing an undocumented substitution after order placement.
Protect Critical Edges During Handling
Finished punches, inserts and shutoff edges can be damaged after machining. Define temporary edge protection, rust prevention, cleaning and individual packing. Inspection should occur before protective coating and be confirmed after packing when contact damage is a risk.
Mark parts and revisions without placing identification on functional surfaces. For matched sets, keep component pairing traceable through inspection and shipment. Receiving inspection should verify packaging condition, identity and critical dimensions before the parts enter tool assembly.
Frequently Asked Questions
Can wire EDM make a blind pocket?
Not in the way sinker EDM does; the wire needs a through cutting path. Some geometry may be redesigned or combined with another process.
Is EDM always more accurate than grinding?
No. Accuracy depends on feature, machine, setup, material, process and inspection. Grinding may be the stronger choice for accessible surfaces; EDM may enable geometry grinding cannot reach.
Does EDM eliminate burrs and distortion?
It minimizes conventional cutting force, but surface integrity, slug handling, heat-treatment distortion and edge condition still require control.
What should a buyer ask before choosing?
Ask which process best creates the functional geometry, what datums and stock are needed, how surface integrity is managed and how every critical feature will be measured.
The Practical Decision
Use wire EDM for conductive through profiles, sinker EDM for blind negative geometry, and grinding for wheel-accessible precision surfaces and forms. Combine them when the part requires multiple functions.
Approve the process route from drawing and inspection evidence, not a generic tolerance advertisement.
Sources
- Mitsubishi Electric EDM Systems — wire and sinker EDM technology context.
- Makino EDM Machines and Technology — manufacturer process resources.
- NIST Dimensional Metrology — measurement traceability context.









