A first article inspection report for a precision mold component should connect every inspected characteristic to the released drawing, the exact manufactured specimen and a suitable measurement method. It is not merely a table of dimensions. A useful FAI shows what changed, what was verified, what could not be verified and who authorized release.
Use the workflow with the XUXIANG quality and certification system before repeat production. The report supports process validation; it does not replace ongoing in-process control or final inspection.
Define the Trigger and Scope
Run a first article inspection for a new part or when a change can affect conformity. Triggers may include drawing revision, material source, manufacturing location, CNC program, tooling, heat treatment, coating, special process, long production gap or corrective action.
The customer and supplier should agree scope before machining. A full FAI verifies all drawing characteristics and applicable notes. A partial or delta FAI verifies affected characteristics, but its link to the original approved baseline must be clear.
Do not call a partial dimensional check a complete FAI. State exclusions and reasons explicitly.
Freeze the Technical Baseline
Record customer, part number, part name, drawing number and revision, model or CAD revision, purchase order, specification revisions and any approved deviation. Keep the exact released documents in the inspection package.
Balloon the drawing so every dimension, geometric tolerance, surface requirement, material note and special-process requirement receives a unique characteristic number. The result table should use the same numbers.
If the drawing and model conflict, stop and obtain disposition. Inspecting to whichever value is easier destroys traceability.
Identify the Physical Specimen
Mark or otherwise trace the first article to work order, machine, program version, cavity or setup, material heat or lot, operator and manufacturing date. For multi-cavity or family tooling, define which cavity is represented and whether all require verification.
The specimen should be produced using the intended production process, equipment and sequence. A hand-finished showpiece may prove geometry but not the repeatable process.
Photograph the part and identification. Protect critical surfaces and retain the specimen according to the agreed control plan.
Verify Material and Purchased Inputs
Check material grade, form, condition and certification against the drawing. Link the certificate to heat or lot identity. For standard mold parts, verify supplier reference and ordered specification.
Chemical composition or mechanical properties should be supported by appropriate certificates or test results. Do not copy values into the FAI without preserving the original evidence and scope.
If material identity cannot be traced to the inspected part, mark the item open. Dimensional conformity does not cure missing material evidence.
Map Each Characteristic to a Method
Choose equipment from tolerance, feature geometry, surface condition, accessibility and measurement uncertainty. Micrometers and calipers suit some direct dimensions; height gauges, bore gauges, optical systems, surface instruments and coordinate measuring machines suit others.
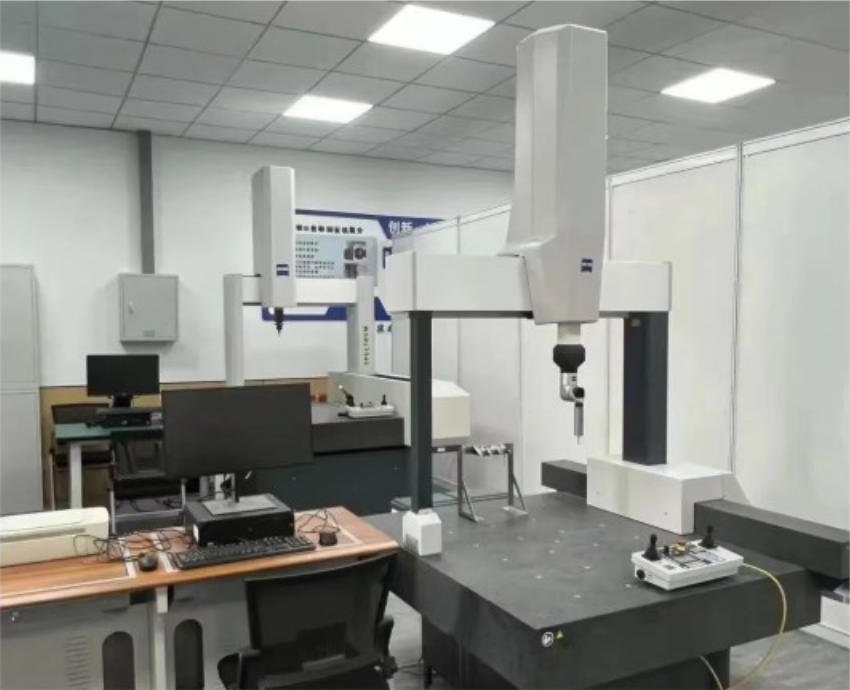
A CMM is powerful but not automatically correct. Fixture, datum alignment, probe selection, point strategy, filtering and software evaluation influence results. Preserve the program version and alignment definition.
NIST’s metrology resources explain measurement science and traceability context. The measurement result should be credible for the required tolerance, not merely generated by expensive equipment.
Establish Datum Alignment Correctly
Geometric tolerances depend on datum reference frames. Simulate datums as the drawing defines them and record setup. A part can show acceptable size yet fail position, profile, runout or orientation when aligned correctly.
Do not “best fit” a point cloud unless that evaluation is authorized by the drawing or inspection plan. Best fitting can distribute error and hide functional datum mismatch.
Photograph complex fixtures and note constrained degrees of freedom. Another qualified inspector should be able to reconstruct the method.
Report Actual Results
For variable characteristics, enter measured values and units, not only “pass.” For bilateral or unilateral tolerances, preserve the actual reading and limits. For attribute requirements, state the method and evidence.
Use enough decimal resolution for the decision without implying more certainty than the method provides. If multiple locations or a pattern are required, report the full set or attach the machine output.
Identify environmental conditions when they materially affect tight-tolerance measurement. Part and instrument temperature should be appropriately stabilized for the method.
Include Surface and Visual Requirements
Mold components may require roughness, polishing, texture, coating, edge break, burr removal, marking and cosmetic conditions. Translate notes into inspectable characteristics. Record instrument, comparator or visual standard used.
Texture and polished surfaces can affect later molding, release and appearance even when dimensions pass. Protect them during measurement. Do not place a rough fixture against a critical polished face.
Photographs support findings but should not replace required numerical roughness or coating evidence.
Verify Special Processes
Heat treatment, nitriding, plating, coating, welding, EDM recast removal and other processes may need approved sources, certificates and test coupons. Record process specification, supplier, batch and results such as hardness or thickness where required.
Inspect dimensions in the correct sequence. Heat treatment or coating can move size and geometry. A pre-process pass does not prove final conformity unless the drawing defines that state.
If a special-process report covers multiple parts, link the inspected specimen to its batch and quantity.
Handle Nonconformities Transparently
Record the actual result, characteristic number and disposition. Do not edit the drawing tolerance, round the measurement into range or rework the part without history. Identify whether remeasurement followed method correction or physical rework.
An approved deviation should reference the authorized document, quantity and expiry or scope. It does not permanently revise the design.
After correction, update the report so original failure, action and final verification remain visible. A clean final sheet with erased failures loses learning and authorization history.
Use AS9102 as a Structured Reference Where Applicable
SAE’s AS9102 standard page describes aerospace first article inspection requirements and standardized forms. A commercial mold project may not be contractually subject to AS9102, but its traceability principles are useful. Do not claim AS9102 compliance unless the contract, forms and process actually satisfy the applicable revision.
Customer-specific templates may require forms for part accountability, product accountability and characteristic accountability. Resolve format before inspection rather than remapping incomplete data at shipment.
FAI Package Checklist
| Section | Required connection |
|---|---|
| Part identity | Part, revision, order, work lot and specimen |
| Drawing | Balloon number to every characteristic |
| Material | Certificate to lot and inspected part |
| Processes | Supplier, specification, batch and result |
| Measurement | Method, equipment, calibration and actual value |
| Geometry | Datum setup and evaluation rule |
| Nonconformity | Actual result, action and authorization |
| Approval | Reviewer, date, scope and release status |
Review Calibration and Measurement Capability
List instrument identification and calibration status. Calibration should be traceable through the organization’s quality system and valid at use. Confirm equipment condition and any required pre-use checks.
For very tight tolerances, evaluate measurement uncertainty or conduct a capability study appropriate to risk. Repeating the same poor method does not make a result reliable.
If supplier and customer results disagree, compare datum simulation, temperature, force, probe strategy and software settings before assuming the part changed.
Move from FAI to Production Control
The approved FAI establishes a baseline. Convert critical and process-sensitive characteristics into in-process and final control plans with appropriate frequency. Monitor tool wear, thermal drift, EDM electrode life and setup changes.
Link production inspection to the same balloon scheme where practical. Trend actual values rather than waiting for an out-of-tolerance result. Retain samples and records according to contract and quality-system requirements.
Reopen the FAI assessment whenever change control indicates risk. A new purchase order alone does not always require full repetition, while a quiet process move may.
Frequently Asked Questions
What is included in a first article inspection report?
It typically includes part and revision identity, ballooned drawing, material and process evidence, actual inspection results, methods, nonconformities and authorized approval status. Contract requirements determine the exact format.
Does one passing part prove the process is capable?
No. It shows that an identified specimen was verified against the defined baseline. Process capability and continuing control require additional production data.
Must every drawing dimension be measured?
A full FAI normally accounts for every applicable characteristic and note. Any exclusion or partial scope must be agreed and linked to the prior baseline.
Can CMM output replace the report?
It can provide measurement evidence, but the package still needs part, drawing, material, process, characteristic and approval traceability. Raw output without mapping is incomplete.
Final Release Rule
Release only when each applicable balloon has a credible result or authorized disposition and all supporting material and process records trace to the inspected component. The approver should be able to move from any drawing requirement to method, actual value and evidence without inference. That is what turns an inspection table into a reliable first article baseline.
Sources
Where customer requirements permit, conduct an independent report review before shipment. The reviewer should follow a small set of balloon numbers from drawing to raw observation and material evidence, then confirm that every deviation has an active authorization. This catches mapping errors that a measurement operator may not notice while focusing on the component itself.