
Straight Ejector Pins — Micron-Stable Precision for High-Performance Molds
XUXIANG straight ejector pins deliver +/-0.001 mm machining accuracy, mirror-grade finishes and full FAI documentation — eliminating tolerance failure with quotes returned in 24 hours.
Featured Straight Ejector Pins
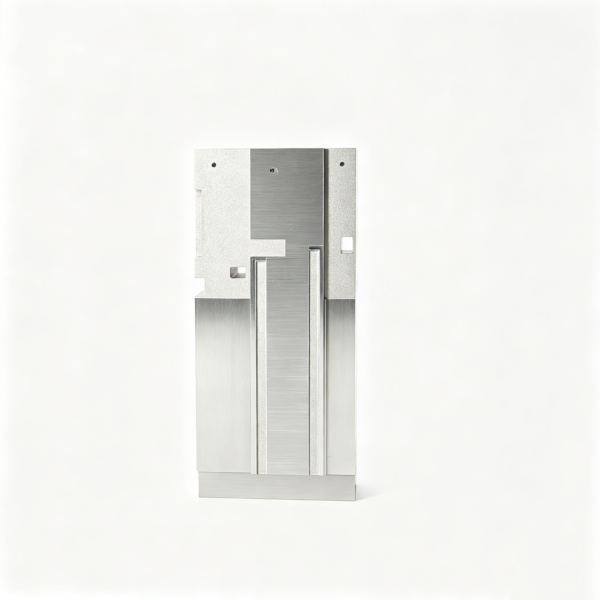
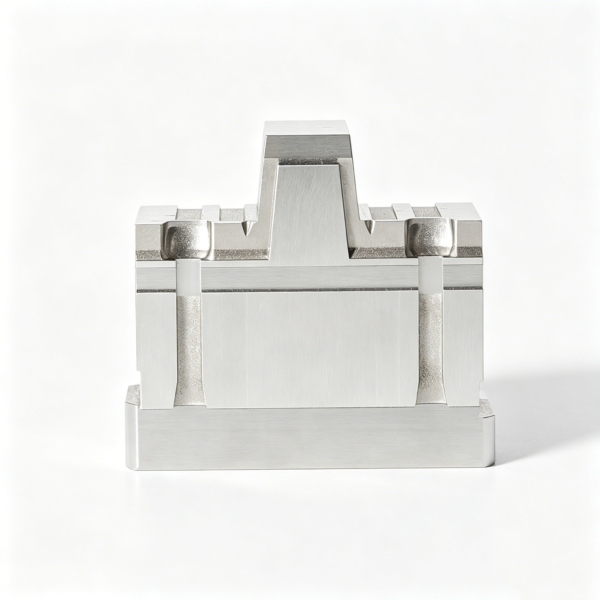
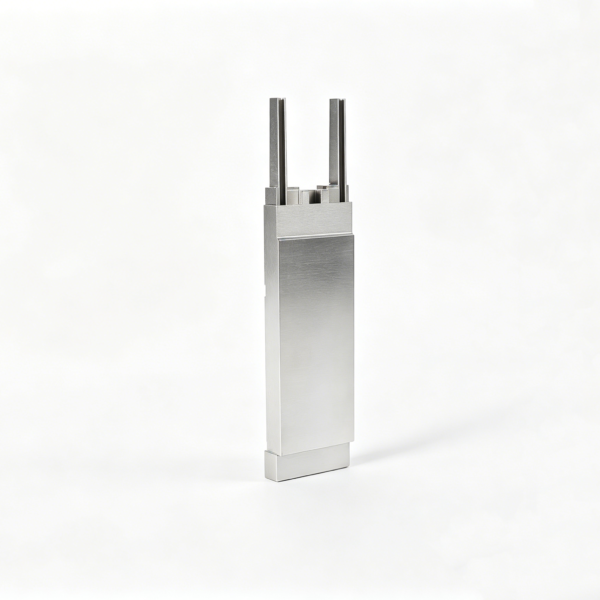
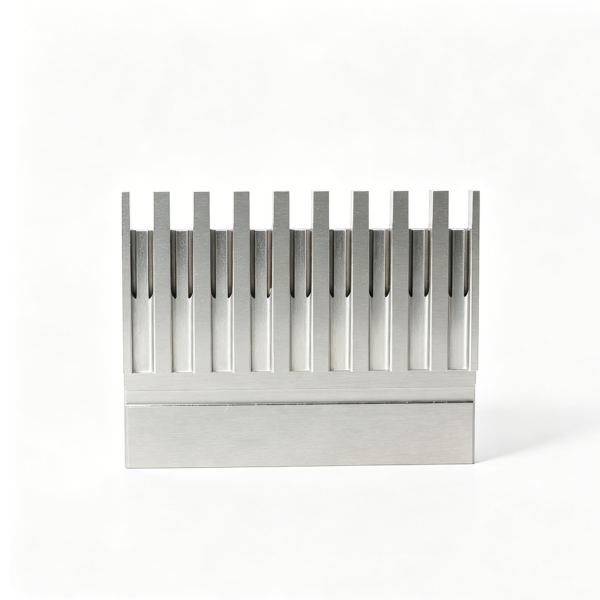
Straight Ejector Pin Gallery

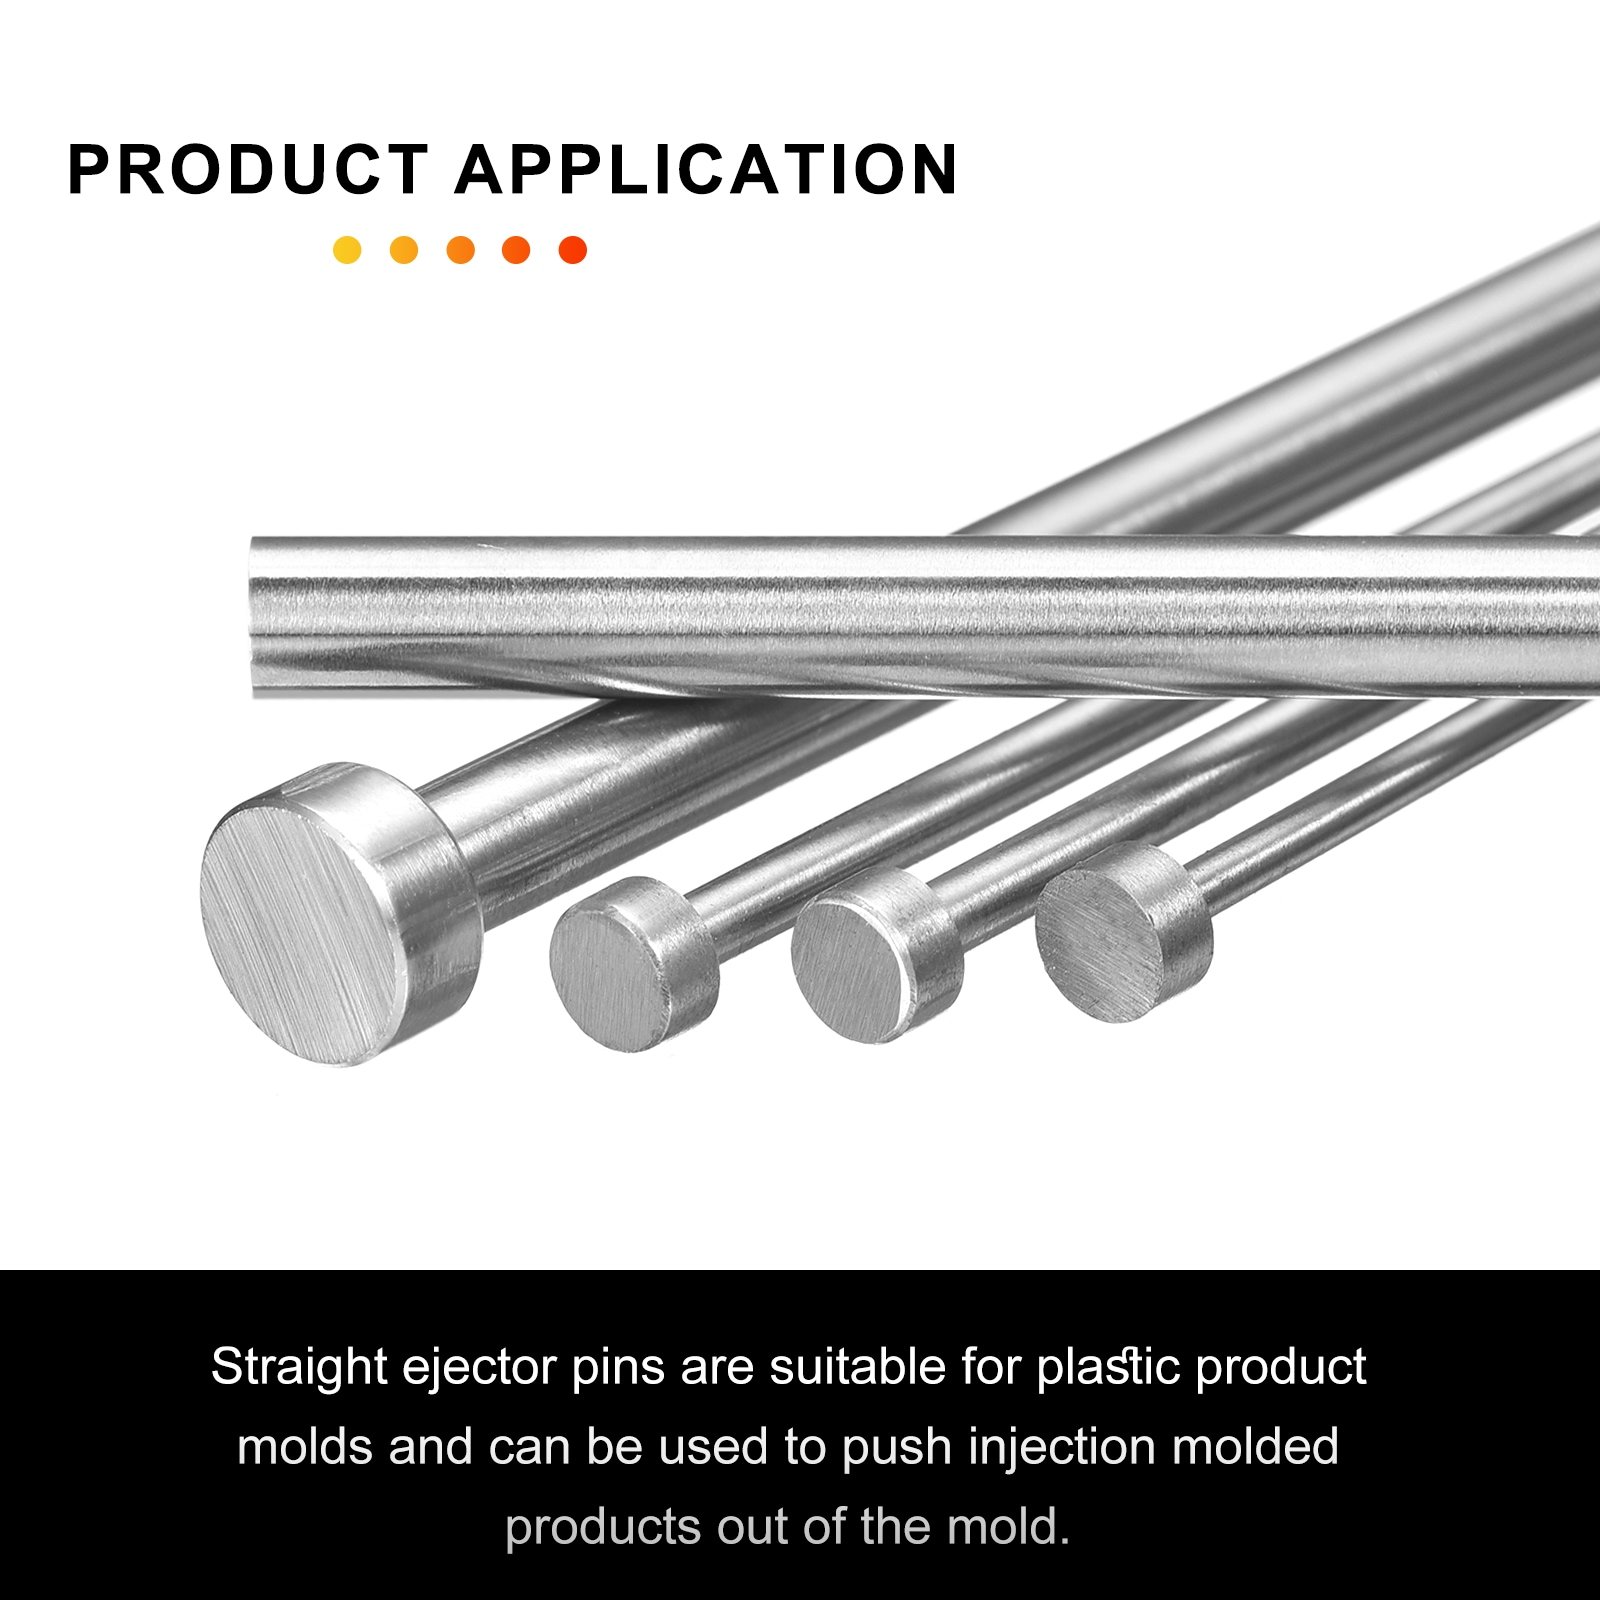
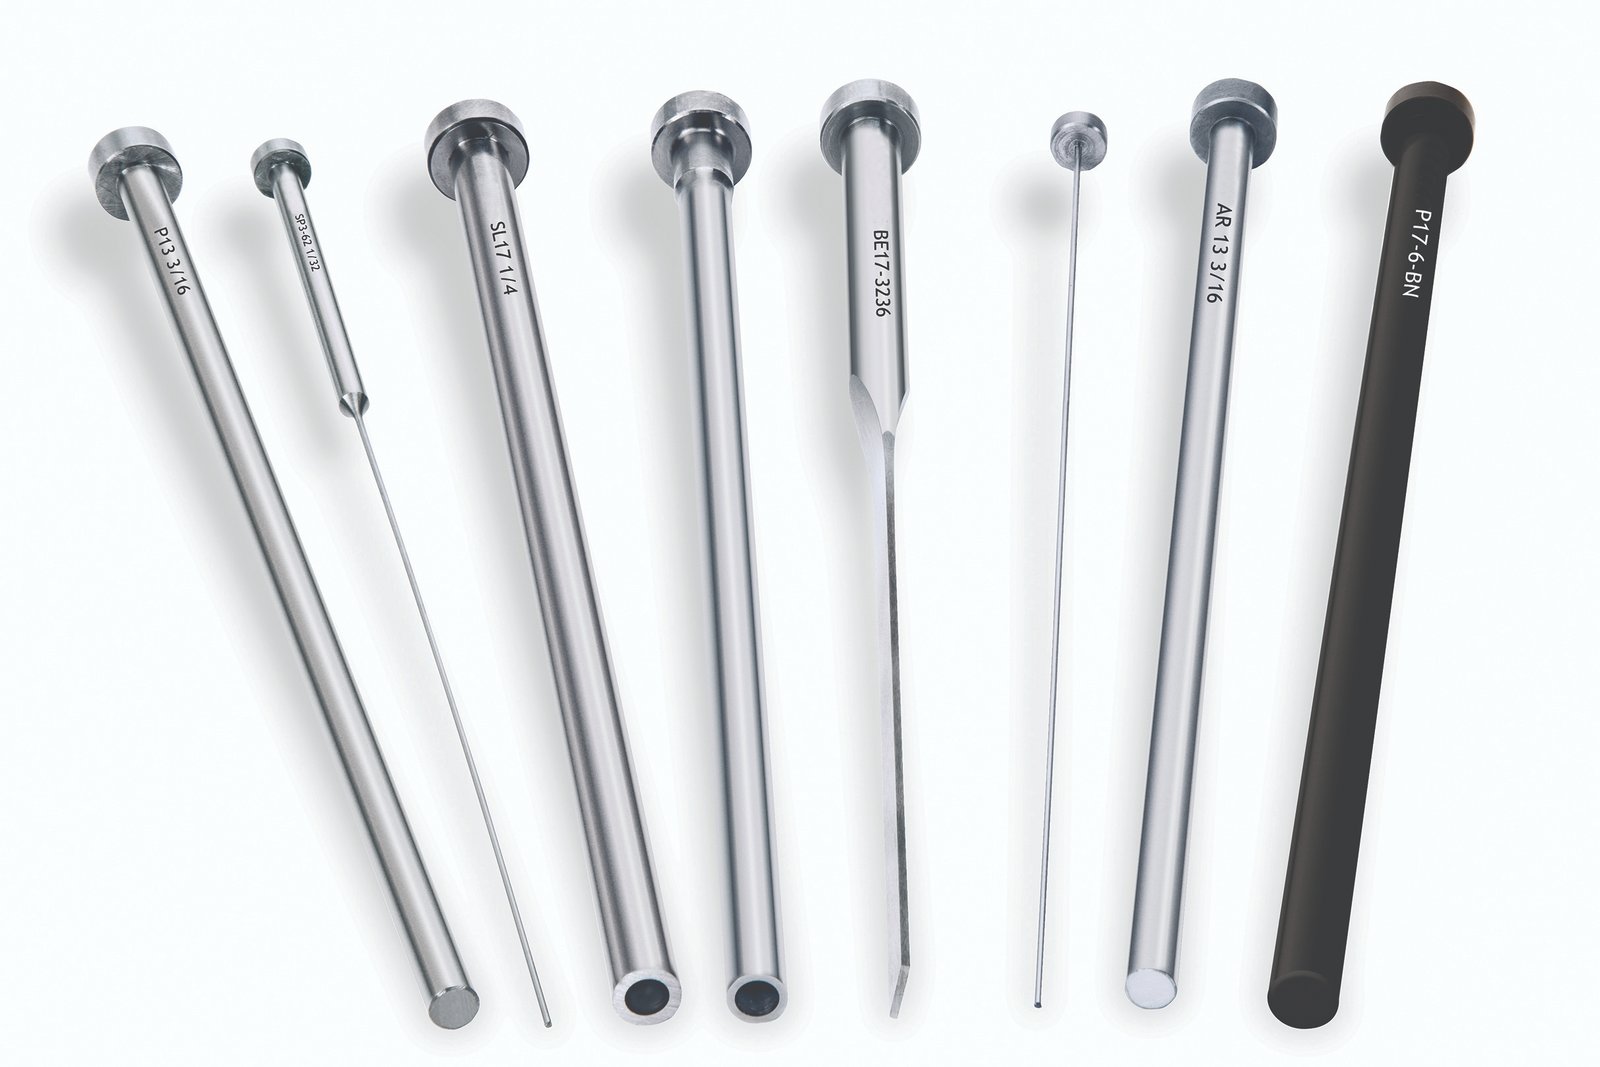
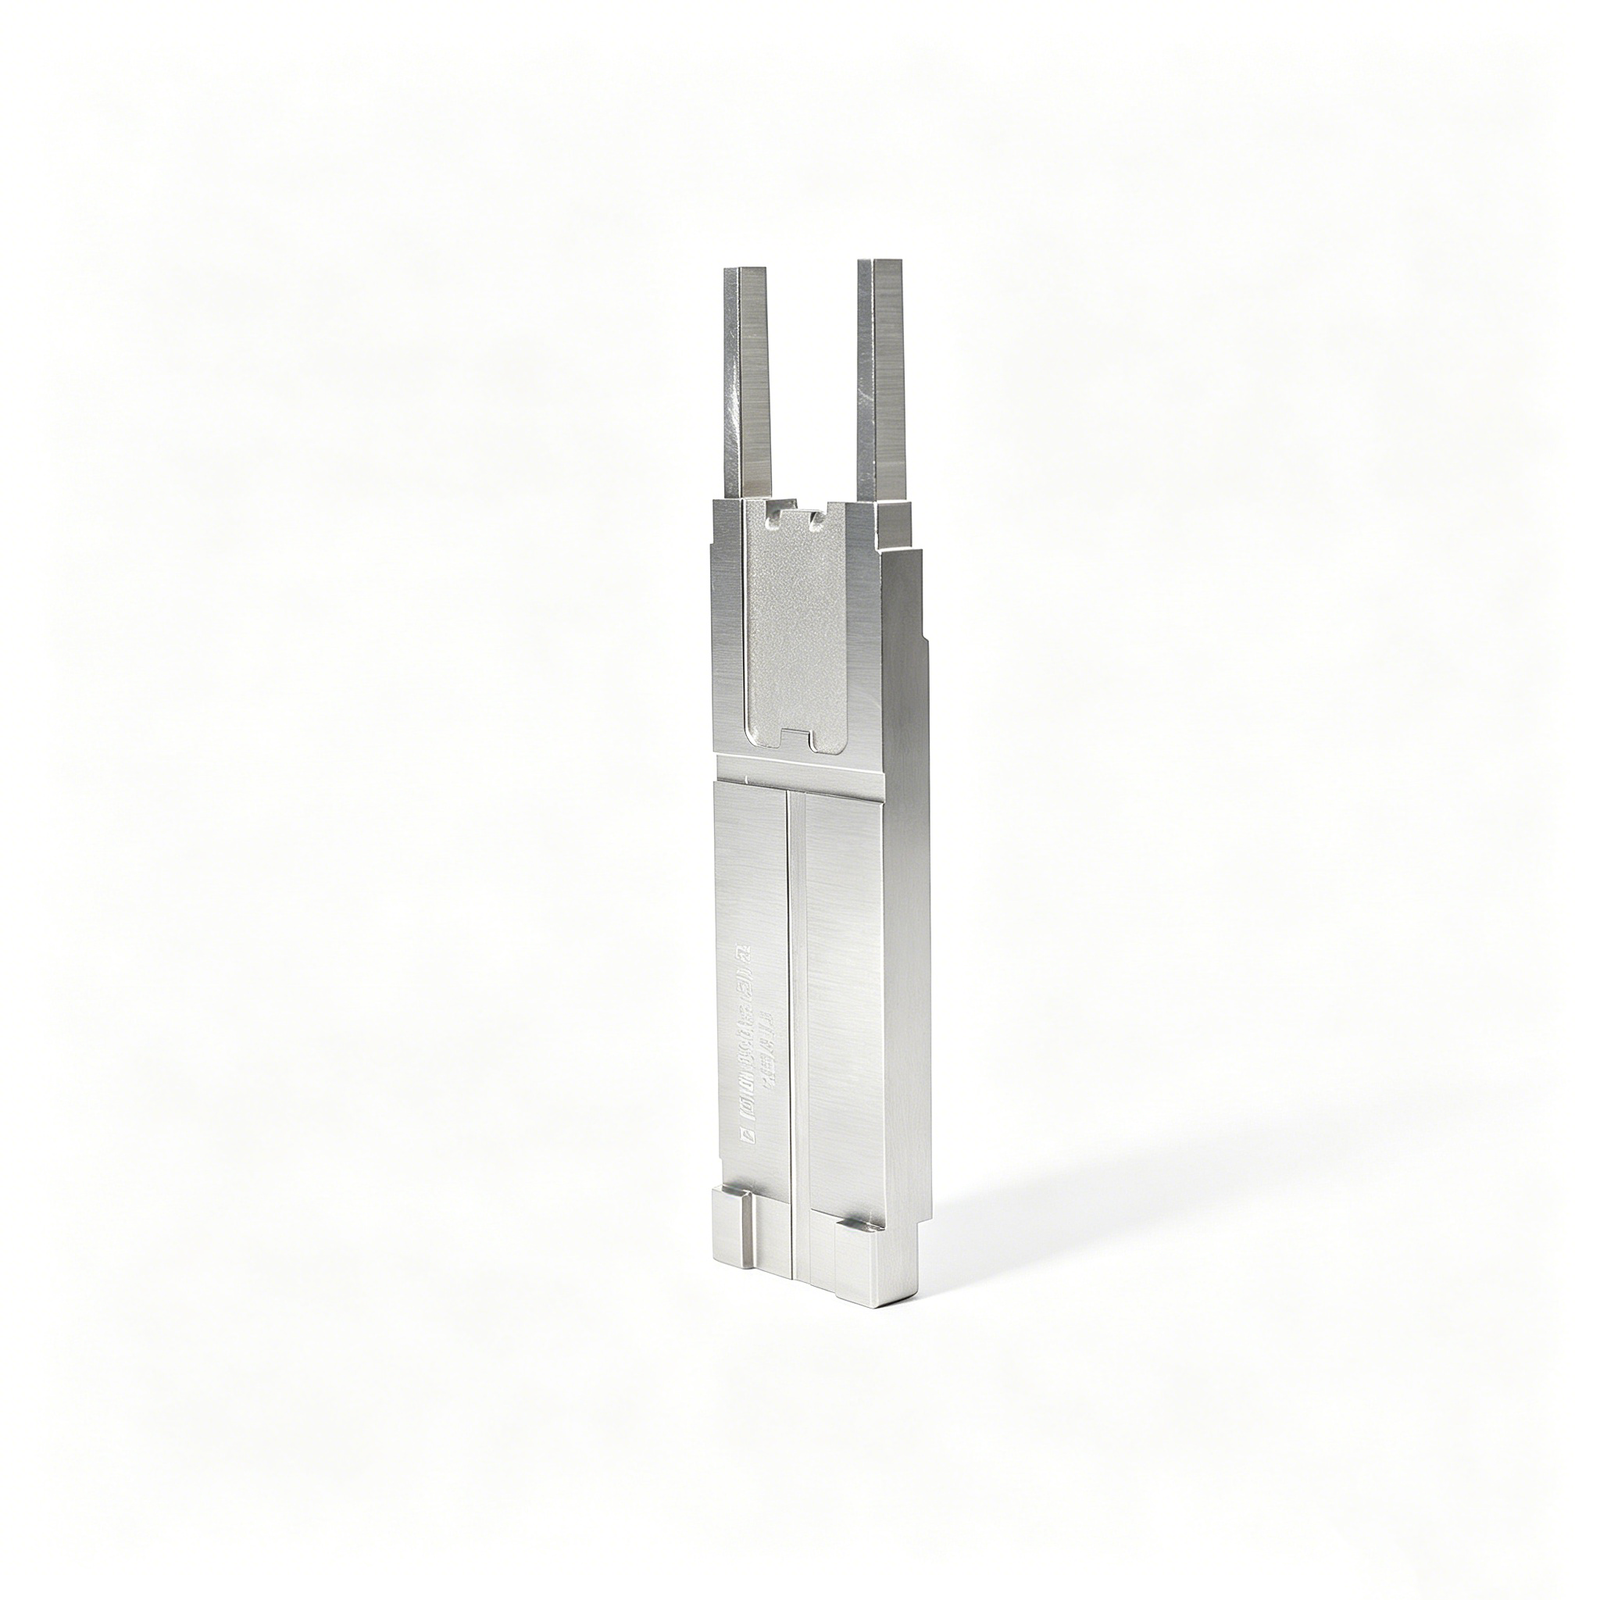
Straight Ejector Pins from XUXIANG: Six Engineering Advantages
Mirror-Grade EDM Finish
Ra 0.1um surface integrity eliminates micro-scratches and drag marks, ensuring clean part release and extended mold life in high-cycle production.
+/-0.001 mm Tolerance Hold
ZEISS MICURA CMM validation to 0.7um and Sodick slow-wire EDM deliver micron-stable dimensional consistency across every pin in your order.
Nitrided Hardness Options
Precision gas nitriding achieves HV 900+ case hardness, resisting wear and galling in abrasive resins and high-temperature molding environments.
3–7 Day Sample Turnaround
Rapid prototyping and validation with full dimensional reports, so you can test fit and function before committing to mass production runs.
Full FAI Documentation
Every shipment includes first-article inspection reports, material certificates and CMM measurement data, meeting OEM traceability and audit requirements.
ISO 9001:2015 Certified
Five-step QC flow from spectral analysis through final inspection ensures zero tolerance failures and repeatable quality across every production batch.
Straight Ejector Pin Configurations & Use Cases
Match your mold design to the right pin specification — from standard through-hardened straight ejector pins for high-cavity consumer molds to armor-coated and stepped variants for demanding 5G, automotive and medical applications.
High-Cavity Consumer Electronics Molds
A tier-one mobile-phone case manufacturer needed 96-cavity straight ejector pins that could maintain +/-0.005 mm positioning over 500,000 cycles without deflection or surface scoring, while meeting 48-hour sample delivery.
XUXIANG supplied H13 through-hardened straight ejector pins ground to +/-0.002 mm, ZEISS-verified to 0.7um repeatability. Pins delivered in 5 days; mold achieved 600,000+ cycles with zero pin replacement and consistent part ejection.
Micro-Connector Tooling for 5G
A 5G board-to-board connector tooling program required ultra-fine straight ejector pins (Ø0.8–1.2 mm) with nitrided surface hardness ≥HV 1000 to eject thin-wall micro-terminals without burr transfer or pin galling over extended production runs.
Nitrided straight ejector pins machined on Sodick slow-wire EDM, Ra 0.2um finish, delivered with full FAI and hardness certificates. Tooling ran 300,000+ shots with no measurable wear; ejection force remained stable within 5%.
Automotive Sensor Housing Molds
An ADAS sensor housing mold required armor-coated straight ejector pins resistant to glass-fiber-filled PA66 abrasion, capable of holding +/-0.003 mm perpendicularity across 12 ejection points in a high-temperature (150°C) molding environment.
TiN armor-coated straight ejector pins, Fanuc CNC-machined and ZEISS-inspected, supplied with DFM guidance on ejection angle and draft. Pins maintained perpendicularity through 200,000 cycles; no coating delamination or dimensional drift observed.
Stepped Pins for Medical Device
A medical syringe component mold demanded stepped straight ejector pins with two diameters (Ø2.0 / Ø1.5 mm) and a shoulder transition radius ≤R0.02 mm, validated to ISO 13485 traceability and supplied with material certificates for biocompatible steel.
Custom stepped straight ejector pins fabricated via multi-axis CNC and mirror EDM, corner radius measured at R0.015 mm. Full material traceability, FAI documentation and ZEISS CMM reports delivered; mold passed FDA audit with zero non-conformance.
Industrial Automation Jig Tooling
A robotics end-effector manufacturer needed heavy-duty straight ejector pins for injection-molded gripper inserts, requiring corrosion resistance, high load capacity and dimensional stability across mixed-resin production (PC, POM, PA) without cross-contamination or pin seizure.
Stainless-steel (SUS420J2) straight ejector pins, precision-ground and passivated, supplied with DFM recommendations for ejector-plate clearance. Pins operated flawlessly across 150,000 multi-material cycles; zero corrosion, zero maintenance downtime recorded.
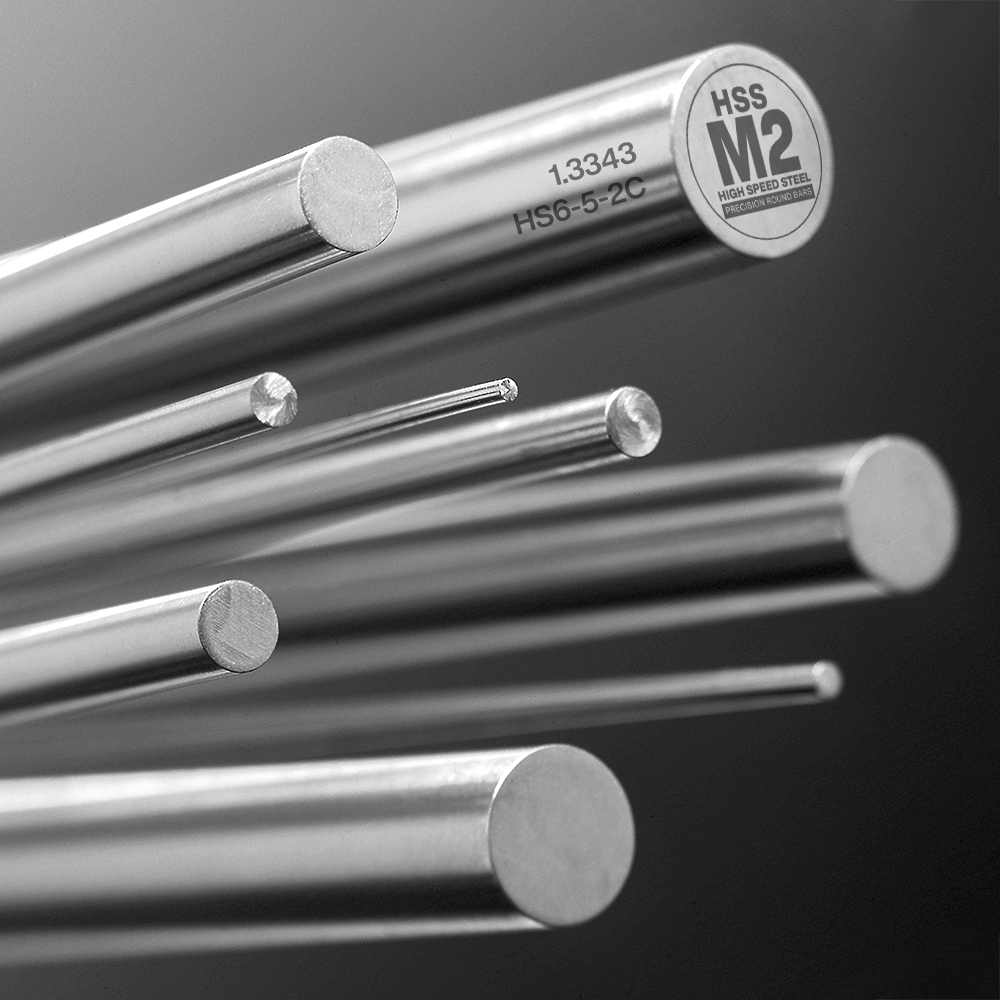
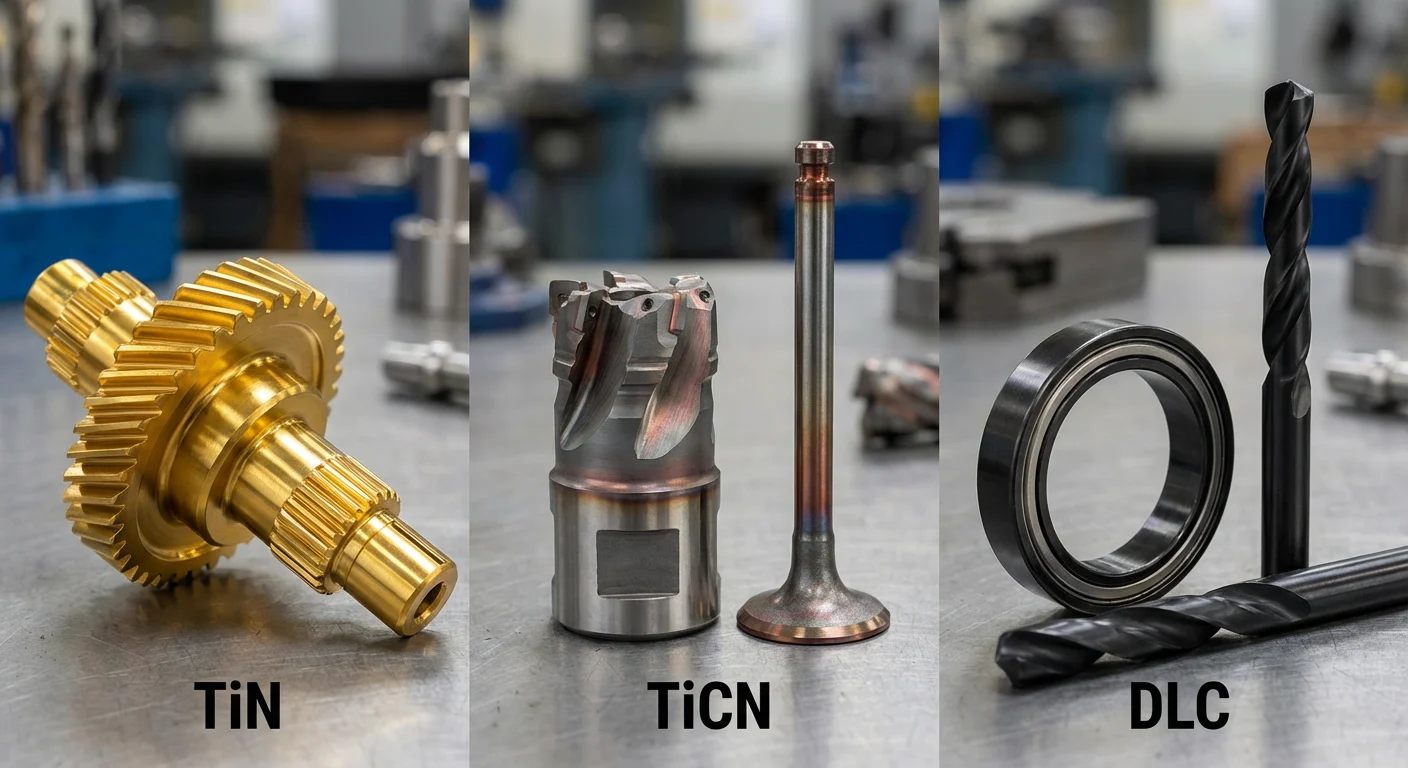
Materials & Finishes for Straight Ejector Pins
Advanced Processes for Straight Ejector Pins
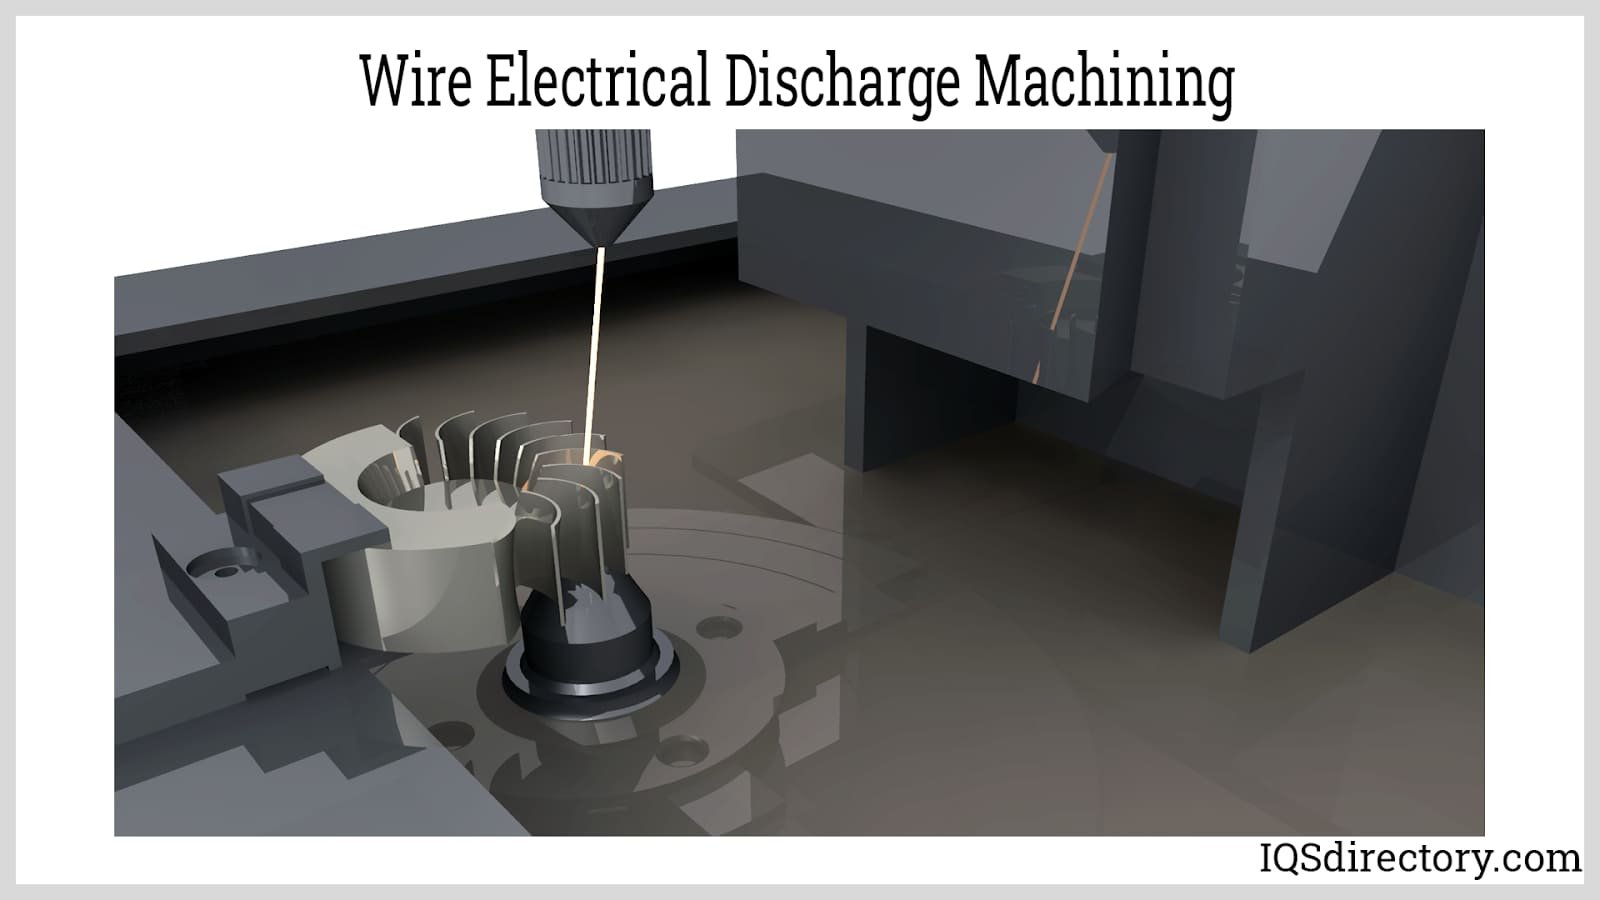
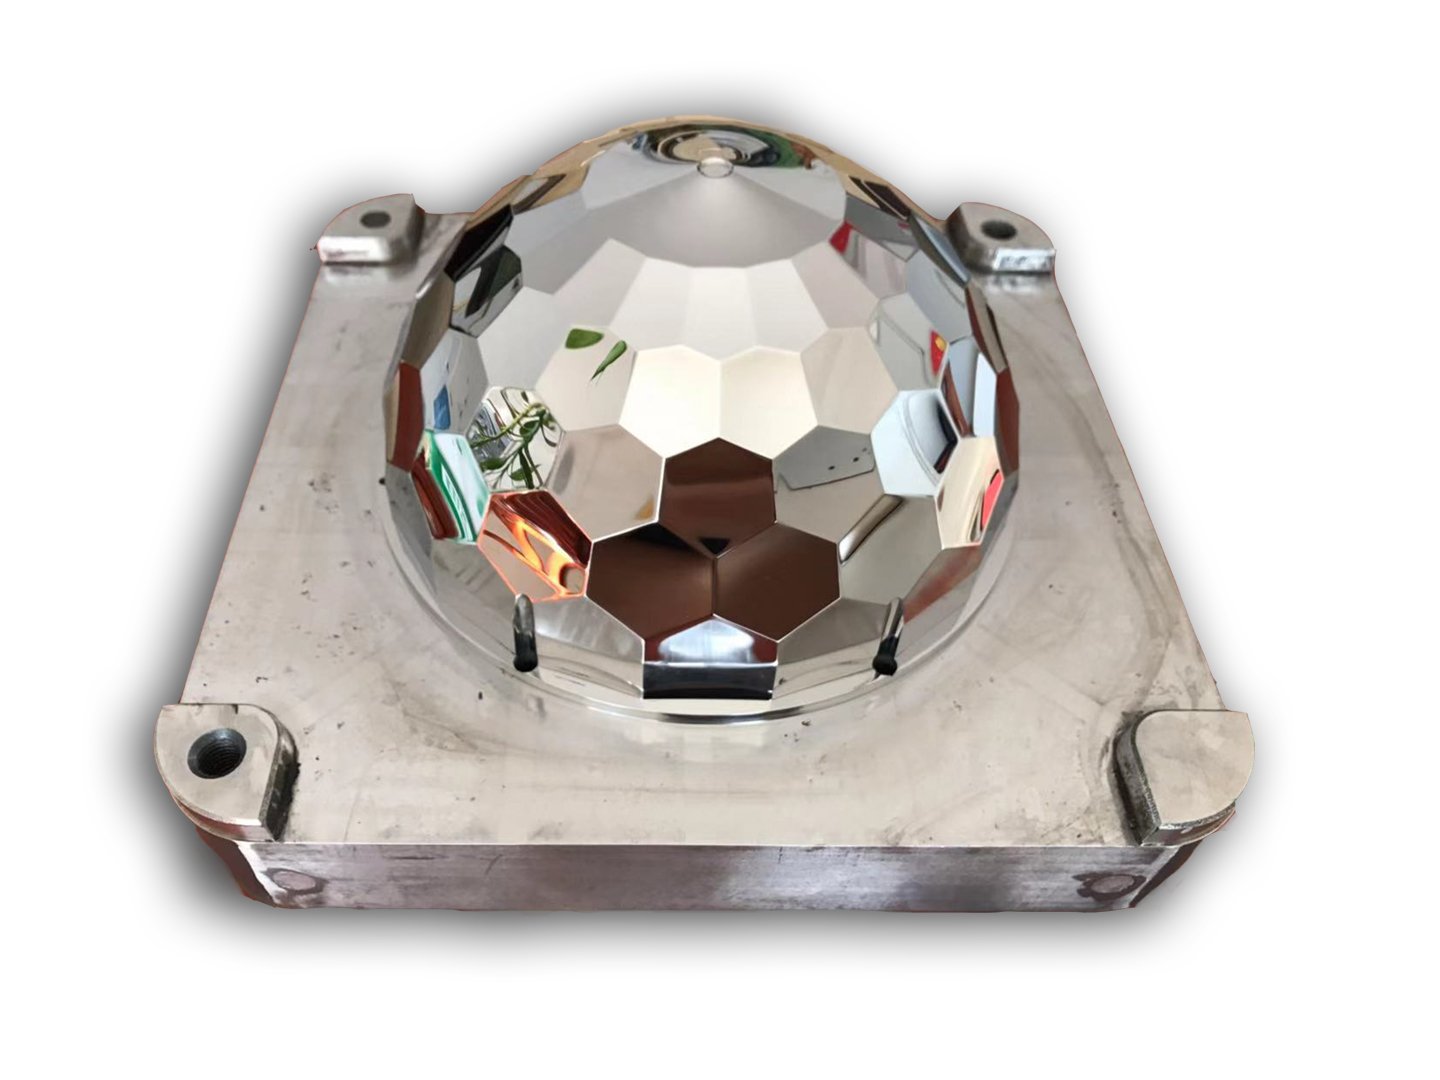
Mirror EDM
Mitsubishi mirror-grade EDM delivers Ra 0.1 µm surface finishes on pin shafts, eliminating micro-scratches and drag marks that cause part sticking, extending tool life and reducing maintenance cycles in high-volume production.
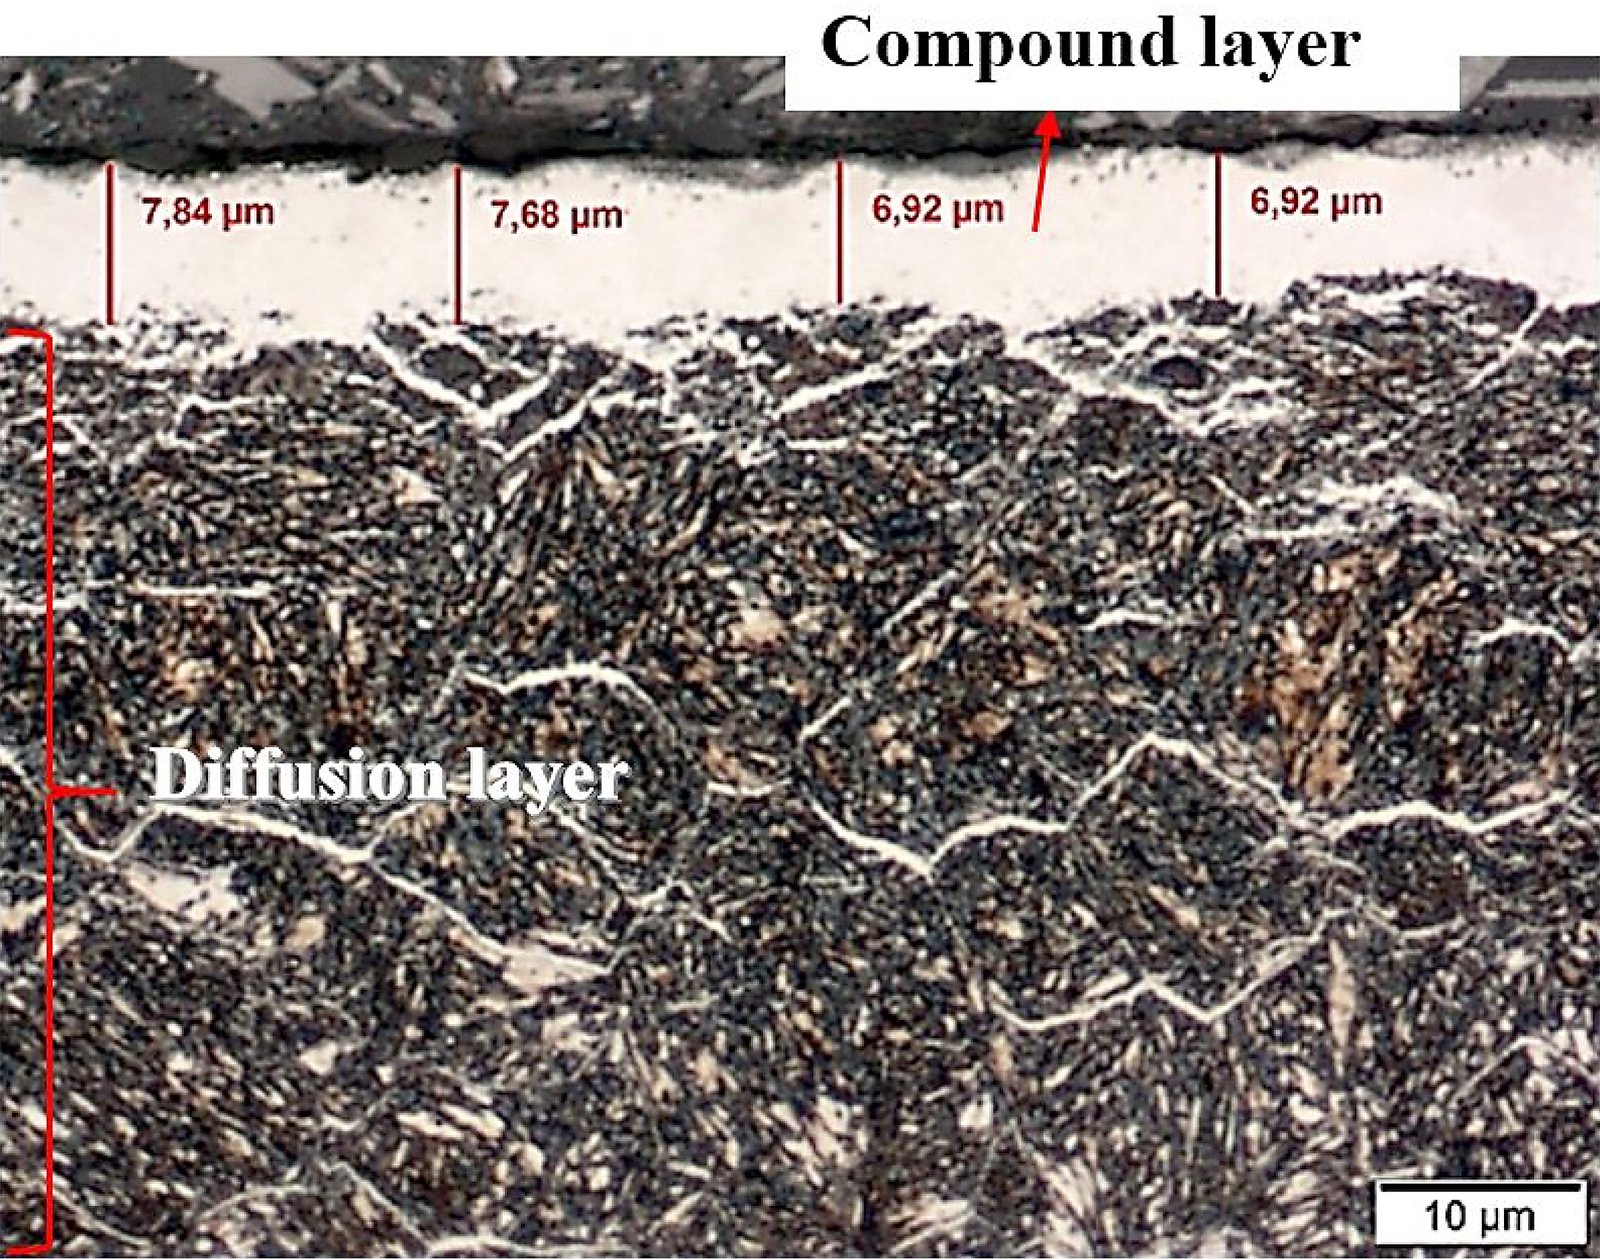
Nitriding Treatment
Gas nitriding hardens pin surfaces to HRC 58–62 while maintaining core toughness, preventing galling and wear under repeated ejection cycles in abrasive engineering resins and high-temperature automotive applications.
Ejector Pin Hardware & Accessories


Spring Kits
High-fatigue spring sets for ejector return systems, rated for 1 million+ cycles. Supplied in matched compression rates and pre-tested for load consistency, ensuring reliable part ejection in high-speed injection molding and automated production lines.
Mounting Hardware
Precision shoulder screws, dowel pins and locking collars manufactured to DIN/ISO standards. Each component is surface-treated for wear resistance and supplied with traceability documentation, ensuring secure assembly and long-term dimensional stability in demanding mold environments.
Wear Plates
Hardened wear plates and backing plates precision-ground to +/-0.005 mm flatness, protecting ejector systems in high-tonnage and abrasive-filled molding. Available in tool steel, carbide-faced and nitrided finishes with full material spectral analysis and hardness certification.
About XUXIANG — Precision Straight Ejector Pins Since 2010
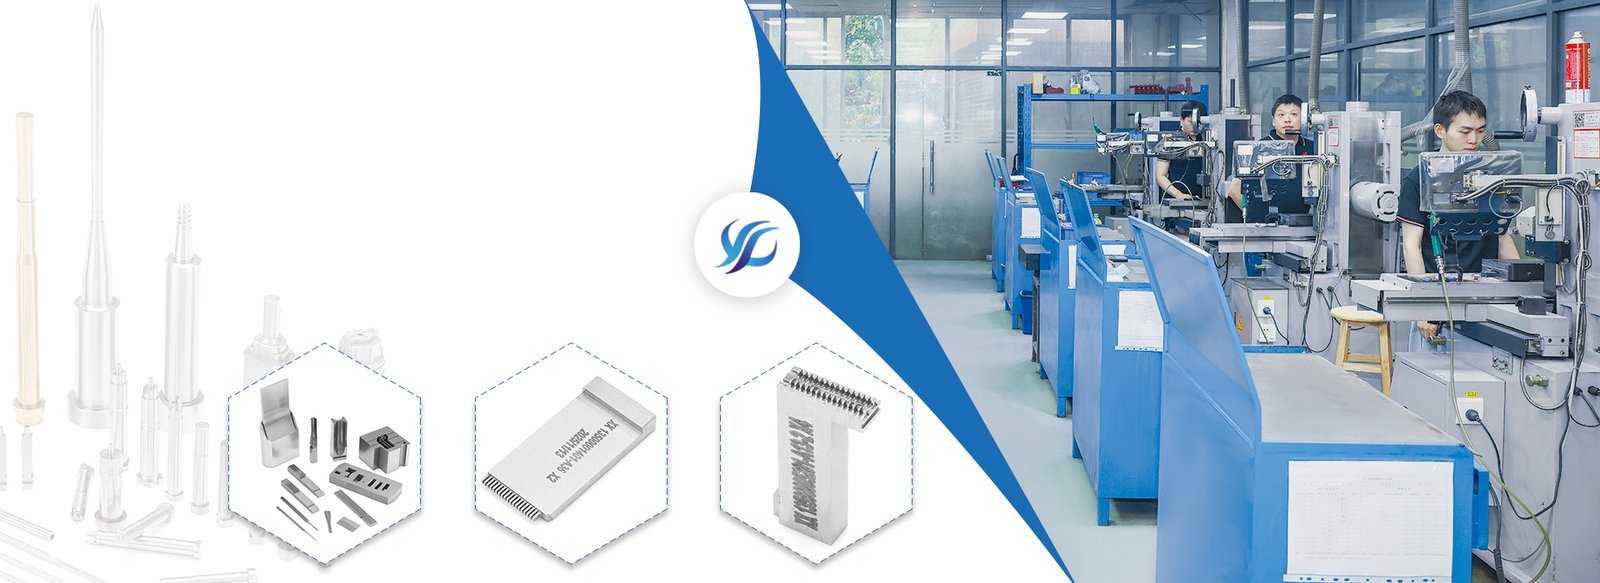
Founded in 2010 in Dongguan’s Chang’an manufacturing hub, XUXIANG has grown from a specialist mold-core machining shop into a dual-factory precision manufacturing group. Today we supply straight ejector pins, micro-connector tooling and high-precision mold components to electronics, 5G/telecom, automotive & NEV, industrial-automation and medical-device customers worldwide, all held to +/-0.001 mm machining accuracy and backed by ISO 9001:2015 quality systems.
Our 2,000 m² Dongguan R&D and micro-machining facility, combined with our 2025-expanded 1,400 m² Quanzhou volume-production plant, houses over CNY 8 million in Japanese, Swiss and German equipment: Sodick and Seibu slow-wire EDM, Mitsubishi mirror EDM, Fanuc CNC and a ZEISS MICURA CMM measuring to 0.7 µm. This dual-site infrastructure delivers +200 percent capacity growth and lead times roughly 30 percent faster than the industry average.
Every straight ejector pin project receives DFM engineering support from 10+ experts, five-step QC validation including ZEISS/Nikon CMM verification, and full FAI documentation with material certificates. We return quotes within 24 hours, ship samples in 3–7 days and complete mass production in 15–25 days — bridging the gap between complex CAD designs and micron-stable physical parts with dependable quality, responsive service and transparent pricing.
How XUXIANG Eliminates Tolerance Failure on Straight Ejector Pins
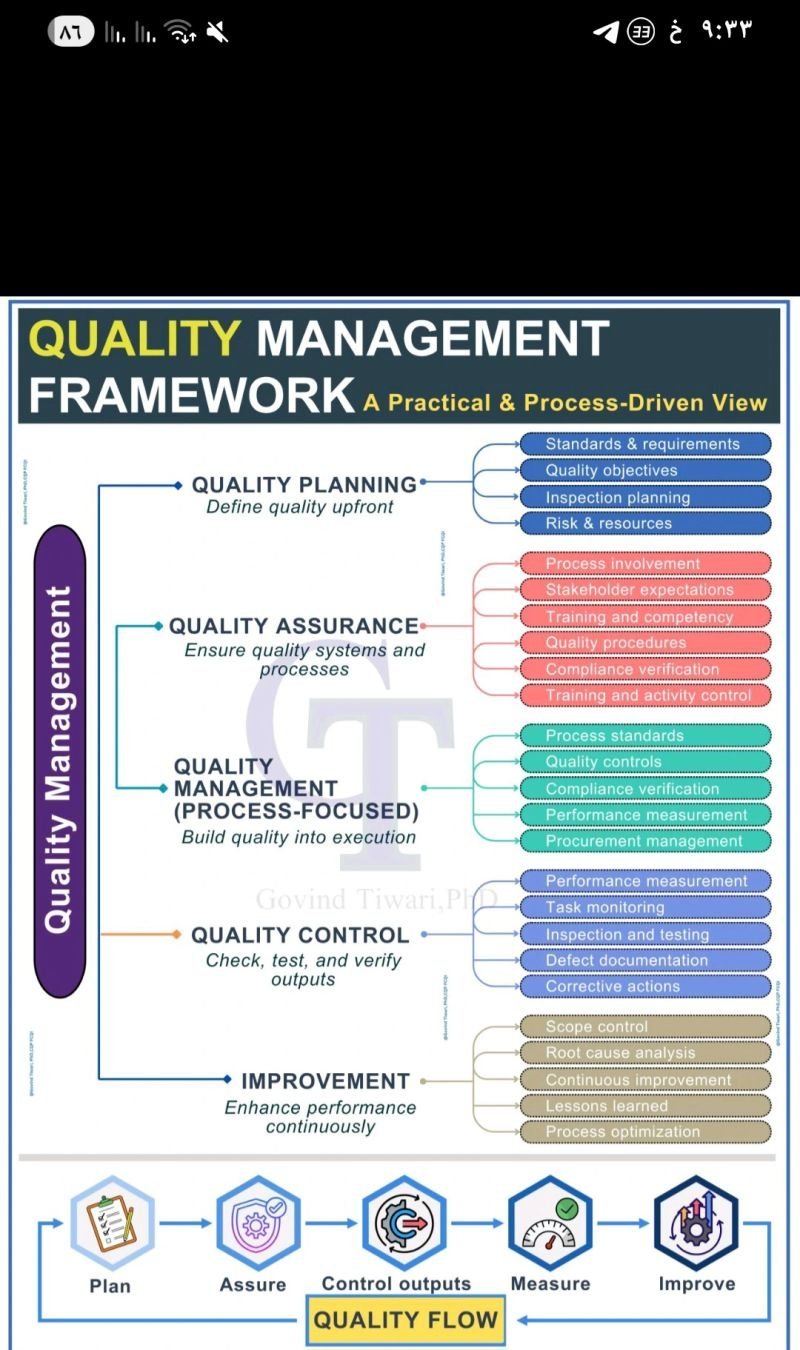
Five-Step Quality Control Flow
Every straight ejector pin batch moves through a five-stage validation protocol — material spectral analysis, in-process tolerance monitoring, ZEISS/Nikon CMM verification, surface-integrity checks and final FAI documentation — ensuring dimensional stability and surface finish meet +/-0.001 mm and Ra 0.1um specifications before shipment.
- Material spectral analysis confirms alloy composition and heat-treat integrity before machining begins
- In-process monitoring captures deviation in real time, preventing cumulative error across high-volume runs
- ZEISS MICURA CMM (0.7um resolution) and Nikon toolmaker's microscopes validate diameter, straightness and concentricity
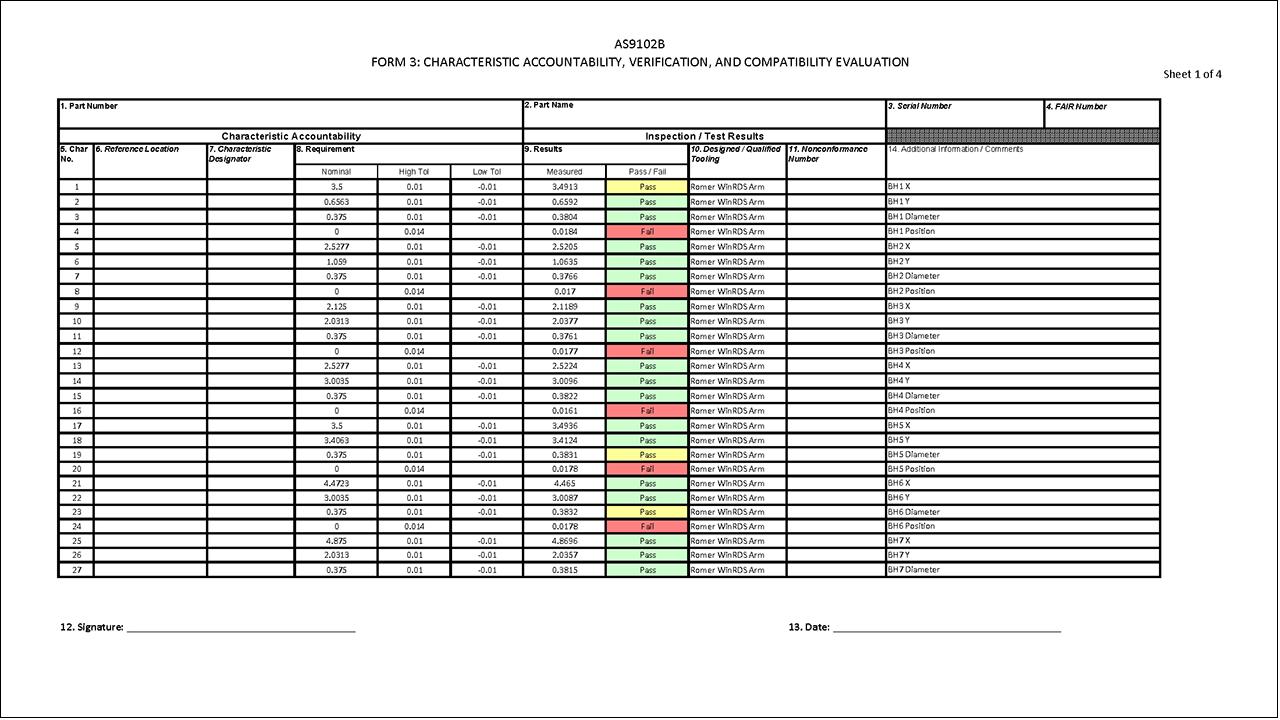
- Full FAI reports with material certificates accompany every order, providing traceability and audit-ready documentation
DFM Engineering Support from 10+ Experts
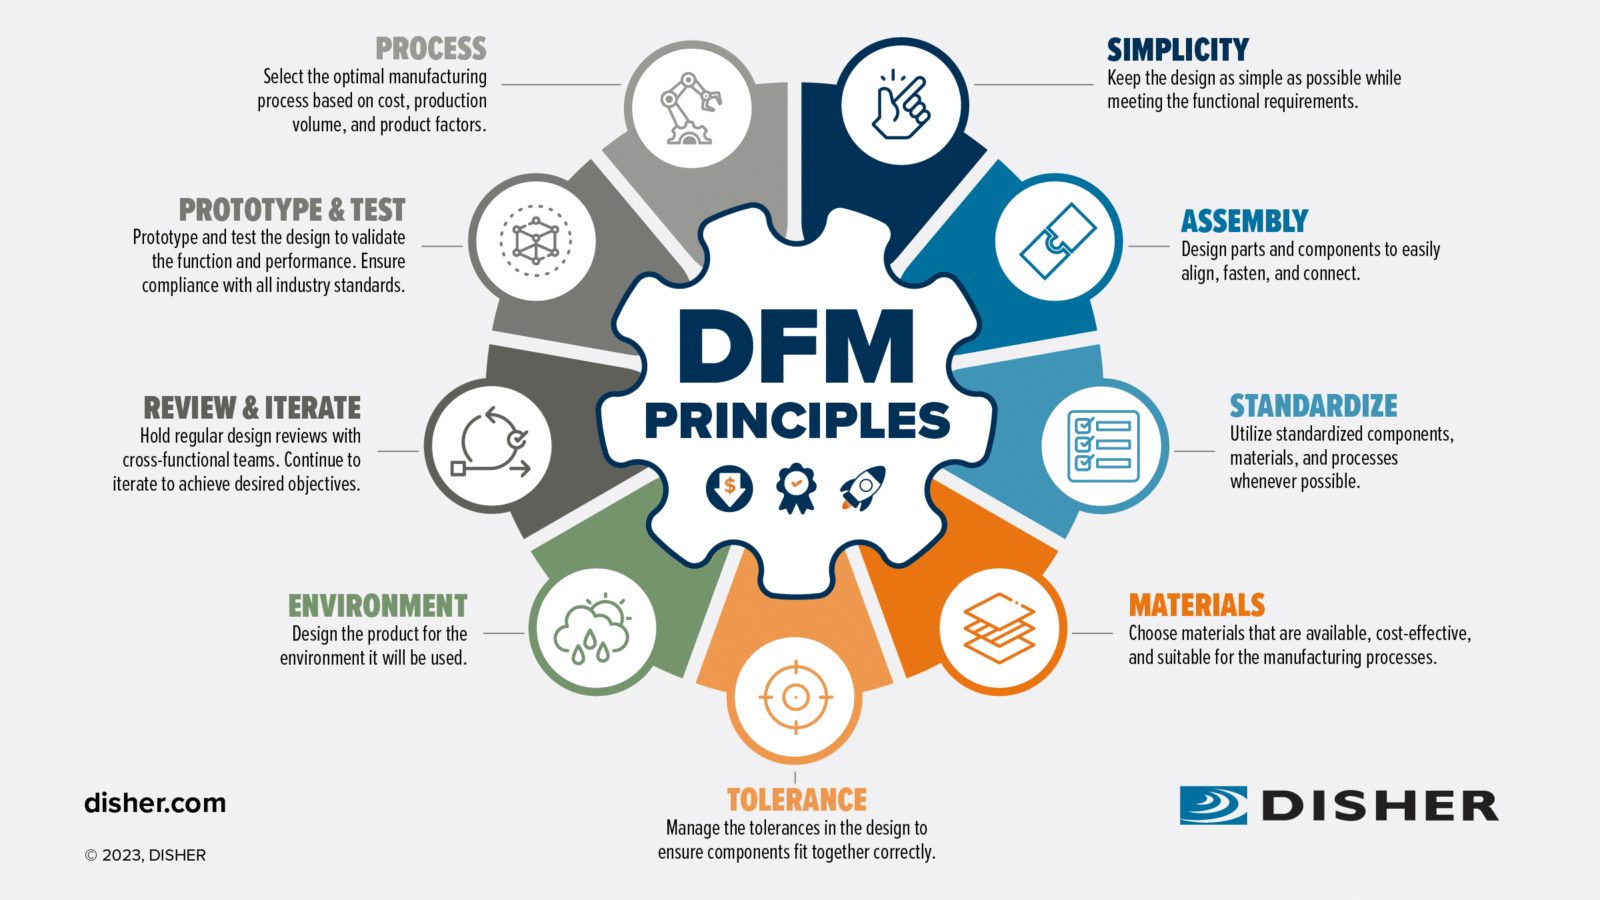
Before production begins, XUXIANG’s team of 10+ mold and machining engineers reviews your straight ejector pin drawings for manufacturability, tolerance stack-up, ejection force optimization and lifecycle durability — reducing rework risk and accelerating time-to-production by an average of 30 percent.
- Pin-diameter and length-to-diameter ratio analysis to prevent buckling and bending under ejection load
- Surface-finish and coating recommendations tailored to part material, cycle time and release requirements
- Tolerance feasibility review flags over-specified dimensions that drive cost without performance benefit
- Alternative material or heat-treat suggestions when standard specs conflict with application environment
Metrology Lab with 0.7um CMM Resolution
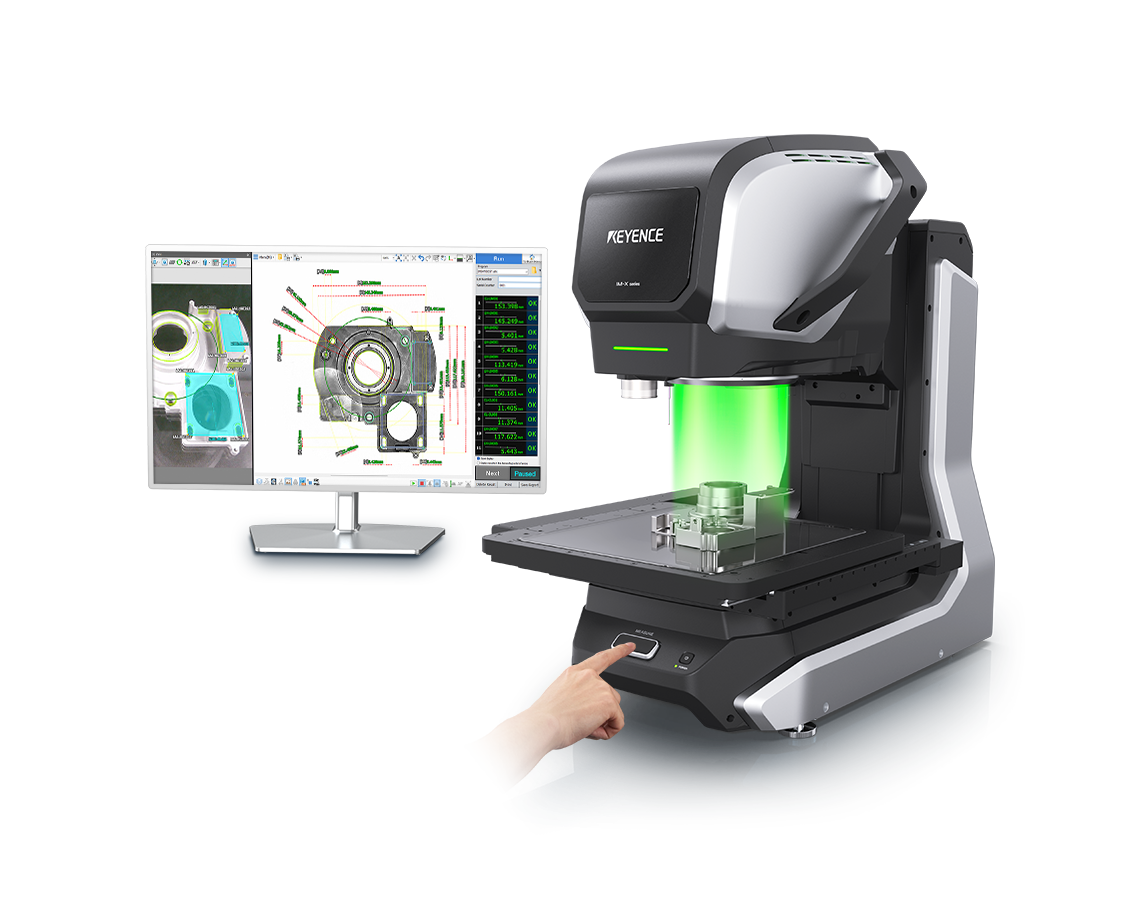
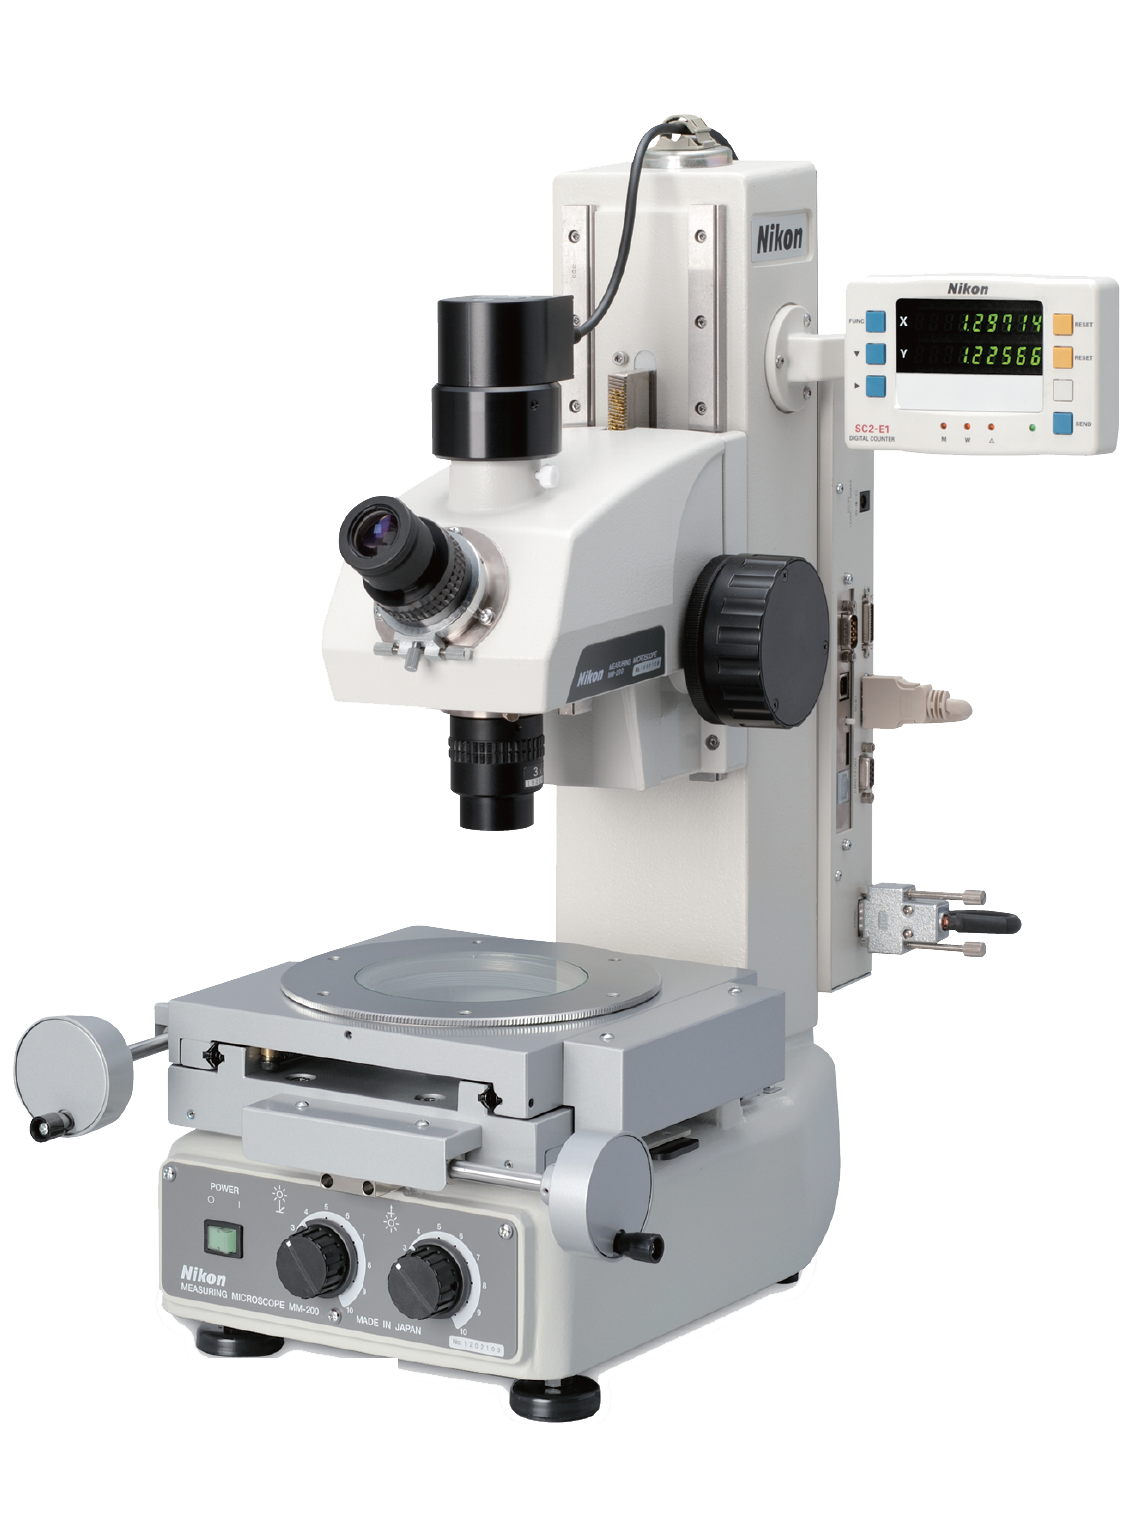
XUXIANG’s metrology lab is anchored by a ZEISS MICURA coordinate measuring machine with 0.7um repeatability, complemented by Nikon V-12B and MM-400 class toolmaker’s microscopes — delivering measurement certainty that matches the micron-stable precision of our straight ejector pins and eliminating false-reject or false-accept decisions.
- ZEISS MICURA CMM captures diameter, straightness, perpendicularity and concentricity across full pin length
- Nikon microscopes verify edge break, surface defects and micro-geometry at magnifications up to 400×
- Temperature-controlled environment (20°C ± 1°C) ensures thermal stability during long-duration inspection runs
- Calibration traceable to national standards, with annual third-party audit and certification renewal
ISO 9001:2015 Process Governance
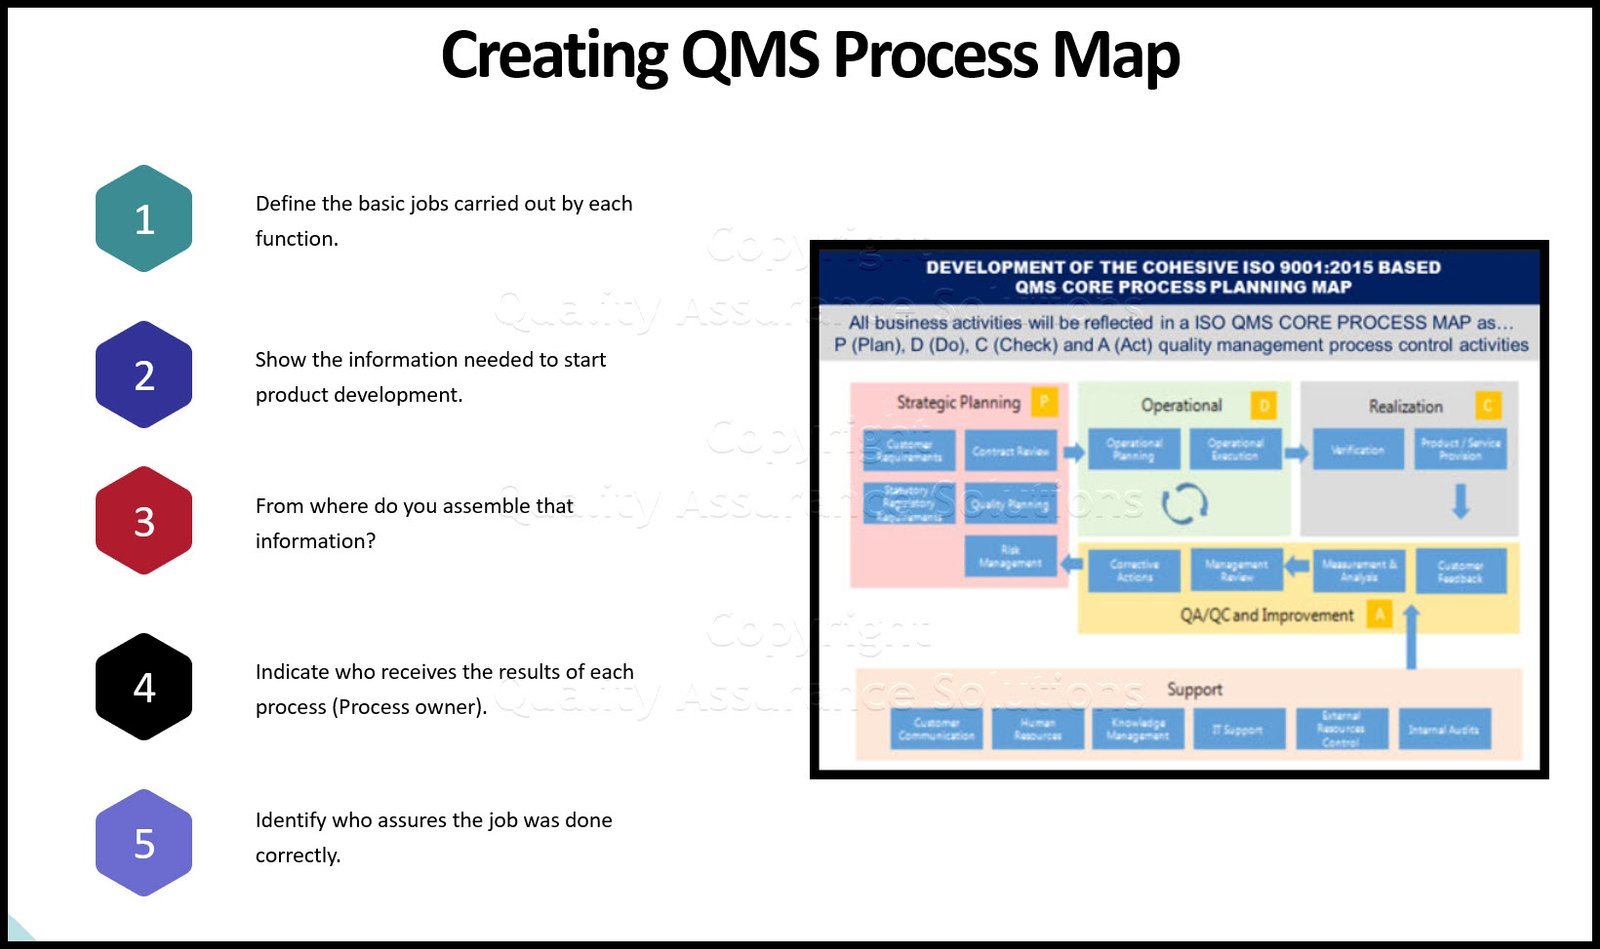
XUXIANG’s straight ejector pin manufacturing operates under ISO 9001:2015 quality management, with documented work instructions, operator qualification records, equipment maintenance logs and corrective-action tracking — ensuring repeatable outcomes across batches, shifts and production sites in Dongguan and Quanzhou.
- Standard operating procedures for every machining, grinding, EDM and inspection step
- Operator certification program with annual skill assessment and equipment-specific training
- Preventive maintenance schedule for all CNC, EDM and CMM assets, minimizing unplanned downtime
- Non-conformance tracking and root-cause analysis close the loop on any deviation, preventing recurrence
Why Choose XUXIANG Straight Ejector Pins Over Standard Suppliers
Evidence-driven comparison: precision-grade tooling backed by Japanese EDM, ZEISS metrology and ISO 9001:2015 quality systems versus commodity ejector pins.
← 左右滑动查看 →
Straight Ejector Pin Production & Delivery Timeline
From design review to FAI documentation, every straight ejector pin order follows our ISO 9001:2015 six-phase workflow — engineered to deliver samples in 3–7 days and mass production in 15–25 days, roughly 30% faster than industry average.
Design Review & DFM
Our 10+ engineering experts analyze your CAD files, validate tolerances, ejection angles and surface-finish requirements, then provide actionable DFM feedback within 24 hours of quote acceptance.
Material Procurement & Verification
Certified H13, SKD61, SKH51 or stainless steel billets undergo spectral analysis to confirm composition and hardness before entering the machining queue, ensuring traceability from raw stock.
CNC & EDM Machining
Fanuc CNC centers rough-turn pin blanks to +/-0.005 mm, then Sodick slow-wire EDM machines intricate profiles and relief features to +/-0.002 mm, holding corner radii down to R 0.015 mm.
Precision Grinding & Finishing
Dawn precision grinding centers achieve final diameter tolerances of +/-0.001 mm and cylindricity within 0.002 mm, followed by mirror EDM finishing to Ra 0.1 µm where specified.
CMM Verification & QC
ZEISS MICURA CMM measures every critical dimension to 0.7 µm resolution; Nikon toolmaker’s microscopes verify surface integrity, ejector-tip geometry and coating adhesion across a five-step QC protocol.
FAI Documentation & Shipping
Full first-article inspection reports, material certificates and dimensional data accompany every shipment, with anti-corrosion packaging and express logistics for samples in 3–7 days, mass orders in 15–25 days total.
How to Order Straight Ejector Pins from XUXIANG
From CAD upload to delivery, our streamlined five-step process delivers +/-0.001 mm precision straight ejector pins with full FAI documentation—backed by 24-hour quotes and ISO 9001:2015 quality assurance.
Submit Your CAD & Requirements
Upload 2D/3D CAD files or technical drawings with material, tolerance and finish specifications. Our engineering team provides DFM feedback within 24 hours to optimize manufacturability and cost.
Receive Your 24-Hour Quote
Get a detailed quotation covering material, machining process, lead time and pricing—transparent, itemized and ready for procurement approval. No hidden fees or surprise revisions.
Approve Sample Production
We manufacture first-article samples in 3–7 days, validated on ZEISS MICURA CMM to 0.7um accuracy. Full dimensional reports and material certificates accompany every sample shipment.
Launch Mass Production
Upon sample approval, bulk orders enter our Sodick slow-wire EDM and Fanuc CNC lines. In-process monitoring and five-step QC ensure every pin meets your exact tolerances.
Receive & Inspect Your Order
Finished straight ejector pins ship in 15–25 days with FAI documentation, material certificates and traceability records—ready for immediate integration into your mold assembly or production line.
ISO 9001:2015 & Industry Certifications for Straight Ejector Pins

What Our Customers Say About XUXIANG Straight Ejector Pins
We switched to XUXIANG straight ejector pins for our 5G connector molds and saw zero tolerance failures across 2.3 million cycles. The +/-0.001 mm precision and mirror finish eliminated our ejection marks completely.
XUXIANG delivered custom-ground straight ejector pins for our automotive sensor housings five days ahead of schedule. Mold downtime dropped by 42% compared to our previous supplier, and the FAI documentation was flawless.
The ZEISS CMM reports gave us total confidence in dimensional stability. After 18 months of high-volume production with XUXIANG straight ejector pins, we’ve had zero pin failures and consistent part quality across 12 cavity medical molds.
FAQ: Straight Ejector Pins, Specifications & Ordering
What is the minimum order quantity for straight ejector pins?
What tolerances can you guarantee on straight ejector pins?
How long does it take to receive straight ejector pins after I place an order?
Can I request samples before committing to a production order?
What materials and surface finishes are available for straight ejector pins?
Do you provide DFM feedback or engineering support for custom straight ejector pins?
How do you protect my design IP when I share CAD files for straight ejector pins?
What payment terms and shipping options do you offer?
Are your straight ejector pins compatible with standard mold-base systems?
The Complete Buyer’s Guide to Straight Ejector Pins for Precision Mold Tooling
Navigate material grades, tolerance specifications, and supplier quality systems with confidence. This guide delivers a decision framework, critical selection criteria, and the most common procurement mistakes to avoid when sourcing straight ejector pins for high-precision injection molds.
1. What Are Straight Ejector Pins and Why Precision Matters
Straight ejector pins are precision-ground cylindrical tooling components that push finished plastic parts out of injection-mold cavities after each molding cycle. They travel through guide holes in the mold base, strike the part at ejection, then retract to allow the next shot. A single multi-cavity mold may use 20 to 200 pins, each cycling tens of millions of times over the tool’s life.
Tolerances of +/-0.001 mm — the maximum machining accuracy XUXIANG holds on pin diameter and straightness — are not marketing claims but engineering necessities. A pin oversized by 0.003 mm will bind in its guide bore, causing ejection marks, cycle delays or catastrophic tool damage. A pin undersized by the same margin allows molten resin to flash into the clearance gap, creating burrs that fail cosmetic inspection or dimensional QC.
Electronics manufacturers building micro-connector housings, automotive tier suppliers molding ADAS sensor brackets, and medical-device OEMs producing implantable-grade enclosures all specify straight ejector pins to micron-level tolerances because part rejection costs far exceed the premium for precision tooling.
2. Evolution of Straight Ejector Pin Manufacturing Standards
Manual grinding dominated straight ejector pin production through the 1980s, delivering +/-0.01 mm tolerances adequate for consumer-goods molding but insufficient for precision electronics. ISO 8405 standardization in the early 1990s formalized dimensional and surface-finish requirements, enabling global interchangeability and driving the shift from carbon steels to high-speed steel (HSS) and carbide grades that could hold tighter tolerances under repeated cycling.
CNC precision turning and slow-wire EDM finishing emerged in the 2000s, compressing diameter tolerances to +/-0.002 mm and enabling mirror-grade surface finishes below Ra 0.2 µm. XUXIANG’s Sodick and Seibu slow-wire EDM assets routinely achieve +/-0.002 mm positional accuracy, essential for high-cavity micro-connector tooling.
The 5G and micro-molding wave after 2015 pushed tolerances into the sub-micron domain. Miniaturized board-to-board and FPC connectors demand straight ejector pins holding +/-0.001 mm over lengths exceeding 100 mm, verified by CMM systems like XUXIANG’s ZEISS MICURA (0.7 µm resolution). Today’s procurement standard is no longer ‘tight enough’ but ‘micron-stable across production lots.’
3. Types of Straight Ejector Pins by Geometry and Application
Straight ejector pins are available in four primary geometries, each optimized for specific mold architectures and part-ejection requirements. Selecting the correct variant depends on diameter constraints, hardness profile, and the mechanical stresses your tooling will encounter.
Standard Cylindrical Straight Ejector Pins
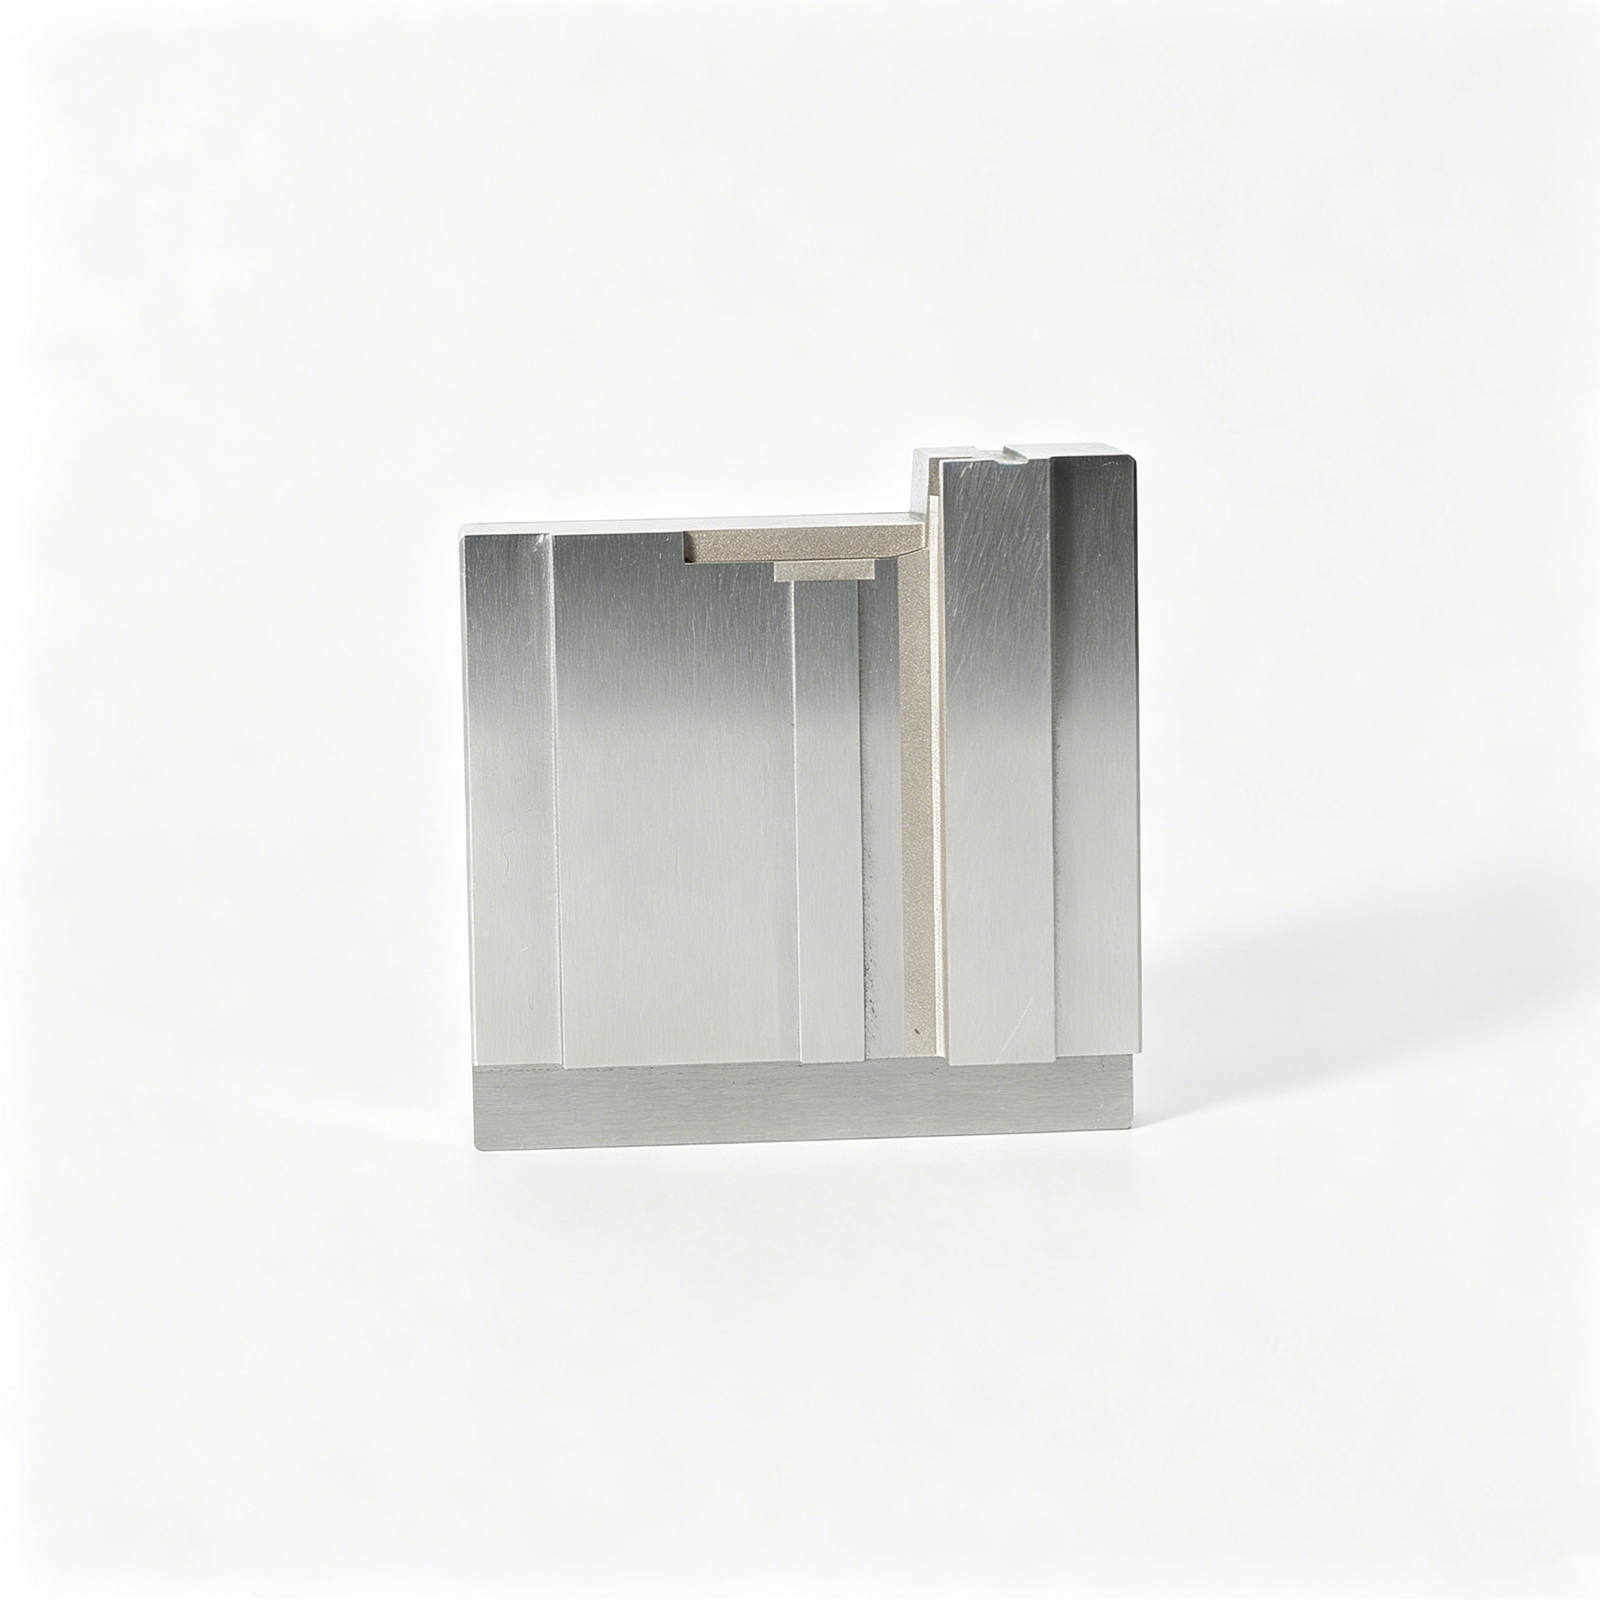
Diameter ranges from 1.0 mm to 16.0 mm cover the majority of injection-mold ejection needs. These pins suit consumer-electronics housings, automotive interior trim and general-purpose molding where uniform cross-section and straightforward installation are priorities. Specify cylindrical pins when your mold base follows HASCO, DME or FUTABA standards and ejection forces remain moderate.
Through-Hardened vs. Case-Hardened Pins

Through-hardened pins (HRC 58–62 full depth) resist bending in high-cycle automotive lamp molds and thick-wall medical housings. Case-hardened variants (HRC 58–62 surface, softer core) absorb shock in high-speed consumer tooling. Choose through-hardened for abrasive glass-filled resins; case-hardened for impact-prone ejection.
Sleeve Ejector Pins
A hollow outer sleeve protects a central core pin, ideal for ejecting fragile bosses or thin ribs in medical micro-molding. Outer diameters typically range 3.0–8.0 mm. Specify sleeve pins when part geometry includes delicate internal features that cannot tolerate single-point ejection forces.
Micro-Diameter Pins for Connector Tooling
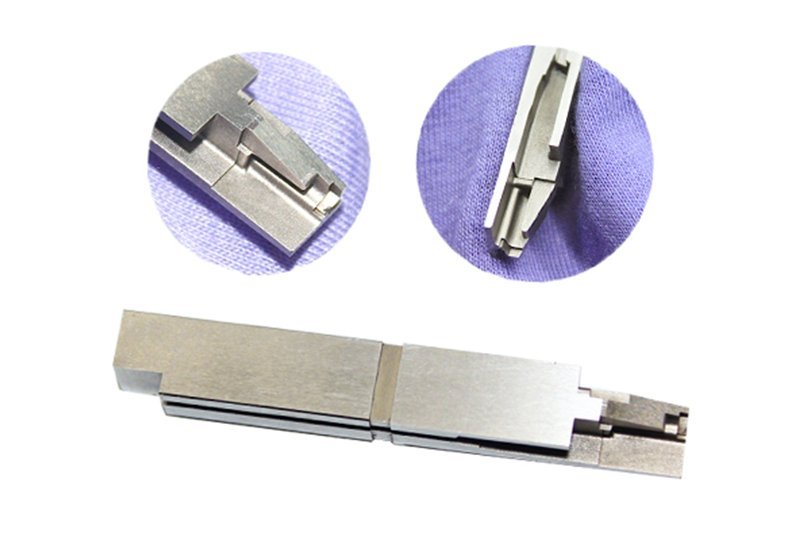
Pins below 1.0 mm diameter—often 0.3–0.8 mm—eject micro-terminals in 5G board-to-board and FPC connector molds. XUXIANG machines these on Sodick slow-wire EDM to +/-0.002 mm, validated under Nikon toolmaker’s microscopes. Specify micro pins when cavity pitch falls below 0.6 mm or terminal wall thickness is ≤ 0.15 mm.
4. Material Selection for Straight Ejector Pins: Steel Grades and Coatings
Material choice governs ejector pin life, surface wear and thermal stability across production cycles. SKH51, SKD61, carbide and stainless grades each deliver distinct hardness, cycle endurance and cost profiles that align with specific resin families and mold temperatures.
| Material | Hardness (HRC) | Typical Life Cycles | Relative Cost | Best-Fit Application |
|---|---|---|---|---|
| SKH51 (High-Speed Steel) | 60–64 | 500,000–1,000,000 | 1.0× | General-purpose, unfilled resins, moderate wear |
| SKD61 (Hot-Work Tool Steel) | 48–52 | 300,000–800,000 | 0.9× | High-temperature resins (PA, PBT), thermal cycling |
| Carbide | ≥80 | 2,000,000+ | 3.0–4.0× | Glass-filled, abrasive resins, ultra-high-volume |
| Stainless (e.g., 440C) | 54–58 | 400,000–700,000 | 1.2× | Medical, corrosion-prone environments |
When to Upgrade to Carbide
Glass-filled nylon, mineral-reinforced PBT and ceramic-loaded compounds erode standard steel within 300,000 cycles. Carbide straight ejector pins triple service life but add 200–300% to unit cost. XUXIANG recommends carbide for annual volumes above 1.5 million shots or when downtime exceeds tooling amortization.
TiN and DLC Coatings for Abrasive Resins
Titanium nitride (TiN) coatings raise surface hardness to HV 2,200 and reduce friction by 30–40%, extending SKH51 life in glass-filled PC/ABS. Diamond-like carbon (DLC) cuts adhesion on sticky LSR and TPE. Coating adds 1–2 days to lead time and 15–25% to pin cost but defers replacement by 50–80%.
5. Customization Options: Tolerances, Surface Finish, and Special Features
Procurement teams can tailor straight ejector pins across five critical dimensions — dimensional tolerance, surface finish, geometry, head configuration and traceability marking. Each lever affects cost, lead time and mold performance; understanding the trade-offs lets buyers match specification to application risk.
| Feature | Standard Spec | Premium Spec | Lead-Time Impact |
|---|---|---|---|
| Tolerance | ±0.005 mm | ±0.001 mm | +1–2 days |
| Surface Finish | Ra 0.2 µm | Ra 0.05–0.1 µm | +1 day |
| Head Style | Flat | Spherical / Chamfered | +0–1 day |
| Laser Marking | None | Part number + date code | +0.5 day |
Dimensional Tolerance Classes
Standard straight ejector pins ship at ±0.005 mm, sufficient for general-purpose tooling. Premium tooling — micro-connector molds, high-density multi-cavity arrays — demands ±0.001 mm or tighter to prevent flash and ensure consistent ejection force across thousands of cycles.
XUXIANG’s slow-wire EDM and ZEISS MICURA CMM (0.7 µm resolution) enable ±0.001 mm class work. Specifying tighter tolerance adds 1–2 days for metrological validation but eliminates field rework.
Surface Finish and Coating
Surface roughness directly impacts part release and pin life. Ra 0.2 µm suits non-cosmetic cavities; Ra 0.1 µm or mirror-grade EDM finishes are essential for optical lenses, medical housings and transparent connectors. TiN or DLC coatings add wear resistance for abrasive resins but require post-grind lapping to maintain diameter tolerance.
Custom Lengths and Head Styles
Standard catalogs list pins in 10 mm increments; custom lengths match exact stack heights and reduce machining waste. Head styles — flat, spherical or chamfered — affect ejector-plate contact and stroke stability. Spherical heads self-align in off-axis loading; chamfered heads ease assembly and reduce edge chipping during high-speed cycling.
6. Critical Quality Elements in Straight Ejector Pin Manufacturing
Straight ejector pins demand four non-negotiable inspection checkpoints: cylindricity, straightness, hardness and surface integrity. Buyers must verify that suppliers measure these attributes on calibrated equipment — not estimate them — and provide batch-traceable documentation with every shipment.
Cylindricity and Straightness Verification
CMM verification is the only reliable method for cylindricity and straightness. XUXIANG uses a ZEISS MICURA CMM with 0.7 µm resolution to map full-length geometry on every critical batch, ensuring deviation stays within +/-0.001 mm.
Toolmaker’s microscopes (Nikon V-12B class) cross-check diameters at multiple sections. Demand a CMM report showing measured vs. nominal for each dimension, not a pass/fail checkbox.
Hardness and Surface-Roughness Testing
Rockwell and Vickers hardness tests confirm heat-treat integrity; spec ranges typically fall between HRC 50–62 for SKH51 and similar tool steels. Surface roughness below Ra 0.2 µm prevents galling and extends pin life.
XUXIANG’s mirror-grade EDM achieves Ra 0.1 µm, verified by contact profilometry. Request hardness certificates and roughness data for every material lot.
ISO 9001 and Process Control Documentation
ISO 9001:2015 certification ensures traceability from raw-material spectral analysis through final inspection. IATF 16949 adds automotive-grade PPAP and control-plan rigor, critical for NEV and ADAS applications.
Demand material certificates, dimensional FAI reports, CMM data files and process capability (Cpk ≥ 1.33) studies. XUXIANG provides full documentation as standard, not on request.
7. How to Choose a Straight Ejector Pin Manufacturer: Supplier Evaluation Criteria
Selecting a straight ejector pin supplier requires due diligence across equipment, process control and service responsiveness. A systematic checklist separates precision-capable shops from commodity vendors and reduces risk of tolerance failure or delivery delay.
Equipment and In-House Capabilities
Verify CNC grinding centers (Dawn, Haas class), precision lathes and in-house heat-treatment furnaces. Shops relying on outsourced hardening add 2–3 days and introduce traceability gaps. Ask for equipment lists and photos; XUXIANG publishes Sodick EDM, Beijing Jingdiao CNC and Dawn grinding assets backed by CNY 8 million in capital investment.
Metrology and Inspection Documentation
Demand CMM inspection reports with actual measured values, not pass/fail stamps. ZEISS or Mitutoyo CMMs measuring to ≤1 µm confirm micron-class claims. Request material certificates (spectral analysis) and surface-finish data (Ra values). Vague ‘Certificate of Conformance’ documents without dimensions are red flags.
Lead Time, MOQ and Engineering Support
24-hour quotation turnaround and 3–7 day production windows signal lean operations and capacity. Confirm MOQ flexibility for prototypes (50–100 pcs) and production runs. Green flags include DFM feedback before PO, case studies in your sector and ISO 9001:2015 certification with audit dates.
8. Common Mistakes Buyers Make When Sourcing Straight Ejector Pins
Even experienced buyers fall into four sourcing traps when ordering straight ejector pins, each triggering downstream costs far exceeding any initial savings. These mistakes compound over production runs, turning a 5% purchase discount into 15–30% mold downtime and scrap expense.
Specifying Looser Tolerances to Cut Price
Relaxing pin diameter from +/-0.005 mm to +/-0.01 mm saves 10–15% on unit cost but creates clearance variance that permits melt flash at the parting line. Flash requires secondary deflashing, raises scrap rates 8–12%, and shortens mold life by 20–25% due to wear from ejection friction.
XUXIANG holds +/-0.002 mm on slow-wire EDM work; specifying the tightest tolerance your mold design allows ensures consistent ejection force and eliminates flash rework across multi-cavity tools.
Ignoring Surface Finish Specifications
Omitting Ra requirements or accepting Ra 0.4 µm when Ra 0.2 µm is feasible invites galling and polymer adhesion, especially in glass-filled resins. Rough surfaces increase ejection force 15–30%, causing part sticking, cosmetic defects and pin seizure after 50,000–100,000 cycles.
Mirror-grade EDM finishes down to Ra 0.1 µm, standard in XUXIANG’s sinker and wire processes, eliminate micro-scratches and extend pin service intervals by 40–60%.
Ordering Without Material Certificates
Skipping material traceability to save documentation fees risks hardness variance of +/-3 HRC within a single lot, leading to uneven wear and premature failure. Uncertified pins may substitute lower-cost alloys that soften under heat, causing dimensional drift and mold crashes.
XUXIANG provides spectral analysis and hardness certificates with every shipment, validated against ISO 9001:2015 material standards, ensuring HRC consistency within +/-1 and full traceability to mill heat numbers.
Choosing Suppliers Without CMM Capability
Suppliers lacking coordinate-measuring-machine verification cannot prove diameter, straightness or perpendicularity, leaving you with no recourse when pins bind or cause misalignment. Without CMM data, first-article inspection relies on hand gauges with +/-0.01 mm uncertainty — ten times looser than mold requirements.
XUXIANG’s ZEISS MICURA CMM measures to 0.7 µm and generates full FAI reports with diameter profiles, straightness deviations and surface maps, providing traceability that protects both production yield and warranty claims.
9. Pricing and Cost Structure for Straight Ejector Pins
Straight ejector pin pricing follows four primary cost drivers: material grade, dimensional tolerance, surface treatment, and order volume. Standard SKH51 or H13 steel pins in +/-0.01 mm tolerance typically start at USD 2–5 per piece for quantities of 1–10, dropping to USD 0.80–1.50 at 101–1,000+ units. Carbide pins command a 200–300% premium due to raw-material cost and grinding complexity.
Custom tolerances below +/-0.005 mm add 20–40% to unit cost, while coatings (TiN, TiCN, CrN) introduce a USD 0.30–0.80 per-pin surcharge depending on batch size and process. Setup fees for non-standard diameters, lengths beyond 300 mm, or proprietary geometries range from USD 50 to USD 200 per SKU, amortized across the order.
Lead times compress with volume: 3–5 days for stock-diameter steel pins in small batches, 7–10 days for coated or carbide variants, and 10–14 days for fully custom specifications requiring electrode fabrication and slow-wire EDM. XUXIANG’s dual-factory capacity and pre-stocked blanks deliver approximately 30% faster turnaround than traditional mold-component suppliers.
| Quantity Tier | Standard Steel (USD/pc) | Carbide (USD/pc) | Coated Steel (USD/pc) | Lead Time (days) |
|---|---|---|---|---|
| 1–10 pcs | 2.00–5.00 | 6.00–15.00 | 3.00–6.50 | 3–5 |
| 11–100 pcs | 1.20–2.50 | 4.00–9.00 | 1.80–3.50 | 5–7 |
| 101–1,000 pcs | 0.80–1.50 | 2.50–5.50 | 1.20–2.00 | 7–10 |
| 1,000+ pcs | 0.50–1.00 | 1.80–4.00 | 0.80–1.30 | 10–14 |
10. Steps to Launch Your Precision Mold Project with Straight Ejector Pins
Launching a precision mold project with straight ejector pins requires a structured six-step workflow that bridges design intent and serial production. Each phase builds quality and reduces risk before scaling to volume.
Define Cavity Layout and Pin Count
Map ejection-point locations across all cavities, noting part geometry, wall thickness and draft angles. Count total straight ejector pins required, including spares for wear rotation.
Specify Diameter, Length, Material and Tolerance
Call out pin diameter (typically 1.0–16.0 mm), working length, SKH-51 or H13 material grade, and positional tolerance (e.g., +/-0.002 mm). Include surface finish (Ra ≤ 0.2 µm for mirror-class) and any coating requirements.
Request Quotes with Dimensional Drawings
Submit 2D drawings or STEP files showing pin diameter, length, head style and tolerance zones. XUXIANG returns quotes within 24 hours, backed by DFM feedback from 10+ engineering experts.
Review Inspection Reports and Material Certificates
Verify ZEISS CMM data, spectral analysis and material certs before production. Confirm compliance with ISO 9001:2015 five-step QC flow and request FAI documentation for traceability.
Order Pilot Batch and Validate In-Mold
Run a pilot batch of 10–50 pins to validate ejection force, wear behavior and dimensional stability under production cycles. Adjust tolerances or coatings based on real-world performance data.
Scale to Production Volumes
Lock specifications and scale to full volumes with delivery ~30% faster than industry average. Leverage XUXIANG’s 2025 Quanzhou expansion for 200% annual capacity lift and dependable mass production.
Request Your Straight Ejector Pin Quote Today
Send your technical specifications now and receive a detailed quote within 24 hours — backed by +/-0.001 mm precision and ISO 9001:2015 quality assurance.